Custom Printed Vacuum Bags for Bulk Orders: Materials, Sizes, Printing & OEM Buying Guide Ordering custom printed vacuum bags in bulk is very different from buying a few sample pouches. For importers, distributors, private-label brands, food processors
and contract packers, a single specification error can be repeated across thousands of bags — or an entire container. The bag has to fit your vacuum machine, protect the product, carry the right print for the destination market, and ship in a carton and pallet
configuration that works commercially. This guide explains what bulk buyers should confirm before requesting a quotation, how to specify bag type, material, size, thickness and printing, why MOQ is only one of several numbers to compare, and how sample approval
leads to bulk production and FCL or LCL shipment. Quick Answer: What Should a Bulk Buyer Confirm Before Ordering Custom Vacuum Bags? Before requesting a quotation, buyers should confirm the product being packed, vacuum machine type, bag structure, thickness,
size, printing requirements, annual or order volume, destination market and required documentation. Product being packed: frozen, chilled or dry; bone-in or sharp edges; liquid or marinade content Vacuum machine type: nozzle-type, chamber or external (non-nozzle)
Bag type and structure: smooth or embossed (channel); material layers Thickness: in micron or mil, and what the figure refers to Bag size: width, length, headspace and sealing allowance Printing requirements: artwork, colors, print area, barcode or date-coding
area Order volume: quantity per size, per design and per year Destination market and documents: labeling and documentation requirements Do not evaluate the bag independently from the vacuum sealing system. A bag that looks right on paper can still fail on
your machine. 1. Start with the Product and the Machine, Not the Artwork Printing is the most visible part of a custom vacuum bag, but it is rarely the part that decides whether the order succeeds. Experienced buyers settle the functional specification first
and send artwork afterwards. Two questions come before everything else: What is being packed? Product form, weight, sharp edges or bones, moisture or liquid content, and whether it will be refrigerated, frozen or heat-treated all influence the bag structure
and thickness you need. Which vacuum machine will seal it? The machine's air-evacuation method determines which bag type can be used. This is the first compatibility check in any bulk order. 2. Smooth vs. Embossed Vacuum Bags: Which One Fits Your Machine?
For international buyers, this is the most important first check. Vacuum bags are commonly supplied as smooth (flat) pouches or embossed (channel) bags, and the two are not interchangeable on every machine. FeatureSmooth (flat) vacuum pouchesEmbossed (channel)
vacuum bags How air is removed The machine design removes the air — for example through a nozzle, or by placing the pouch in a vacuum chamber Embossed channels on the film create air paths, so an external machine can draw air out through the bag opening Commonly
used with Nozzle-type and chamber vacuum sealers External (non-nozzle) vacuum sealers Buyer should confirm Pouch width against sealing length or chamber size; sealing conditions for the bag structure Bag opening position and effective sealing length in the
machine manual; channel pattern suits the machine These pairings are common patterns, not guarantees. Machine designs vary, so confirm the bag type against the specification of your exact machine — and test before bulk production. Explore the bag ranges: Channel
Vacuum Bags and Vacuum Sealer Bags (smooth). Machine types: nozzle type, non-nozzle type and chamber vacuum sealers. 3. How to Select Material Structure for Commercial Vacuum Packaging Commercial vacuum bags are usually multilayer films. PA (nylon)/PE laminates
are one common structure, but do not assume that every bag with the same material name performs the same way. Barrier properties, puncture resistance and suitability for refrigerated or frozen use depend on the exact layers, resin grades and thickness — and
should be confirmed from the supplier's specification. What to specifyWhy it matters Material structure (for example PA/PE or other multilayer) Affects barrier performance, flexibility and heat-seal behavior Heat-seal layer Determines sealing conditions and
whether the bag suits your sealer Barrier requirement Depends on product sensitivity to oxygen and moisture and your target storage conditions Puncture resistance Important for bone-in products, shellfish, hardware or other sharp items Temperature application
Refrigerated, frozen or heat-treated use should be confirmed against the actual bag specification Food-contact documentation Request the documents that apply to the exact bag and the destination market 4. How Should Importers Specify Bag Size and Thickness?
Bag size is not simply product size. Size must also account for air evacuation, the sealing area and the machine's limits. Supply the following so the supplier can quote the right bag the first time: Bag width and length Inner dimensions, stated clearly as
internal or external. Product dimensions Length, width and height of the packed product, including the thickest point. Headspace Enough open space above the product for air evacuation and a clean seal area. Sealing allowance The opening must not exceed the
sealer's effective sealing length. Thickness In micron or mil, and whether it is total film thickness. Tolerance Agree acceptable dimensional and thickness tolerance in advance. Reading thickness: suppliers may quote micron (µm) or mil. One mil equals 25.4
µm, so 3 mil is about 76 µm and 4 mil is about 102 µm. Always confirm whether the number refers to total thickness or to a single layer, so quotes from different suppliers can be compared fairly. Bag format also matters. Daily Sealing supplies smooth pre-made
vacuum sealer bags for nozzle-type and chamber vacuum sealers, while vacuum roll bags are channel-type bags designed for non-nozzle vacuum sealers. Confirm both the bag format and the machine type before ordering — and decide early whether you need pre-made
pouches or roll stock that your team cuts to length. For help matching bag opening width to machine capacity, see: How to Choose the Right Sealing Length and Sealing Width. 5. Custom Printing for Private Label and Retail Packaging: What to Send the Supplier
This section is not about how printing works — it is about what information a supplier needs from you to quote and produce printed vacuum bags correctly. ProvideWhy the supplier needs it Artwork file and logo Basis for the print layout and any tooling Print
area Defines usable space and keeps print clear of the seal area Colors Affects process choice, cost and setup Barcode or QR code Needs a readable position away from seals, folds and edges Batch or date-coding area A blank, printable zone reserved for lot
codes added later Mandatory labeling Legal text that must appear for your product and market Destination-market requirements Language, symbols and documentation vary by country Two cautions. First, keep key text, logos and codes away from the heat-seal area
so they are not obscured or distorted after sealing; whether print affects sealing performance depends on the laminate structure and where the print layer sits, so confirm this with the supplier. Second, mandatory labeling for food or export products depends
on the product and the destination market — it must be confirmed by the buyer and is not something a print layout can decide. 6. MOQ Is Not the Only Number Bulk Buyers Should Compare Minimum order quantity depends on bag type, size, material, thickness and
printing, so there is no universal figure. For a container-level purchase, buyers should confirm the following items, not MOQ alone: Confirm with the supplierWhy it affects your cost and risk Order quantity per size Several sizes may be treated as separate
production runs Quantity per artwork or design version Each print version can carry its own minimum Sample or pre-production sample Lets you test on your machine before committing Tooling or printing-plate cost, if applicable A one-time cost that changes the
real unit price on smaller runs Production lead time Drives your shipping schedule and stock planning Carton packing Quantity per carton and carton marking affect handling at your end Pallet requirement Affects loading efficiency and freight cost Shipment
volume / CBM Helps buyers plan LCL vs. FCL shipment and compare carton, pallet and loading efficiency Repeat-order consistency Print, dimensions and material should match from batch to batch Every item above is something for the buyer to confirm during quotation.
Actual minimums, lead times and costs are agreed per specification and are not fixed in advance. 7. From Sample Approval to Bulk or FCL Shipment For volume orders, a practical procurement workflow is to confirm the specification and sample before moving into
bulk production and export shipment. The exact sequence and timing depend on the agreed specification and supplier arrangement, so treat the stages below as a checklist rather than a promised schedule. 01 Specification confirmation Bag type, structure, size,
thickness and machine 02 Artwork confirmation Print area, colors, codes and mandatory labeling 03 Sample / pre-production check Review dimensions, print and structure 04 Machine compatibility test Run the sample on your actual vacuum sealer 05 Production approval
Written sign-off on the confirmed specification 06 Bulk production Production against the approved specification and reference sample, where applicable 07 Packing Carton marking, pallet configuration and loading plan 08 Export shipment Shipping documents and
delivery arrangement 8. What Should Be Included in an RFQ for Custom Vacuum Bags? A complete request for quotation shortens the back-and-forth and reduces the risk of a wrong specification. Use the template below and replace the bracketed examples with your
own information. If a value is not yet known, write "to be confirmed" rather than guessing. Product: [for example, frozen meat portions] Bag type: [smooth pouch / embossed channel bag / roll bag] Bag size: [width × length; opening position] Material structure
and thickness: [for example, PA/PE; thickness in µm or mil] Vacuum machine: [brand and model; chamber / nozzle-type / external non-nozzle] Printing: [logo, product information, number of colors, print area] Barcode / QR / date-coding area: [required or not;
preferred position] Estimated quantity: [per size / per design / annual] Destination market: [for example, USA / EU / Middle East] Required documents: [for example, food-contact documentation, material specification] Packing requirements: [carton marking,
pallet, container loading] Shipping information: [destination port, preferred Incoterm if known, estimated FCL / LCL requirement] Target timing: [required arrival window] 9. Why Machine Compatibility Matters Before Bulk Production Many packaging-material suppliers
sell only the bag. Daily Sealing System designs and manufactures vacuum sealing machines and also supplies vacuum sealer bags, with technical support for both. For a bulk buyer this means the bag and the machine can be evaluated as one system — which is exactly
how they perform in production. Do not evaluate the bag independently from the vacuum sealing system. A change in bag structure, thickness or supplier can change how the bag evacuates, seals and holds vacuum. Compatibility check before approving bulk production:
Run the sample bags on your actual vacuum sealer with the real product Confirm air evacuation works properly with the chosen bag type Check seal appearance and continuity after the machine cycle Observe vacuum retention over an internal QC period you define
Re-confirm the sealing settings applicable to your machine — such as sealing time, temperature where adjustable, and cooling time — when the bag structure or thickness changes Record the confirmed settings for repeat production Related technical guides: How
to Set Sealing Time for Impulse, Constant Heat & Band Sealers, Heat Sealing Temperature Guide for Different Packaging Materials, How to Check Heat Seal Integrity: Quality & Leak Inspection Guide. If a new bag produces weak seals, see Why Is My Sealing Machine
Not Sealing Properly? Related Products Channel Vacuum Bags Embossed channel bags and roll bags for non-nozzle vacuum sealers View Series Vacuum Sealer Bags Smooth pre-made pouches for nozzle-type and chamber sealers View Series Chamber Vacuum Sealers For smooth
pouches and moist or liquid products View Series Non-nozzle Vacuum Sealers External machines used with channel bags View Series The following answers are based on Daily Sealing System's sealing-machine manufacturing, vacuum-bag compatibility and after-sales
technical support experience since 2010. Frequently Asked Questions Q1: Can vacuum bags be custom printed for OEM or private-label orders? Custom printed vacuum bags are commonly ordered for OEM and private-label use. Whether a specific bag type, size and
print layout can be produced depends on the material structure, printing process and order conditions, so confirm the details during quotation before committing to a bulk order. Q2: Can both smooth and embossed vacuum bags be printed? This depends on the actual
bag structure and manufacturing process. Smooth and embossed bags should not be assumed to have the same printing conditions, so confirm print feasibility for the specific bag type with the supplier. Q3: What is the minimum order quantity for custom vacuum
bags? There is no universal figure. MOQ is influenced by bag type, size, material, thickness, printing method, number of colors, any tooling or plate requirement and production conditions. It should be confirmed by quotation, together with quantity per size,
quantity per design and lead time. Q4: What information should be included in an RFQ for custom vacuum bags? Include the product, bag type, bag size, material structure and thickness, vacuum machine type, printing requirements, barcode or date-coding needs,
estimated quantity, destination market, required documents and packing requirements. Use "to be confirmed" for anything not yet known rather than guessing. Q5: Should I test the bags on my vacuum machine before ordering in bulk? Yes. Test sample bags on your
actual machine with the real product to confirm air evacuation, seal quality and vacuum retention, and re-confirm the sealing settings applicable to your machine (such as sealing time, temperature where adjustable, and cooling time) if the bag structure, thickness
or supplier differs from your previous bags. Record the confirmed settings for repeat production. Q6: Are all printed vacuum bags suitable for freezing, boiling or microwave use? No. Frozen storage, boiling, hot-fill and microwave use are separate application
requirements. Each must be supported by the exact bag structure and supplier documentation. Suitability for one condition does not automatically mean the bag is suitable for another. Q7: What documents should importers request for food-contact vacuum bags?
Request the material specification and the food-contact documentation that applies to the exact bag and the destination market. The documents required differ by country and product, so confirm what is available and what your market requires before placing
a bulk order. 📖 Further Reading → Vacuum Sealer vs. Continuous Band Sealer: Key Differences, Applications, and Buying Guide → How to Set Sealing Time for Impulse, Constant Heat & Band Sealers → Heat Sealing Temperature Guide for Different Packaging Materials
→ How to Check Heat Seal Integrity: Quality & Leak Inspection Guide → Why Is My Sealing Machine Not Sealing Properly? Common Causes and How to Fix Them → How to Choose the Right Sealing Length and Sealing Width About This Article This article was prepared
by the Daily Sealing System technical team for importers, distributors, private-label brands, food processors, contract packers and procurement teams sourcing vacuum packaging. Daily Sealing System Co., Ltd. is a Taiwan-based manufacturer of sealing equipment
and vacuum sealer bags, with an in-house production facility and experience supporting international B2B buyers. Its product range includes vacuum sealers, smooth vacuum pouches, channel vacuum bags, impulse sealers, constant heat sealers, continuous band
sealers, medical pouch sealers and customized sealing equipment, together with OEM / ODM support and after-sales technical service. The company holds ISO 9001:2015 certification and has patents related to sealing equipment in Taiwan, the United States, Europe,
Germany, Japan and China. See the certificates page for details. This guide is based on Daily Sealing System's sealing-machine manufacturing, vacuum-bag compatibility and after-sales technical support experience since 2010. This article is general buying guidance.
Available bag structures, sizes, printing options, minimum order quantities, lead times and documentation depend on the specific specification and a formal quotation. Food-contact, freezing, heat-treatment and destination-market requirements should be confirmed
against the actual bag specification and supplier documents. Planning a Bulk Order of Custom Printed Vacuum Bags? Send us your product, vacuum machine model, bag type and size, material and thickness requirements, printing needs, estimated quantity and destination
market. Our technical team can help you check bag and machine compatibility and plan the specification before you request a quotation. View Vacuum Sealer Bags Contact Our Technical Team // //
Commercial UV Knife Sterilizer Cabinets: Capacity, Voltage, Rack Design & Bulk Buying Guide Meat plants, seafood processors, central kitchens, butcher operations and food factories handle large numbers of knives every day, and cleaned knives still need
to be stored in a controlled, organized way. A UV knife cabinet is one piece of that hygiene process. For importers, distributors and restaurant-equipment buyers, the harder questions come before the first order: how many knives must one cabinet hold, how
long are the blades, which voltage does the destination market use, and what documents and after-sales support come with the unit? This guide explains how procurement teams compare commercial UV knife sterilizer cabinets by capacity, knife length, rack design,
UV exposure, installation, voltage and safety, and which specifications to confirm before a volume or distributor order. 1. What Is a Commercial UV Knife Sterilizer Cabinet? A commercial UV knife sterilizer cabinet is designed to store cleaned knives inside
an enclosed cabinet while exposing their surfaces to UV light under controlled operating conditions. It should be used as part of a hygiene process, not as a substitute for cleaning. Knives need to be washed and free of residue before they are placed in the
cabinet. The same type of equipment is sold under several names, including UV knife sterilizer, UV knife sanitizer cabinet, UV knife disinfection cabinet and ultraviolet lamp cabinet for knives. These terms are used interchangeably in the market, so buyers
should compare actual specifications — not product names. "Sterilizer" is a common market term for this equipment category; actual microbial-reduction performance depends on the UV source, exposure conditions, cabinet design and supporting test data. Quick
Answer: What Should Buyers Confirm Before Ordering? Before requesting a quotation, confirm the knife quantity, maximum knife length, handle thickness, rack design, installation space, local voltage and frequency, UV safety features, documentation and after-sales
support. Knife quantity: how many knives are stored at one time Knife dimensions: maximum length, blade width and handle thickness Rack design: standard rack, or reinforced rack for wider or heavier knives Installation: wall-mounting space and cabinet dimensions
Electrical configuration: voltage, frequency and plug type for the destination market Safety and maintenance: UV shielding, lamp replacement and spare parts Documents and support: manuals, labeling, warranty and export documents 2. Who Typically Buys UV Knife
Sterilizer Cabinets? Commercial UV knife cabinets are typically considered wherever many knives are shared, used frequently and need to be stored in a central, organized place. Common buyer groups include: End users Meat processing plants Seafood processing
facilities Commercial and central kitchens Butcher operations Food factories Trade buyers Food-processing equipment distributors Restaurant equipment importers Kitchen equipment wholesalers Brands seeking OEM supply Whether a UV knife cabinet satisfies a particular
hygiene regulation, customer audit or import requirement depends on the product, the country and the authority concerned. Buyers should confirm this with their own regulators and customers — it should not be assumed from the equipment type alone. 3. Capacity:
How Many Knives Does Your Facility Need to Store? Start with the working knife set at one station, not with a model number. Capacity falls into three practical categories: Lower-capacity cabinet For a small knife set at one workstation, a small kitchen team
or limited wall space. Reinforced rack design For wider, heavier or longer knives — such as Chinese cleavers or knives with thick handles — where stable positioning matters more than extra capacity. Higher-capacity double-door cabinet For stations or teams
that use more knives at the same time and have enough wall space for a wider cabinet. The specific cabinet models in each category are listed in the product section at the end of this guide. 4. Knife Length, Handle Thickness and Rack Design Capacity alone
does not tell a buyer whether the knives will actually fit and stay stable. A professional specification covers the dimensions of the knives themselves: ConfirmWhy it matters Maximum knife length The longest knife must fit the cabinet; For the three Daily
Sealing models currently listed, the published maximum knife length is 385 mm Blade width Wide blades such as cleavers take up more rack space and can shade neighboring knives Handle thickness Thick handles affect how knives sit in the rack and how much space
they need Rack spacing Spacing between knives affects both stability and UV exposure Stability Knives that swing or shift can overlap each other; baffles or a reinforced rack are designed to help hold them in place Shadowing / obstruction Any part of a blade
hidden from the light receives less exposure (see the next section) 5. Why UV Exposure Depends on Placement UV light treats surfaces it can directly reach. If a blade is overlapped by another knife, or hidden behind a thick handle, the shaded area receives
less UV exposure. This is why packing more knives into a cabinet does not make it more effective. Placement problems typically come from: Overlapping blades One blade partly covers another and blocks the light. Knives placed too close Insufficient spacing
creates shadows between neighboring knives. Handles shading the blade Thick handles or poor angles can hide part of the blade. Surface contamination Residue, grease or other contamination can shield parts of the blade from direct UV exposure. Follow the manufacturer's
cleaning and drying instructions before placing knives in the cabinet. Effectiveness also depends on the UV source, exposure time and distance, none of which can be judged from the cabinet's name. Ask the supplier for the lamp specification and the manufacturer's
recommended operating procedure instead of assuming a fixed exposure time. 6. Installation Requirements for Commercial Buyers Many UV knife cabinets are wall-mounted. Before ordering, confirm the physical and workflow conditions at the installation site: Wall-mounting
space: available wall width and height, and whether the wall can support the cabinet Cabinet dimensions: compare against the wall space and the door-opening clearance Workflow position: a place that suits the movement of cleaned knives from washing to storage
Cleaning access: room to open the doors and wipe down the cabinet Local voltage: a nearby outlet matching the cabinet's electrical configuration Operating environment: kitchen or processing-room conditions such as humidity and washdown practices 7. Voltage
and Destination Market For overseas buyers, electrical compatibility is one of the first things to settle. Before ordering, confirm each of the following with the supplier: ItemWhat to confirm Destination country Where the cabinets will be installed and used
Voltage The mains voltage at the installation site. The product pages of the three Daily Sealing models currently listed show 110V and 220V Frequency 50 Hz or 60 Hz, as used in your market Plug / power configuration Plug type and power-cord arrangement required
locally Local electrical requirements Any electrical or product-marking requirements that apply in your country Buyers should confirm the required electrical configuration before ordering. Availability of a given voltage, frequency or plug arrangement for
a specific order is agreed in the quotation and is not assumed for every market. 8. Safety Questions Buyers Should Ask the Supplier UV-C radiation can be harmful to eyes and skin, so safety design is a core procurement question — more important for an overseas
buyer than a simple "how to use" explanation. Useful questions to put to any supplier: UV shielding: how is the user protected from direct exposure? Viewing window: what material is used and is it UV-protective? Lamp specification: type, power rating and wavelength
Replacement procedure: how are lamps changed safely? Maintenance parts: which parts can be supplied afterwards? Operating instructions: manuals, warning labels and recommended exposure procedure Door-open protection: ask whether the specific cabinet includes
a door interlock or other protection that limits UV exposure when the door is opened Documentation: which certificates or test documents exist for the specific model Verify against the product page, not by assumption. The public product pages list a stainless
steel body, UV glass viewing window and wall-mounted design. Lamp wavelength and model-specific test or certification documents are not stated on the public pages, so buyers should request the documents applicable to the exact product and destination market
during quotation. 9. What Importers and Distributors Should Confirm Before Bulk Ordering For distributor and volume orders, the cabinet specification is only part of the decision. The following are inquiry items to confirm with the supplier — they are not
claims that every item is available: AreaConfirm with the supplier Unit specification Unit dimensions, net weight and gross weight Packing and loading Carton dimensions, quantity per carton, palletization and container loading quantity Electrical Voltage options
for your market Spare parts Spare parts and replacement lamps, and how they are supplied Documents Manuals, labeling and export documents Branding OEM branding requirements, if any After-sales Warranty terms and after-sales support arrangements Daily Sealing's
EN product category page states that the company also offers OEM/ODM and custom-made services. The scope for a specific order — including minimum quantities, lead times and pricing — is confirmed through a formal quotation. 10. RFQ Checklist for Commercial
UV Knife Sterilizers A complete request for quotation shortens the exchange and helps the supplier recommend the right cabinet. Provide as much of the following as you can, and write "to be confirmed" for anything not yet known: Buyer informationWhat to provide
Destination market Country / region Application Food factory / central kitchen / distributor resale Knife quantity Typical number used at one time Knife dimensions Maximum length / blade width / handle thickness Required capacity Lower / reinforced rack /
higher capacity Electrical requirement Voltage / frequency / plug type Installation Wall-mounted / available wall space Order volume Units / mixed models / shipment plan (LCL or FCL) Branding Standard or OEM Documents Required certifications / manuals / labels
Shipping information Destination port, preferred trade term (EXW / FOB / CIF, if known) Daily Sealing UV Knife Cabinets: Product Overview The table maps the three capacity categories to Daily Sealing's current cabinets, using only the specifications published
on the product pages. Details not published there — such as carton size, gross weight and lamp wavelength — should be requested in the quotation. See the full Commercial UV Knife Sterilizer Cabinets category. Buyer needCapacity / rack designKey published specificationsProduct
Small knife set at one station Lower-capacity single-door cabinet; 7 knives 450 x 130 x 580 mm; 10 kg; 110V / 220V; 10W; max. knife length 385 mm; stainless steel body; wall-mounted View productModel DS-C10 Wider, heavier or longer knives Reinforced rack design
(baffle and double shelf); 7 knives 450 x 130 x 580 mm; 10.5 kg; 110V / 220V; 10W; max. knife length 385 mm; stainless steel body; wall-mounted View productModel DS-C10A More knives in use at the same time Higher-capacity twin-door cabinet; 14 knives 810 x
130 x 580 mm; 20 kg; 110V / 220V; 20W; max. knife length 385 mm; stainless steel body; wall-mounted View productModel DS-C15 Lower-capacity cabinet Single door, 7 knives, wall-mounted View Lower-Capacity Cabinet Reinforced rack design Baffle and double shelf
for wider or longer knives, 7 knives View Reinforced-Rack Cabinet Higher-capacity twin-door cabinet Twin door, 14 knives View Twin-Door Cabinet The following answers are based on Daily Sealing System's manufacturing experience since 2010, the published specifications
of its UV knife cabinets, and its technical support for international B2B buyers. Frequently Asked Questions Q1: Is a UV knife sterilizer the same as a UV knife sanitizer or disinfection cabinet? The names are used interchangeably in the market. Compare the
actual specifications — UV source, capacity, rack design, safety features and operating instructions — rather than the product name. Q2: Can a UV knife cabinet replace washing the knives? No. A UV knife cabinet should be used as part of a hygiene process,
not as a substitute for cleaning. Food residue, grease and other surface contamination can reduce direct UV exposure, so knives should be properly cleaned and prepared before being placed in the cabinet. Q3: Does loading more knives improve results? No. Overloading
increases overlap and shadowing, so some surfaces receive less UV exposure. Use the cabinet within its designed capacity and place knives according to the rack layout. Q4: How long should knives stay in a UV cabinet? There is no single exposure time that applies
to every cabinet. The appropriate time depends on the UV source, the cabinet design and the manufacturer's operating instructions, so follow the instructions supplied for the specific model. Q5: What knife length should buyers confirm when choosing a UV knife
cabinet? For the three Daily Sealing UV knife cabinets currently listed, the published maximum knife length is 385 mm. Buyers should confirm the limit of the model they choose, together with blade width, handle thickness and rack design, before ordering. Q6:
What voltage do Daily Sealing's UV knife cabinets use? The product pages of the three currently listed models show 110V and 220V. Buyers should confirm the required voltage, frequency and plug configuration for their destination market before ordering. Q7:
What should an importer or distributor ask before a volume order? Ask about unit and carton dimensions, net and gross weight, quantity per carton, palletization, container loading quantity, voltage options, spare parts and replacement lamps, manuals and labeling,
OEM branding, warranty terms and export documents. Use the RFQ checklist in this guide to organize the request. Q8: Do UV knife cabinets meet food-safety regulations in my country? That depends on the specific model, the country and the authority or customer
concerned, and cannot be assumed from the equipment type. Confirm the applicable requirements with your regulator or customer, and request the documents available for the exact model. Related Products & Resources → UV Knife Sterilizer Cabinets – Product Category
→ Lower-capacity knife cabinet (7 knives) → Reinforced-rack knife cabinet (7 knives) → Higher-capacity double-door cabinet (14 knives) → Contact us for an RFQ About This Article This article was prepared by the Daily Sealing System technical team for importers,
distributors, restaurant-equipment buyers, food processors and central-kitchen procurement teams evaluating commercial UV knife cabinets. Daily Sealing System Co., Ltd. is a Taiwan-based manufacturer with in-house manufacturing capability, serving international
buyers with sealing equipment, vacuum packaging solutions, UV knife cabinets and OEM / ODM support. The company holds ISO 9001:2015 certification and has patents related to sealing equipment in Taiwan, the United States, Europe, Germany, Japan and China. These
company-level credentials should not be read as certification of a particular UV knife cabinet; see the certificates page for what the company holds. The safety guidance in this article is general and draws on public information from the U.S. FDA and CDC/NIOSH,
listed below. This article is general buying guidance. UV wavelength, exposure conditions, microbial-reduction performance, regulatory suitability, minimum order quantities, lead times and documentation depend on the specific model and a formal quotation,
and should be confirmed against the actual product specification and supplier documents. External References CDC / NIOSH: Germicidal UV (GUV) information U.S. FDA: Ultraviolet (UV) Radiation Planning a Distributor or Volume Order of UV Knife Cabinets? Send
us your destination market, knife quantity and dimensions, preferred capacity, voltage and frequency, estimated order volume and any OEM requirements. Our technical team can help you match the cabinet to your application before you request a quotation. View
UV Knife Cabinets Contact Our Technical Team // //
How to Set Sealing Time for Impulse, Constant Heat and Continuous Band Sealers How long should a sealing machine seal a bag? There is no single sealing time that works for every packaging material or sealing machine. The correct heat-sealing process depends
on several variables, including the sealing method, pouch structure, material thickness, seal width, pressure, temperature and production speed. This is especially important for B2B packaging operations because impulse sealers, constant heat sealers, continuous
band sealers and vacuum sealers do not control heat in the same way. For production teams, the goal should not be to find a universal number of seconds — the better approach is to establish a tested and documented sealing condition for the specific machine,
packaging material and production requirement. Quick Answer: How Long Should Sealing Time Be? There is no universal sealing time. Impulse sealers: commonly control heating time or output rather than actual sealing temperature Constant heat sealers: require
the correct combination of temperature, contact time and pressure Continuous band sealers: temperature and conveyor speed must be evaluated together, since line speed changes heat exposure Vacuum sealers: sealing time or temperature depends on machine design,
pouch structure and sealing requirements When material changes: re-test the sealing conditions whenever pouch structure, thickness, supplier or machine configuration changes For industrial production, sealing time should always be treated as one process parameter
rather than a standalone setting. 1. Why Is There No Universal Sealing Time? Heat sealing works by applying sufficient thermal energy to the pouch sealant layer while maintaining the required contact pressure for an appropriate period. This means that two
machines sealing what appears to be the same pouch may still require different settings. Sealing Method Impulse, constant heat and continuous sealing systems transfer heat differently. An impulse sealer heats only during the sealing cycle, while a constant
heat sealer maintains a heated sealing surface. A continuous band sealer moves the pouch through heating and cooling sections. Packaging Material Structure PE, PA/PE, PET/PE and other laminated films use different sealant layers and material structures. The
outer material name alone does not determine the correct sealing time. Material Thickness Thickness affects heat transfer, but a thicker pouch does not automatically mean operators should simply increase temperature or extend heating time. Material structure,
sealant layer and machine capability must also be considered. Seal Width and Pressure Seal width, contact area and pressure can affect how thermal energy is transferred across the sealing zone. A change in sealing width or pressure may therefore require process
settings to be re-tested. Related guide: How to Choose the Right Sealing Length and Sealing Width 2. Impulse Sealers: Start with Heating Time or Output Hand impulse sealers, many foot impulse sealers and other impulse-type machines heat the sealing element
only during the sealing cycle. For this reason, many impulse sealers do not directly control the actual surface temperature. Instead, the operator commonly adjusts heating time, timer level or output. Recommended adjustment process: Confirm the pouch structure
and thickness Start from the machine manual or an existing tested setting Test the actual packaging material used in production Begin with a relatively low setting and increase gradually Change only one major parameter at a time Allow the seal area to cool
appropriately before evaluating the result Record the confirmed machine and material settings Some impulse sealing systems also require a short pressure or cooling period after heating stops. Moving the pouch too early can affect a newly formed seal. Avoid
this common mistake: if a pouch does not seal properly, do not immediately turn the timer to the maximum setting. Excessive heat input may cause pouch shrinkage, melting or burn-through, excessive seal distortion, material sticking, or unnecessary wear on
heating elements or PTFE covers. The objective is not to apply maximum heat — it is to apply enough controlled heat to create a reliable seal without damaging the packaging material. 3. Constant Heat Sealers: Sealing Time Is Only One Part of the Process Constant
heat sealers maintain the sealing jaws or heating surface at a controlled temperature. For these machines, sealing performance depends on the combined effect of sealing temperature, contact or dwell time, sealing pressure, pouch structure and material thickness.
If the temperature is too low, simply holding the pouch longer may not produce a reliable seal. If temperature and dwell time are both excessive, the pouch may distort, thin out or melt through. For constant heat sealing, a better process is: pouch structure
→ suitable temperature range → dwell time → pressure → seal-quality verification — rather than asking only "how many seconds should I seal this bag?" For material-specific temperature guidance, see: Heat Sealing Temperature Guide for Different Packaging Materials.
4. Continuous Band Sealers: Conveyor Speed Changes Heat Exposure A continuous band sealer moves the pouch continuously through a heating section. For this reason, conveyor speed affects how long the packaging material remains exposed to heat. Production ChangePossible
Effect Higher conveyor speed Shorter exposure time in the heating zone; existing temperature settings may provide insufficient heat Lower conveyor speed Longer heat exposure; excessive temperature may distort or overheat the pouch Different pouch thickness
or laminate Temperature and conveyor speed should be re-tested together Temperature and conveyor speed should therefore be treated as linked process variables. A production team that increases line speed without rechecking the sealing condition may see previously
stable seals become weak or inconsistent. Similarly, slowing the line while maintaining an unnecessarily high temperature may create excessive heat exposure. For higher-volume packaging operations, both seal consistency and production throughput should be
considered when validating the settings. Related guide: When Should You Use a Continuous Band Sealer? 5. How Should Sealing Time Be Set on a Vacuum Sealer? A vacuum sealer normally performs at least two different process stages: air evacuation and heat sealing.
The vacuum cycle and the sealing cycle should therefore be evaluated separately. Depending on machine design, the operator may adjust sealing time, temperature or another heat-control setting. Whenever the vacuum pouch supplier, material structure or thickness
changes, the sealing condition should be re-tested — even if the vacuum extraction performance remains unchanged. If Sealing Heat Is Insufficient Incomplete seal formation Weak seal strength Gradual loss of vacuum Leakage after handling or storage If Heat
Input Is Excessive Seal-area distortion Pouch shrinkage Melt-through Weakening of the seal area Always confirm the specific vacuum sealer design and pouch structure before establishing production settings. 6. How Can You Tell If Sealing Time Is Too Short or
Too Long? The seal result provides useful clues, but one symptom does not always point to only one cause. Seal ConditionPossible Direction to Check Seal opens easily or contains unfused areas Heat input may be insufficient; also check material compatibility,
pressure and contamination Seal line shrinks or wrinkles Possible excessive heat or unsuitable settings Pouch melts through or burns Heat input may be excessive The same section repeatedly fails to seal Check heating element, PTFE cover, pressure pad or sealing-area
alignment rather than only increasing time Seal quality changes after switching pouch supplier Re-test material structure, thickness and sealing parameters If increasing sealing time does not improve the result, do not continue increasing it indefinitely.
The problem may instead involve an incompatible packaging material, insufficient or excessive temperature, uneven pressure, contamination in the sealing area, a worn heating element, damaged PTFE material, or other machine-related issues. Related guide: Heat
Sealer Not Sealing Properly? 5 Common Causes and How to Fix Them 7. How to Validate Sealing Time After Changing Packaging Material For manufacturers, food processors, contract packers and other B2B users, a pouch change should be treated as a process change.
This includes changes in packaging supplier, resin or laminate structure, material thickness, bag dimensions, sealing machine, and production speed. 01 Confirm the Packaging Specification Record the material structure, total thickness and sealant layer when
available 02 Confirm the Sealing Machine Type Impulse, constant heat, continuous band or vacuum sealer 03 Establish a Starting Setting Use manufacturer instructions or a previously confirmed condition 04 Keep Other Variables Stable Change only one major parameter
at a time 05 Adjust Gradually Make small changes and compare seal results 06 Allow the Seal to Stabilize Allow sufficient cooling before judging the seal 07 Record the Confirmed Production Setting Document the machine, material and operating parameters 8.
For Production Lines, Do Not Record Only "2 Seconds" or "3 Seconds" For repeat B2B production, a single sealing-time number is usually not enough. If the packaging material or equipment changes later, a record such as "seal for 2 seconds" provides very little
information about why the process originally worked. A more useful production record should include: Sealing machine model Packaging material structure Pouch thickness Sealing time or output setting Sealing temperature, when applicable Conveyor speed for continuous
band sealers Seal width Product type Pouch opening condition Seal inspection result Packaging-material supplier or batch, when relevant This makes it easier to reproduce confirmed conditions and troubleshoot future process changes. 9. B2B Sealing-Process Checklist:
What Information Should Buyers Prepare? When contacting a sealing-machine manufacturer or packaging equipment supplier, providing complete process information can help identify the correct machine configuration and starting settings more efficiently. Prepare:
Current sealing machine model Pouch material structure Pouch thickness Bag opening width Required sealing length Required seal width Product being packaged Dry, oily, powder or liquid product condition Current sealing time or timer setting Current temperature,
when applicable Conveyor speed, when applicable Daily production volume Required production speed Current seal-quality problem Target market or special packaging requirement For OEM / ODM or new packaging projects, this information is also useful when determining
whether the existing sealing method is suitable for the required output and material. The following questions are compiled from Daily Sealing System's manufacturing, packaging-material testing and after-sales technical support experience since 2010. Frequently
Asked Questions Q1: How many seconds should a heat sealer be set for? There is no universal sealing time. The correct setting depends on machine type, pouch structure, thickness, seal width, pressure and other process conditions. Always validate the setting
using the actual production material. Q2: Does a thicker bag always require a longer sealing time? No. Thickness can affect heat transfer, but material structure, sealant layer, temperature, machine output and pressure also influence the result. Thickness
alone should not determine sealing time. Q3: Should I adjust temperature or time on an impulse sealer? Many impulse sealers primarily control heating time or output rather than actual sealing temperature. Machine designs vary, so always confirm the controls
specified for the model. Q4: Why does my continuous band sealer produce weak seals after increasing conveyor speed? Increasing conveyor speed reduces the time the pouch remains in the heating zone. If other parameters remain unchanged, the material may receive
insufficient heat. Re-test temperature and conveyor speed together. Q5: Why does the bag still not seal even after increasing sealing time? The problem may not be insufficient time. Check packaging-material compatibility, sealing temperature or output, pressure,
contamination, heating elements and PTFE components before continuing to increase the setting. Q6: Do sealing settings need to be re-tested when changing pouch suppliers? Yes. Even when the material name and nominal thickness appear similar, the sealant layer,
laminate structure and production specifications may differ. Re-test and document the sealing condition before full production. 📖 Further Reading For sealing-machine buyers, packaging engineers and production teams: → Heat Sealing Temperature Guide for PE,
OPP & Foil Bags → Heat Sealer Not Sealing Properly? Common Causes and How to Fix Them → How to Choose the Right Sealing Length and Sealing Width → When Should You Use a Continuous Band Sealer? → Sealing Machine Maintenance: 7 Ways to Extend Service Life About
This Article This article was prepared by the Daily Sealing System technical team for purchasing teams, packaging engineers, production managers, contract packers and industrial packaging users. Daily Sealing System Co., Ltd. is a Taiwan-based sealing machine
manufacturer with an in-house production facility. The company provides impulse sealers, foot sealers, constant heat sealers, continuous band sealers, vacuum sealers, medical pouch sealers and customized sealing equipment, together with OEM / ODM support and
after-sales technical service. This guide is based on Daily Sealing System's manufacturing, packaging-material testing and after-sales technical support experience since 2010. Actual sealing time, temperature, pressure and conveyor-speed settings vary by machine
model, packaging material and production conditions. Production parameters should always be tested and confirmed using the actual machine and pouch specification. Need Help Determining the Right Sealing Settings for Your Packaging Material? Send us your machine
model, pouch structure, pouch thickness, bag dimensions, product type, current sealing settings, daily production requirement and current seal result. Our technical team can help you evaluate the appropriate sealing-machine configuration and starting process
settings for your packaging application. View Sealing Machines Contact Our Technical Team // //
How to Check Heat Seal Integrity: Seal Quality & Leak Inspection Guide A pouch that looks closed is not necessarily properly sealed. A seal can appear complete while still containing wrinkles, unfused sections, contamination, pinholes, weak bonding or
small leakage paths. In some cases, the problem does not become visible until the package is handled, transported or stored for a period of time. For B2B packaging operations, checking seal quality should therefore go beyond asking whether the two sides of
the pouch are attached. Production and quality-control teams should evaluate seal-line continuity, seal appearance, post-cooling seal condition, leakage or vacuum loss, pouch and pre-made seal integrity, production consistency, and applicable customer or industry
quality requirements. The inspection method should match the packaging material, product and required level of quality assurance. Quick Answer: How Do You Check Whether a Heat Seal Is Good? A practical first-level seal inspection can follow these steps: Inspect
the seal line — it should be continuous and free from obvious wrinkles, burn-through, holes or unfused areas Check the pouch opening — oil, water, powder or product particles should not be trapped in the sealing area Allow the seal to cool — then perform an
appropriate preliminary seal check for easy peeling or recurring weak areas Check for leakage or vacuum loss — inspect the seal, pouch body and original side or bottom seals For production use, establish a QC procedure — do not rely on the appearance of one
sample as proof that the process is stable A visual or manual check is useful for preliminary inspection, but it does not replace formal seal-strength or package-integrity testing when such testing is required. 1. Start with a Visual Inspection of the Seal
Line Visual inspection is usually the fastest first step. A properly formed heat seal should generally appear continuous and consistent, without obvious interruptions or damage. Is the Seal Line Continuous? Check the full sealing length for gaps, unfused sections,
fixed-position defects or significant variation in appearance. If the same position repeatedly fails to seal, the issue may relate to the heating element, PTFE material, pressure pad or sealing-area alignment rather than only the process setting. Are There
Wrinkles? Wrinkles across the seal area can create small leakage channels. This is especially important when sealing gusseted pouches, multi-layer sections, uneven bag openings, or pouches that were not flattened before sealing. Is There Evidence of Excessive
Heat? Check for discoloration, severe shrinkage, material thinning, melt-through or burn marks. These conditions may indicate excessive heat input or a sealing condition that does not match the pouch structure. Is the Seal Area Contaminated? Oil, moisture,
powder, food particles or other product residue can interfere with seal formation. For products with oily, wet or powdery contents, maintaining a clean sealing area is especially important. Related guide: Heat Sealer Not Sealing Properly? 5 Common Causes and
How to Fix Them 2. Allow the Seal to Cool Before Performing a Preliminary Seal Check Heat-sealed material may still be soft immediately after the heating cycle. For this reason, seal quality should not always be judged the instant the pouch leaves the sealing
area. Depending on machine design, the process may include heating time, pressure or dwell time, cooling time, and continued pressure during cooling. After the seal has cooled appropriately, a preliminary manual check can help identify obvious weak bonding.
For example, if the seal opens under very light handling, repeatedly peels at the same position, or contains clearly unfused areas, the sealing condition should be reviewed. However, this type of manual check is only a shop-floor screening method. It should
not be presented as a standardized seal-strength test. For products subject to customer specifications, regulated packaging requirements or formal quality systems, use the required measurement or verification method. 3. How Do You Check a Vacuum Package for
Leakage? A vacuum package can appear normal immediately after sealing and later lose its vacuum. When this happens, inspect several possible leakage locations. Inspection AreaWhat to Check Heat seal line Wrinkles, contamination, unfused sections or interrupted
sealing Pouch body Pinholes, punctures, sharp-product damage or handling damage Original side / bottom seals Leakage from pre-made pouch seams Packaging material Whether the pouch structure and barrier properties are suitable for the application Seal area
Whether heat, pressure and time were sufficient for the material If the vacuum sealer cannot remove air from the beginning, the issue may involve pouch compatibility, air evacuation or the vacuum system rather than seal integrity. This is a different troubleshooting
issue from a package that initially seals correctly and later loses vacuum. Important: Package Expansion Does Not Always Mean Seal Leakage. If a vacuum package gradually expands after sealing, leakage is one possible cause, but it should not automatically
be assumed to be the only cause. Depending on the product and storage conditions, package appearance may also change because of factors such as product gas release or temperature changes. For this reason, investigate seal line → pouch body → original pouch
seams → packaging material → product condition before concluding that the sealing machine is defective. 4. Can You Leave a Package for a Period of Time to Check for Leaks? Yes, a defined observation period can be used as an internal screening method. For example,
a production team may keep vacuum-sealed samples and monitor whether they lose vacuum, rebound or expand, develop visible leakage, or show seal deterioration. However, the observation period should be defined by the company's product and QC requirements. There
is no universal observation time that automatically proves package integrity for every application. For example, "no vacuum loss after 24 hours" may be useful as an internal screening criterion for a particular company or product, but 24 hours is not a universal
industry standard for all vacuum packaging. 5. Formal Seal-Quality Verification Requires More Than Visual Inspection For production packaging, customer acceptance, food packaging, medical packaging or applications with defined quality requirements, visual
inspection alone may not be sufficient. Depending on the product and quality specification, a company may need to evaluate seal strength or peel strength, package integrity or leakage, vacuum retention, package condition after transport or handling, and other
test methods required by the customer, market or application. The appropriate method and acceptance criteria depend on pouch structure, packaging application, product risk, target market, customer specifications, and applicable internal or external quality
requirements. Important scope note: The visual inspection, preliminary manual seal check and observation methods described in this guide are intended for general industrial packaging screening and troubleshooting. They do not replace any formal packaging validation,
regulated test method or customer acceptance standard required for a specific product or industry. 6. Establish a Seal-Quality Sampling Record for Production Once a sealing process enters repeat production, "the machine is running normally" should not be the
only quality criterion. Seal consistency can change because of packaging-material batch variation, material supplier changes, temperature changes, production speed changes, machine wear, heating-element condition, operator handling, contamination, or process-setting
changes. A practical production QC record can include: Sealing machine model Pouch material structure Pouch thickness Pouch supplier or batch Sealing time Sealing temperature Conveyor speed, when applicable Seal width Visual inspection result Preliminary seal
check result Vacuum-loss observation, when applicable Defect samples Adjustment history These records help production teams trace changes when seal quality starts to decline. They also make repeat production more consistent because the process is documented
instead of relying only on operator memory. 7. What Should You Do When Seal Quality Fails Inspection? Once a seal-quality problem is identified, the next step should depend on the symptom. Problem FoundRecommended Direction Weak seal / easy peeling Check material,
sealing temperature, time and pressure Wrinkled or burnt seal Review heat input and pouch compatibility Uncertain sealing time Re-test and document the sealing-time setting Same location repeatedly fails Inspect heating element, PTFE material, pressure area
and alignment Vacuum package gradually loses vacuum Inspect seal line, pouch body and original pouch seams Problem continues after settings are corrected Inspect machine components or contact technical support For sealing-time adjustment, refer to: How to
Set Sealing Time for Impulse, Constant Heat and Continuous Band Sealers For material-specific temperature guidance: Heat Sealing Temperature Guide for Different Packaging Materials For troubleshooting: Heat Sealer Not Sealing Properly? 5 Common Causes and
How to Fix Them 8. B2B Seal-Quality Checklist: What Information Should You Prepare for Technical Support? When discussing a seal-quality problem with a sealing-machine manufacturer or packaging equipment supplier, providing complete application and process
information can help the technical team identify whether the issue is related to the packaging material, process settings or equipment condition. Sealing machine model Sealing method: impulse, constant heat, band or vacuum Pouch structure Pouch thickness Pouch
dimensions Required seal width Product being packaged Dry, oily, wet, powder or liquid condition Sealing temperature Sealing time or timer setting Conveyor speed, when applicable Current seal appearance Whether the seal opens easily Whether the package loses
vacuum Whether the defect always occurs in the same position Daily production volume Applicable customer or quality requirements For OEM / ODM or new packaging projects, this information can also help determine whether the existing sealing method and machine
configuration are suitable for the required material and production conditions. The following answers are based on Daily Sealing System's sealing-machine manufacturing, packaging-material application testing and after-sales technical support experience since
2010. Frequently Asked Questions Q1: How can I tell if a heat seal is properly sealed? Start with a visual inspection. The seal line should be continuous and free from obvious wrinkles, burn-through, contamination and unfused sections. After appropriate cooling,
perform a preliminary seal check and use any additional strength or integrity verification required for the packaging application. Q2: Is a seal good if the pouch looks completely closed? Not necessarily. A pouch can appear closed while still containing weak
bonding, wrinkles, contamination or small leakage paths. Seal appearance is only the first level of inspection. Q3: Is it normal if a heat seal opens easily after cooling? If the seal opens very easily after appropriate cooling, the material, sealing time,
temperature, pressure or equipment condition should be reviewed. Formal acceptance criteria should still follow the applicable product or customer quality requirement. Q4: Does a vacuum package that expands later always mean the seal is leaking? No. Leakage
from the heat seal, pouch body or original pouch seams is one possible cause, but product gas release or storage-temperature changes may also affect package appearance. Inspect both the package and the product condition before drawing a conclusion. Q5: If
a vacuum bag does not leak after 24 hours, is it automatically acceptable? No. A 24-hour observation can be used as an internal screening condition, but it is not a universal acceptance standard for all products or vacuum packaging applications. Q6: Does every
package need to be tested during production? Not necessarily. Whether a company uses 100% inspection or sampling depends on product risk, internal quality procedures, customer requirements and the production process. The inspection frequency and acceptance
criteria should be defined by the applicable quality system. Q7: What is the difference between seal inspection and seal testing? Seal inspection usually includes preliminary checks such as visual condition, continuity, contamination and obvious bonding defects.
Formal seal testing may involve defined strength, integrity or leakage methods with specified acceptance criteria. The required level depends on the packaging application. 📖 Further Reading → How to Set Sealing Time for Impulse, Constant Heat and Continuous
Band Sealers → Heat Sealing Temperature Guide for Different Packaging Materials → Heat Sealer Not Sealing Properly? 5 Common Causes and How to Fix Them → How to Choose the Right Sealing Length and Sealing Width → Sealing Machine Maintenance: 7 Ways to Extend
Service Life About This Article This article was prepared by the Daily Sealing System technical team for purchasing teams, packaging engineers, production managers, contract packers and industrial packaging users. Daily Sealing System Co., Ltd. is a Taiwan-based
sealing machine manufacturer with an in-house production facility. The company provides impulse sealers, constant heat sealers, foot sealers, continuous band sealers, vacuum sealers, medical pouch sealers and customized sealing equipment, together with OEM
/ ODM support and after-sales technical service. This guide is based on Daily Sealing System's sealing-machine manufacturing, packaging-material application testing and after-sales technical support experience since 2010. The inspection methods described here
are intended as general industrial packaging guidance. Where a product is subject to formal quality, regulatory or customer requirements, the applicable test method and acceptance criteria should take priority. Need Help Evaluating Seal Quality for Your Packaging
Application? Send us your machine model, pouch material structure, pouch thickness, bag dimensions, product type, sealing temperature, sealing time, current seal appearance, photos of the defective seal, production volume and applicable quality requirements.
Our technical team can help you identify whether the issue is more likely related to the packaging material, process settings, machine configuration or equipment condition. View Sealing Machines Contact Our Technical Team // //
How to Extend Sealing Machine Service Life: 7 Maintenance and Operating Practices For food processors, manufacturers, contract packers and other B2B packaging operations, a sealing machine is often a critical part of daily production. Equipment condition
can directly affect seal consistency, production throughput, maintenance workload and the risk of unplanned downtime. Even two identical machines can have very different service lives when they are operated under different production conditions. Correct heat-sealing
settings, routine cleaning and timely replacement of worn consumables are three of the most practical ways to reduce unnecessary equipment wear. This guide explains seven maintenance and operating practices for impulse sealers, foot sealers, continuous band
sealers, vacuum sealers and other industrial sealing equipment. Quick Answer: 7 Ways to Extend Sealing Machine Service Life Use the correct heat-sealing settings — avoid excessive temperature or heating time. Use packaging materials compatible with the machine
— confirm pouch structure, thickness and sealing method. Clean the sealing area after production — remove oil, powder and product residue. Operate within the machine's rated duty cycle — do not continuously overload intermittent-duty equipment. Inspect and
replace worn consumables — heating elements, PTFE covers and silicone pads should be checked regularly. Store equipment correctly — protect the machine from moisture, dust and unnecessary environmental exposure. Maintain equipment records — document consumable
replacement, settings and abnormal events. 1. Use the Correct Heat-Sealing Settings Excessive heat is one of the common causes of premature wear on sealing-machine consumables. Production operators sometimes assume that a higher temperature or longer heating
time will always create a stronger seal. In practice, excessive thermal input can shorten the service life of heating elements, PTFE covers and silicone pressure pads while also damaging the packaging material. It is also important to understand that not every
machine directly controls temperature. Impulse sealers typically control heating time or output, while constant heat sealers and continuous band sealers commonly use adjustable temperature controls. Potential Effects of Excessive Heat Heating elements may
oxidize, become brittle or fail sooner PTFE covers or heat-resistant tape may discolor, carbonize or wear faster Silicone pressure pads may deform and reduce pressure uniformity Packaging film may burn, shrink or stick to the sealing surface Heat stress may
increase wear on surrounding machine components Better Sealing-Setting Practice Confirm pouch material, structure and thickness Start from the recommended heat or timing range Run sample seals before full production Re-test when the packaging material or supplier
changes Record validated machine settings for repeat production Related Guide: Heat-sealing conditions vary significantly by packaging material. Refer to our Heat Sealing Temperature Guide for Different Packaging Materials. 2. Use Packaging Materials Compatible
with the Sealing Machine Packaging-material compatibility is an important factor in both seal quality and machine life. Different pouch structures require different heating methods, sealing times, pressures and machine configurations. Using a machine outside
its intended material range may force operators to compensate with excessive heat or extended sealing time, which can increase consumable wear without solving the actual compatibility problem. Common Material-to-Machine Compatibility Issues: Thick foil laminates
on a standard impulse sealer: Some multi-layer foil pouches require stable, adjustable heat that a basic impulse sealing system may not provide. Confirm pouch structure and machine capability before production. Vacuum embossed bags on an incompatible vacuum
system: Embossed vacuum bags are commonly used with specific external vacuum systems. Incorrect bag and machine combinations may result in poor air extraction, weak seals or vacuum loss. Bag width exceeding the sealing length: The full bag opening must fit
within the effective sealing length. Increasing heat cannot compensate for a bag opening that extends beyond the sealing bar. Using excessive temperature to compensate for thick material: Pouch thickness is only one factor. Heat method, dwell time, pressure
and sealing width should be evaluated together. 3. Clean the Sealing Area After Daily Production Routine cleaning is one of the simplest preventive-maintenance practices for sealing equipment. Powder, oil, food particles, adhesive residue and moisture can
accumulate around the sealing area. Repeated heating may carbonize this contamination, affecting heat transfer and gradually damaging PTFE covers, heating elements and pressure surfaces. Daily Cleaning Checklist Remove powder, oil and product residue from
the sealing area Inspect the PTFE surface for contamination or damage Remove carbonized residue around the heating area Inspect the sealing bar and pressure surface Confirm that ventilation openings are not blocked Cleaning Precautions Disconnect the machine
from power before maintenance when required by the equipment manual Allow heated components to cool before cleaning Avoid applying liquid cleaner directly to electrical or heating components Do not scrape PTFE surfaces with sharp or abrasive tools Follow the
machine manufacturer's cleaning instructions 4. Operate Within the Machine's Rated Duty Cycle Different sealing machines are designed for different production volumes and operating patterns. A small impulse sealer used intermittently has a different duty requirement
from a continuous band sealer designed for higher-volume production. For B2B buyers, machine selection should therefore be based not only on sealing length and material type, but also on hourly output, daily production volume and expected operating time. Machine
TypeTypical Operating PatternMaintenance / Operating Consideration Hand Impulse Sealer Intermittent manual sealing for low- to medium-volume packaging Follow the rated duty cycle and observe seal consistency during repetitive operation. If production volume
is consistently high, evaluate a higher-duty machine. Foot Impulse Sealer Repeated manual sealing where hands-free operation improves workflow Monitor seal consistency, heating element condition and production frequency. Avoid exceeding the manufacturer's
recommended duty cycle. Continuous Band Sealer Continuous higher-volume packaging Monitor heater condition, temperature stability, conveyor speed and moving components. Follow the manufacturer's inspection and maintenance schedule. Vacuum Sealer Vacuum extraction
and sealing performed as a production cycle Inspect vacuum-pump performance, sealing components and rated cycle frequency. For oil-lubricated pumps, maintain pump oil according to the equipment manual. 5. Inspect Consumables and Replace Them Before Failure
Affects Production Heating elements, PTFE covers and silicone pressure pads are normal wear components on many sealing machines. Their service life depends on machine type, production frequency, material structure, heat settings and operating conditions. Instead
of replacing consumables only after a complete failure, establish regular inspection points and replace parts when visible wear or seal-quality deterioration appears. This helps reduce the risk of secondary damage and unexpected production interruption. Heating
Element / Heater Wire Inspect when: seal lines become uneven, heating becomes inconsistent, the element shows visible discoloration, deformation or signs of fatigue. Why it matters: a deteriorated heating element may create localized heating problems and can
also damage the PTFE cover or pressure surface. PTFE Cover / Heat-Resistant Tape Inspect when: the surface shows abrasion, holes, burnt areas, contamination or sticking during sealing. Why it matters: damaged PTFE material may allow packaging film to contact
the heating element directly, leading to sticking, contamination and additional component wear. Silicone Rubber Pad Inspect when: the pad becomes hardened, uneven, permanently compressed or visibly damaged. Why it matters: an uneven pressure surface can cause
inconsistent sealing pressure across the seal line. 6. Store Sealing Equipment in a Clean, Dry Environment Equipment condition can deteriorate even during periods when the machine is not in production. Moisture, dust, direct sunlight and poor storage practices
may affect metal components, electrical systems, rubber parts and ventilation paths. Recommended Storage Practices: Keep equipment dry: store machines away from water sources, condensation and excessive humidity. Control dust: use an appropriate protective
cover during extended idle periods while keeping required ventilation areas clear. Avoid direct sunlight and heat: prolonged exposure may accelerate aging of plastics and rubber components. Store power cables correctly: avoid excessive bending, crushing or
tension on the cable and plug. Before restarting after long-term storage: inspect the power cable, heating components, moving parts and machine exterior before trial operation. For vacuum sealing machines: check vacuum-pump condition before restarting. Oil-lubricated
pumps should be inspected and serviced according to the manufacturer's instructions. 7. Keep a Preventive Maintenance and Consumables Record For sealing equipment used every day, a simple maintenance record helps production and purchasing teams understand
component replacement patterns, identify recurring failures and prepare spare parts before a machine stops unexpectedly. Recommended Maintenance Record Items: Machine information: model, serial number, purchase date and production line Consumable replacement:
heating element, PTFE cover, silicone pad and other wear parts Process settings: validated temperature, sealing time and conveyor speed for each packaging material Seal-quality observations: recurring seal defects and corrective actions Abnormal events: unusual
noise, overheating, vacuum loss, electrical issues or emergency maintenance Spare-parts inventory: critical consumables and replacement components currently in stock A maintenance record does not need to be complicated. A spreadsheet, maintenance form or digital
equipment-management system can be sufficient. The key is consistent documentation so that operators, maintenance staff and purchasing teams can identify trends and plan replacement parts in advance. B2B Maintenance Priority Summary Maintenance AreaWhy It
MattersRecommended Action Sealing settings Excessive heat or time increases wear and can damage packaging material Validate settings for each pouch structure and document them Daily cleaning Residue affects heat transfer and consumable condition Clean and
inspect the sealing area after production Consumables Worn parts can cause seal inconsistency and secondary damage Inspect regularly and keep critical spare parts available Duty cycle Equipment selected for insufficient production volume may be overloaded
Match machine type to required output and operating hours Maintenance records Recurring failures and spare-part usage become easier to identify Record replacement dates, failures and process settings Key Principle: Proper sealing settings, routine cleaning
and timely consumable inspection are relatively simple preventive-maintenance practices that can help reduce unnecessary wear and improve production consistency. Sealing Machine Spare Parts and Technical Support from Daily Sealing System Daily Sealing System
Co., Ltd. is a Taiwan-based sealing machine manufacturer with an in-house production facility. Our product range includes impulse sealers, foot sealers, constant heat sealers, continuous band sealers, vacuum sealers, medical pouch sealers and customized sealing
equipment. For maintenance and replacement-part inquiries, buyers can provide the machine model, serial number, packaging material, production frequency and current operating condition. Our technical team can help identify compatible consumables, replacement
parts and maintenance requirements. The following questions reflect common sealing-machine maintenance and service-life concerns from food processors, agricultural packaging companies, electronics manufacturers and industrial packaging users. Frequently Asked
Questions Q1: How long does a sealing machine usually last? There is no universal service-life figure for sealing equipment. Machine life depends on production volume, duty cycle, operating environment, packaging materials, maintenance quality and machine
design. Replaceable parts such as heating elements, PTFE covers and silicone pads should be inspected separately from the main equipment structure. Q2: What commonly causes premature sealing machine wear? Common causes include excessive heat-sealing settings,
contamination around the sealing area, operation beyond the machine's rated duty cycle, incompatible packaging materials and continued use of worn consumables. Regular inspection and correct process settings can reduce these risks. Q3: When should heating
elements and PTFE covers be replaced? Replacement should be based on actual condition rather than a universal calendar interval. Inspect these consumables when seal quality becomes uneven, heating becomes inconsistent, PTFE material is worn or burnt, or packaging
begins sticking to the sealing surface. Q4: Can a hand impulse sealer be used continuously for high-volume production? A hand impulse sealer is generally intended for intermittent manual operation. Actual duty capability varies by model. For sustained higher-volume
production, buyers should compare required output, operating hours and cycle frequency with the machine specification and consider a foot sealer, semi-automatic sealer or continuous band sealer when appropriate. Q5: What maintenance information should purchasing
teams keep for sealing equipment? Keep the machine model and serial number, consumable replacement history, validated sealing settings, maintenance dates, abnormal-event records and spare-parts inventory. These records make it easier to plan preventive maintenance
and source replacement parts before an unexpected shutdown. Further Reading Related guides for sealing-machine buyers, maintenance teams and production managers: → Sealing Machine Maintenance Guide: How Often Should You Service Your Equipment? → Heat Sealer
Not Sealing Properly? Common Causes & Fixes → How to Choose the Right Sealing Length and Sealing Width → Sealing Machine Buying Guide: How to Choose the Right Sealer → When Should You Use a Continuous Band Sealer? About This Article This article was prepared
by the Daily Sealing System technical team for purchasing teams, maintenance personnel, production managers and industrial packaging users. Daily Sealing System Co., Ltd. is a Taiwan-based sealing machine manufacturer with an in-house production facility.
The company manufactures vacuum sealers, impulse sealers, foot sealers, constant heat sealers, continuous band sealers, medical pouch sealers and customized sealing equipment, and provides OEM / ODM support. The company operates under ISO 9001:2015 quality
management practices. Certain products and related packaging materials have CE, FDA, EU No.10/2011 and BPA Free compliance or certifications depending on the product and application. This guide is based on Daily Sealing System's manufacturing, maintenance
and after-sales technical support experience since 2010. Actual maintenance intervals and replacement timing vary by machine model, usage frequency, packaging material and production environment, so always follow the applicable machine manual and maintenance
recommendations. Need Help with Sealing Machine Maintenance or Replacement Parts? Send us your machine model, serial number, packaging material, production frequency and current operating condition. Our technical team can help you evaluate consumables, maintenance
requirements and whether a different machine configuration would better match your production volume. View Sealing Machines Contact Our Technical Team // //
Do Different Packaging Materials Require Different Sealing Temperatures? Heat Sealing Temperature Guide When switching from one packaging material to another, many production teams continue using the same heat sealer settings. This often results in weak
seals, burnt seal lines, pouch deformation, leakage, or inconsistent seal quality. Based on Daily Sealing System's practical experience in sealing machine manufacturing and after-sales technical support since 2010, different packaging materials, sealant layers
and material thicknesses require different heat sealing conditions. Selecting the correct sealing temperature is therefore one of the first steps toward achieving reliable and repeatable seal quality in a B2B packaging operation. A setting that is too low
may result in insufficient bonding, while excessive heat can distort the pouch and accelerate wear on sealing-machine consumables. Quick Answer: Key Principles for Heat Sealing Temperature Settings Different packaging materials require different heat sealing
conditions. Material structure and sealant-layer composition are as important as total pouch thickness. Always re-test sealing settings when changing pouch material, supplier, structure or thickness. A temperature that is too low may cause weak or incomplete
seals. Excessive temperature may burn, distort or melt the packaging material and accelerate consumable wear. For production validation, start from the machine or material supplier's recommended range and adjust incrementally using sample pouches. Temperature
is only one variable — dwell time, pressure, sealing width and conveyor speed can also affect final seal quality. 1. Why Do Different Packaging Materials Require Different Sealing Temperatures? A heat sealer applies thermal energy to the sealant layer of a
pouch or bag. The two inner surfaces soften and bond under controlled heat and pressure, then form a seal as the material cools. Different pouch structures use different sealant materials, thicknesses and laminated layers. This means that the same machine
setting may produce a strong seal on one material but an incomplete or burnt seal on another. When Sealing Temperature Is Too Low Sealant layers do not fully bond Seal line appears closed but opens under light pressure Vacuum bags may lose vacuum after sealing
Thicker laminated pouches may seal inconsistently Parts of the seal line may remain unfused When Sealing Temperature Is Too High Seal line becomes burnt or discolored Pouch material melts through at the sealing area Seal edges become wrinkled or distorted
Thin PE or heat-sealable OPP structures are particularly sensitive Heating elements and PTFE tape may wear faster 2. Reference Heat Sealing Temperature Ranges by Packaging Material The following ranges are intended as starting references for process testing,
not universal production specifications. Actual settings can vary depending on pouch supplier, sealant-layer composition, total material thickness, machine design, sealing pressure, dwell time and production speed. For procurement and production teams, the
safest approach is to confirm the material specification with the pouch supplier and then perform a sample sealing test on the actual machine before mass production. Packaging MaterialStarting Temperature Reference*Typical ApplicationsPurchasing / Production
Notes Thin PE Bags Approx. 120–160°C Snacks, dry products, general lightweight packaging Relatively heat-sensitive. Start conservatively and verify actual material specifications before production. Heat-Sealable OPP / OPP Laminates Approx. 120–160°C Stationery,
lightweight goods, food and retail packaging Confirm that the structure includes a heat-sealable layer. Pure OPP film structures may require different converting or sealing conditions. NY/PE Laminated Vacuum Bags Approx. 170–200°C Meat, seafood, agricultural
products, vacuum packaging Settings depend strongly on laminate thickness, sealant layer and vacuum-sealer design. Confirm seal width and machine compatibility. PET/PE Laminated Pouches Approx. 170–200°C Food packaging, industrial components, general laminated
packaging The PET outer layer provides heat resistance while the inner PE-based sealant layer forms the bond. Process settings must deliver sufficient heat to the sealant layer without damaging the laminate. Aluminum Foil / Foil-Laminated Pouches Approx. 180–220°C
Coffee, tea, pharmaceutical packaging, moisture-sensitive industrial products Thicker foil laminates commonly require an adjustable-temperature constant heat sealer. Confirm pouch structure, sealant layer and equipment compatibility before purchase. Thick
Multi-Layer Laminated Pouches May require 200°C or above depending on structure Heavy industrial products, agricultural bulk packaging, specialty packaging Do not increase temperature alone. Dwell time, sealing pressure, sealing width and heating method should
be evaluated together. Important: The temperature ranges above are starting references only. Packaging films with the same generic material name can use different resin grades, sealant layers and laminate structures. Whenever the pouch material, supplier,
thickness or structure changes, run a new sealing test before starting production. 3. How to Determine the Correct Heat Sealing Temperature There is no single sealing temperature that works for every material and every heat sealer. For B2B production, the
correct approach is to establish a controlled test procedure and document the validated setting for each packaging material. 01 Identify the Material Confirm pouch structure, sealant layer and thickness — for example PE, NY/PE, PET/PE or foil laminate. 02
Set a Starting Point Use the machine manufacturer's or packaging-material supplier's recommended range as the starting point. 03 Run Sample Seals Use production-equivalent sample pouches and inspect seal appearance, continuity and initial seal strength. 04
Adjust Incrementally Increase heat gradually if the seal is weak. Reduce the setting if the pouch burns, distorts or melts. 05 Document the Setting Record pouch supplier, material structure, thickness, machine model, temperature and other relevant process
settings. 4. How Can You Verify Whether the Seal Is Strong Enough? Temperature setting alone does not confirm seal quality. After establishing an initial setting, the production team should verify the actual seal according to the packaging requirements and
internal quality-control criteria. Practical Seal Quality Checks: Visual Inspection: The seal line should be continuous and even, without burn marks, excessive wrinkles, holes or obvious unfused sections. Manual Pull Check: Apply even force to both sides of
the sealed area. A properly bonded seal should not peel open easily under normal handling conditions. Vacuum Hold Observation: For vacuum packaging, monitor the package over a defined internal QC period to check for loss of vacuum, leakage or package rebound.
A 24-hour observation may be used as an internal screening step, but it is not a universal industry standard. Production QC Testing: For applications with defined seal-integrity requirements, consider peel-strength, leak, burst or vacuum-decay testing according
to your internal quality specification. Cross-Section Review: For troubleshooting, inspect the seal area for uniform fusion and signs of delamination. 5. Six Common Heat Sealing Temperature Mistakes 1. Changing Pouch Material Without Re-Testing Even materials
with the same generic name can use different resin grades, thicknesses and sealant layers. Re-test whenever the pouch supplier or specification changes. 2. Assuming Higher Temperature Means a Stronger Seal Excessive heat can damage the pouch, distort the seal
area and accelerate wear on heating elements and PTFE tape. 3. Ignoring Heat Build-Up During High-Volume Production During extended production runs, equipment temperature and process conditions may change. Periodically inspect seal quality instead of assuming
the first validated setting remains optimal throughout the shift. 4. Looking Only at Material Thickness Thickness matters, but laminate structure, sealant layer, dwell time, sealing pressure and heating method can be equally important. 5. Sealing Through Oil,
Moisture or Powder Contamination at the bag opening can prevent proper bonding even when the temperature setting is correct. Keep the sealing area clean and dry before sealing. 6. Using the Wrong Heating Method for Thick Foil Laminates Some thick multi-layer
foil pouches require stable, adjustable heat that a standard impulse sealer may not provide. Confirm the pouch sealant structure and machine capability, and evaluate an adjustable-temperature constant heat sealer when required. 6. How Sealing Settings Differ
by Machine Type Not every sealing machine controls heat in the same way. For purchasing teams, understanding the difference between time-controlled impulse sealing and temperature-controlled constant heat sealing is especially important. Sealing Machine TypePrimary
Setting MethodB2B Purchasing / Production Notes Hand Impulse Sealer Sealing time / heating-time control rather than direct temperature setting Commonly used for PE and other compatible plastic bags. Material compatibility should be confirmed before purchasing.
Foot Impulse Sealer Heating-time control Suitable for repetitive manual packaging where hands-free operation improves workflow. High-frequency use requires monitoring of seal consistency. Constant Heat Sealer Direct adjustable temperature control Often preferred
for foil laminates, vacuum nylon bags and other thicker or multi-layer packaging materials requiring stable continuous heat. Continuous Band Sealer Temperature setting + conveyor speed Designed for higher-volume production. Temperature and line speed must
be optimized together to maintain consistent heat input. Vacuum Sealer Sealing time or temperature depending on machine design Vacuum extraction and sealing are separate process stages. Confirm bag type, sealing method, seal width and production requirements
before equipment selection. 7. Continuous Band Sealer: Why Temperature and Conveyor Speed Must Be Adjusted Together For a continuous band sealer, seal quality is determined by the combined effect of temperature, conveyor speed and material characteristics.
Higher conveyor speed → shorter exposure time in the heating zone → process settings may need adjustment to maintain sufficient heat input. Lower conveyor speed → longer heat exposure → excessive temperature may distort or burn the pouch. Whenever pouch structure,
thickness or conveyor speed changes, re-test the sealing conditions. Use sample material before a full production run and confirm that the seal line is continuous, undamaged and sufficiently strong for the intended application. B2B Buyer Checklist: Information
to Prepare Before Selecting a Heat Sealer Packaging material structure: PE, OPP laminate, NY/PE, PET/PE, foil laminate, etc. Total pouch thickness and sealant-layer specification Bag opening width and required sealing length Required sealing width or number
of seal lines Product type: dry, oily, powder, liquid, food, industrial component or medical product Daily production volume and required cycle speed Current sealing temperature, time or conveyor-speed settings Required seal-integrity or internal QC criteria
Available power supply and production-line configuration Daily Sealing System Can Help Evaluate the Right Sealing Conditions for Your Packaging Material Daily Sealing System Co., Ltd. is a Taiwan-based sealing machine manufacturer with an in-house production
facility. Our product range includes impulse sealers, constant heat sealers, foot sealers, continuous band sealers, vacuum sealers, medical pouch sealers and customized sealing equipment. For a new packaging project, buyers can provide the machine model, pouch
structure, material thickness, bag dimensions, product type and daily output requirement so our technical team can help evaluate the appropriate sealing-machine configuration and starting process settings. The following questions are based on common sealing-temperature
and packaging-material inquiries handled by Daily Sealing System's technical and after-sales service team across food processing, agricultural packaging, electronics manufacturing and industrial packaging applications. Frequently Asked Questions Q1: Do different
packaging materials require different sealing temperatures? Yes. Different packaging films use different sealant layers, resin structures and thicknesses, so the same temperature setting may produce a weak seal on one material and burn another. Whenever the
material, supplier, laminate structure or thickness changes, the sealing conditions should be re-tested before production. Q2: Does a higher sealing temperature always produce a stronger seal? No. The goal is to apply enough thermal energy to create a reliable
bond without damaging the pouch. Excessive heat can distort the seal area, melt through the bag, weaken the laminate structure and accelerate wear on sealing-machine consumables. Q3: What type of sealer is recommended for aluminum foil or laminated foil pouches?
Thick multi-layer foil laminates often require stable, adjustable heat so that sufficient thermal energy reaches the inner sealant layer. An adjustable-temperature constant heat sealer is commonly evaluated for these applications. However, machine selection
should be based on the actual pouch structure, thickness, sealing width and production requirements rather than material name alone. Q4: How should I adjust the temperature of a continuous band sealer? Continuous band sealing depends on both temperature and
conveyor speed. Increasing line speed reduces the time the pouch remains in the heating zone, while slower speed increases heat exposure. Whenever the material or production speed changes, test both parameters together and confirm seal quality before full
production. Q5: How do I know whether my heat sealing temperature is correct? Start with a visual inspection: the seal line should be continuous and free from burns, holes and obvious unfused sections. Then perform an appropriate strength or leak check for
the packaging application. For vacuum packaging, monitor whether the package maintains vacuum over your defined QC observation period. Once the process is validated, record the material specification, machine model and sealing settings for repeat production.
Further Reading Related technical guides for sealing-machine buyers, production managers and packaging engineers: → Heat Sealer Not Sealing Properly? 5 Common Causes & Fixes → Sealing Machine Maintenance Guide: How Often Should You Service Your Equipment?
→ How to Choose the Right Sealing Length and Sealing Width → Sealing Machine Buying Guide: How to Choose the Right Sealer → When Should You Use a Continuous Band Sealer? About This Article This article was prepared by the Daily Sealing System technical team
for purchasing teams, packaging engineers, production managers and industrial packaging users. Daily Sealing System Co., Ltd. is a Taiwan-based sealing machine manufacturer with an in-house production facility. Our product portfolio includes vacuum sealers,
external vacuum sealers, chamber vacuum sealers, impulse sealers, constant heat sealers, foot sealers, continuous band sealers, medical pouch sealers and customized sealing equipment. The company holds ISO 9001:2015 certification. Certain products and related
packaging materials carry CE, FDA, EU No.10/2011 and BPA Free certifications. Patents are registered in Taiwan, the United States, Europe, Germany, Japan and China. The content in this guide is based on Daily Sealing System's practical manufacturing experience,
packaging-material testing and after-sales technical support since 2010. The temperature ranges provided are starting references only; actual production settings should always be validated using the specific pouch material and machine configuration. Need Help
Matching Your Packaging Material to the Right Heat Sealer? Send us your pouch material, thickness, bag size, product type, required daily output and current sealing-machine model. Our technical team can help you evaluate the appropriate sealing-machine configuration
and starting process settings for your packaging application. View All Sealing Machines Contact Our Technical Team // //
How Often Should You Maintain Your Sealing Machine? Preventive Maintenance Guide for Better Seal Quality Sealing machines are critical equipment in food processing, agricultural packaging, electronics, and industrial manufacturing — but many operators
only consider maintenance after a seal quality problem has already appeared. Waiting until failure typically means higher repair costs, unexpected production downtime, and avoidable product loss. Based on Daily Sealing System's practical experience in sealing
machine manufacturing and after-sales technical support since 2010, the majority of seal quality problems can be prevented through consistent preventive maintenance. This guide explains how often to maintain your sealing machine, what to inspect at each interval,
and how to identify when consumable parts need to be replaced. Quick Answer: How Often Should You Maintain a Sealing Machine? Most sealing machines should be inspected weekly or monthly depending on production volume. Here is the recommended schedule by usage
level: Occasional use: Full inspection every 3–6 months Daily use: Monthly inspection of heating wire (nichrome wire), PTFE tape, and seal quality High-volume continuous production: Weekly inspection of heating system, consumables, and full machine cleaning
Any usage level: If seal quality declines at any point, inspect consumables immediately — do not wait for the next scheduled date Regular maintenance helps extend the service life of sealing machines and prevents most seal quality problems before they affect
production output. 1. Why Do Sealing Machines Need Preventive Maintenance? A sealing machine relies on its heating wire (nichrome wire), PTFE tape (Teflon tape), heating system, and pressure mechanism to create a consistent seal. All of these components are
subject to natural wear over time. A preventive maintenance schedule reduces unexpected downtime and repair costs — and allows problems to be identified and corrected before they escalate into seal failures or production stoppages. Consequences of Neglected
Maintenance Weak or incomplete seals — increased leakage risk Burnt or discolored seal lines Uneven seal appearance affecting product presentation Reduced sealing throughput Significantly shortened equipment service life Higher repair and replacement costs
Benefits of Regular Preventive Maintenance Consistent seal quality across every production run Reduced risk of unexpected equipment failure Extended overall equipment service life Lower repair and consumable costs over time Reduced packaging defect rate Improved
production line reliability and uptime 2. Sealing Machine Maintenance Schedule There is no single fixed maintenance interval that applies to all sealing machines. The right schedule depends on usage frequency, daily output volume, and bag material type. From
Daily Sealing System's after-sales service experience, machines sealing aluminum foil or thick laminated bags wear through consumables noticeably faster than those sealing standard PE bags — and should be inspected more frequently. Usage FrequencyRecommended
Maintenance IntervalMain Inspection Items Occasional use (less than daily) Every 3–6 months Consumable appearance, power cable, seal quality test Daily regular use Monthly Heating wire, PTFE tape, silicone strip, full cleaning High-volume continuous production
Weekly Heating wire, PTFE tape, heating system, full machine cleaning Any usage level — seal quality declines Immediately Inspect consumables first — do not wait for the next scheduled date 📌 Key principle: Most sealing quality problems can be prevented through
routine maintenance. If seal quality starts declining between scheduled maintenance dates, check consumables immediately — this is almost always the fastest, lowest-cost solution. 3. Preventive Maintenance Checklist Use this checklist to establish a consistent
maintenance routine across your production operation. Heating wires (nichrome wire) and PTFE tape (Teflon tape) are consumable parts that require periodic replacement — but proper daily care extends their service life considerably. ⚙️ Before Every Shift ☐
Visually inspect PTFE tape surface ☐ Check heating wire appearance ☐ Run a test seal with a scrap bag ☐ Confirm temperature setting is correct 🗓 Daily (End of Shift) ☐ Clean sealing area — remove powder, oil, debris ☐ Inspect PTFE tape for damage or burn
marks ☐ Confirm heating wire shows no discoloration ☐ Allow machine to cool before shutdown 📅 Weekly ☐ Inspect heating wire for uneven width or gaps ☐ Check PTFE tape for holes or worn areas ☐ Check all screws and fasteners for looseness ☐ Verify temperature
settings vs. production requirements 🔧 Monthly ☐ Replace PTFE tape proactively if showing wear ☐ Inspect power cable for visible damage ☐ Deep clean the full sealing area ☐ Review seal quality trend from past month 📋 Quarterly ☐ Full equipment inspection
☐ Replace heating wire if showing any deterioration ☐ Test temperature calibration accuracy ☐ Contact manufacturer if performance has declined 4. Heating Wire (Nichrome Wire) Replacement: When and How to Tell The heating wire — also referred to as nichrome
wire or sealing wire — is a primary consumable component in impulse sealers and continuous band sealers. It has no fixed replacement interval. Replacement timing depends on usage frequency, bag material type, and observed seal quality. From Daily Sealing System's
technical service experience, machines sealing thicker materials or running high daily volumes will wear through heating wire (nichrome wire) significantly faster. Signs the heating wire (nichrome wire) needs replacing: Seal line width is uneven — some sections
visibly narrower than others Gaps or unheated sections appear within the seal line Heating is non-uniform — part of the seal holds, other sections do not Heating wire appears visibly discolored, brittle, or has broken through Increasing temperature does not
improve seal quality Heating wire (nichrome wire) is a user-replaceable consumable on most sealing machine models. Daily Sealing System can supply original-specification replacement parts and confirm the correct part number for your machine model. 5. PTFE
Tape (Teflon Tape) Replacement: When and How to Tell PTFE tape (Teflon tape) acts as a non-stick barrier between the bag material and the heating wire, preventing the bag from sticking to the sealing bar during heat bonding. PTFE tape wear is one of the most
commonly overlooked causes of declining seal quality. Signs PTFE Tape Needs Replacing Bag material sticks to the sealing bar during operation Irregular pressure marks or uneven texture on the seal line surface Visible holes, tears, or burnt areas on the tape
surface Overall seal line appearance has declined without another obvious cause Replacement Notes Ensure the machine has fully cooled before replacing PTFE tape Confirm the new tape matches the original manufacturer specification Apply the tape flat — no wrinkles
or bubbles Run a test seal with a scrap bag after installation Contact the manufacturer if unsure of the correct specification 6. What Can You Handle In-House — and When to Call a Technician? Most routine sealing machine maintenance can be performed by the
equipment operator without specialist tools. Issues involving internal components or control systems should be handled by a qualified technician to avoid additional damage or warranty issues. Maintenance TaskIn-HouseContact Manufacturer Clean sealing area
✅ Replace heating wire (nichrome wire) ✅ Most models Replace PTFE tape (Teflon tape) ✅ Per operating manual Check and tighten fasteners ✅ Visual check of power cable ✅ Temperature control malfunction or display error ✅ Control board failure ✅
Motor noise or abnormal vibration ✅ Vacuum system not achieving vacuum ✅ Progressive overall performance decline ✅ 7. Operational Habits That Extend Sealing Machine Service Life Beyond scheduled maintenance, daily operating habits have a direct impact
on how long a sealing machine performs reliably. Based on Daily Sealing System's after-sales technical service experience, premature equipment wear is often caused by operating practices rather than product quality issues. Use Compatible Bag Materials Mismatched
bag materials accelerate consumable wear. Before sealing a new material type — PE bags, aluminum foil, or vacuum bags — confirm it is compatible with your machine's heating method and temperature range. Set the Correct Sealing Temperature Running at excessively
high temperatures is one of the primary causes of accelerated consumable degradation. Set temperature based on the bag material specification — not higher than necessary to achieve a reliable seal. Do Not Exceed Operating Limits Impulse sealers and foot sealers
have recommended continuous operation limits. During high-frequency use, allow brief cooling intervals to prevent overheating and premature component wear. Replace Consumables Proactively Do not wait for a machine failure before replacing consumables. Proactively
replacing heating wire (nichrome wire) and PTFE tape on a maintenance schedule significantly reduces the risk of unexpected production stoppages. Related Products If your sealing machine is consistently underperforming despite regular maintenance, it may be
time to evaluate whether a different machine type better fits your current bag material or production volume requirements. Impulse Sealers PE bags, OPP bags, light packaging View Series Continuous Band Sealers High-volume production line sealing View Series
Vacuum Sealers Meat, seafood, food preservation View Series Medical Pouch Sealers Sterilization pouches, medical packaging View Series The following questions are compiled from Daily Sealing System's after-sales technical service experience across food processing,
agricultural packaging, electronics manufacturing, and industrial packaging clients since 2010. Frequently Asked Questions Q1: How often should I maintain my sealing machine? Most sealing machines should be inspected weekly or monthly depending on production
volume. Machines used occasionally should be checked every 3–6 months. Daily-use machines should receive monthly maintenance. High-volume production equipment should be inspected weekly. Regardless of schedule, if seal quality declines at any point, inspect
consumables immediately. Q2: Does declining seal quality always require professional repair? Not necessarily. When seal quality declines, the first step is always to inspect the heating wire (nichrome wire) and PTFE tape — these consumables are the most common
cause of seal quality problems. In many cases, replacing one or both resolves the issue without any professional repair. If quality does not improve after replacing consumables, contact the manufacturer for technical diagnosis. Q3: How often does the heating
wire (nichrome wire) need to be replaced? Heating wire (nichrome wire) has no fixed replacement interval — timing depends on usage frequency and bag material. When the seal line becomes uneven, develops gaps, or the wire shows visible discoloration or brittleness,
replace it promptly. Machines used for high-volume daily production or sealing thicker materials such as aluminum foil bags will wear through heating wire more quickly. Q4: Can I replace the PTFE tape (Teflon tape) myself? Yes, on most sealing machine models
PTFE tape can be replaced in-house without specialized tools. Allow the machine to cool completely before replacing. Confirm the replacement tape matches the original specification. Run a test seal with a scrap bag after installation to confirm correct fit
and restored seal quality. Contact the manufacturer if you are unsure of the correct specification for your model. Q5: Does a sealing machine need to be cleaned regularly? Yes. After each production shift, clean the sealing area to remove powder, oil residue,
food debris, and moisture. Residue buildup directly accelerates PTFE tape and heating wire (nichrome wire) degradation, and is a common contributing factor to seal quality problems. Use a dry cloth and confirm the machine has fully cooled before cleaning —
avoid applying liquid cleaners directly to heating elements. Q6: How can preventive maintenance reduce downtime? Preventive maintenance reduces downtime by identifying consumable wear and developing performance issues before they cause a production stoppage.
Replacing a heating wire or PTFE tape during a scheduled maintenance window takes minutes. Waiting until the machine fails mid-production means unplanned downtime, delayed shipments, and potentially wasted product. A consistent maintenance schedule converts
reactive repair time into planned, controlled maintenance windows — significantly improving overall equipment availability and production reliability. 📖 Further Reading Related articles on sealing machine troubleshooting, selection, and performance: → Heat
Sealer Not Sealing Properly? 5 Common Causes and How to Fix Them → How to Choose the Right Sealing Machine Based on Product Type → How to Choose the Right Sealing Length and Sealing Width → Vacuum Sealer vs. Continuous Band Sealer: Which Should You Choose?
→ When Should You Use a Continuous Band Sealer? About This Article This article was prepared by the Daily Sealing System technical team. It is intended as a practical maintenance reference for packaging engineers, production managers, purchasing teams, and
industrial packaging operators. Daily Sealing System Co., Ltd. is a Taiwan-based sealing machine manufacturer with an in-house production facility. Our product range includes vacuum sealers, external vacuum sealers, chamber vacuum sealers, continuous band
sealers, foot sealers, impulse sealers, medical pouch sealers, and customized sealing equipment. The company holds ISO 9001:2015 certification. Certain products and related materials carry CE, FDA, EU No.10/2011, and BPA Free certifications. Patents are registered
in Taiwan, the United States, Europe, Germany, Japan, and China. Content in this article is based on Daily Sealing System's practical manufacturing experience and after-sales technical service since 2010. The recommendations provided in this article are intended
for general industrial sealing applications. Maintenance intervals may vary depending on machine model, production volume, and packaging material. Need Help Identifying the Correct Maintenance Schedule for Your Sealing Machine? Our technical team can recommend
the appropriate consumables and maintenance intervals based on your machine model and production requirements. Share your machine model and current situation — we'll recommend the most appropriate solution. ✓ Heating wire (nichrome wire) — original specification
✓ PTFE tape (Teflon tape) — multiple widths available ✓ Technical consultation and maintenance guidance ✓ Equipment repair support View All Sealing Machine Series Contact Our Technical Team // //
Heat Sealer Not Sealing Properly? 5 Common Causes and How to Fix Them Sealing machines are straightforward to operate — but seal quality problems are more common than most users expect. Wrinkled seal lines, seals that open under light pressure, burnt or
discolored seal lines, and vacuum-sealed bags that lose vacuum quickly are all issues that packaging operators regularly encounter. In most cases, the problem is not a machine failure — it is caused by incorrect temperature settings, incompatible bag material,
worn consumables, contamination at the bag opening, or operator technique. This guide covers the five most common causes of poor seal quality, a practical diagnostic table, and a maintenance checklist to help you identify and resolve the issue quickly. Quick
Answer: Why Is My Heat Sealer Not Sealing? Most heat sealer problems are caused by one of these five issues: Incorrect sealing temperature — too high or too low, both cause seal failure Wrong bag material — incompatible material leads to weak seals or burnt
bags Worn heating wire — degraded wire causes uneven or incomplete sealing Damaged Teflon tape — worn tape produces wrinkled, uneven seal lines Contamination at the bag opening — oil, moisture, or powder prevents proper heat bonding Most issues can be resolved
without replacing the machine. Start by checking consumables and temperature settings before contacting a technician. 1. Incorrect Sealing Temperature Sealing temperature is the most direct factor affecting seal quality. Based on Daily Sealing System's practical
experience in sealing machine manufacturing and after-sales technical support since 2010, incorrect temperature settings are the single most common cause of poor seal quality. Different bag materials and thicknesses require significantly different sealing
temperatures — and what works for one material can burn or fail to bond another. Symptoms: Temperature Too Low Seal line appears closed but opens under light pressure Seal area looks hazy or incompletely fused Vacuum-sealed bags lose vacuum quickly after sealing
Thicker bag materials seal inconsistently or fail entirely Symptoms: Temperature Too High Seal line is burnt, discolored, or blackened Bag material melts through or distorts at the seal area Seal line edges are uneven or charred Thin PE or OPP bags are particularly
susceptible Recommended fixes: Start from the mid-point of the manufacturer's recommended temperature range and adjust incrementally When switching to a new bag material, always re-test and recalibrate the temperature setting Thicker bag materials generally
require higher sealing temperatures During extended high-volume runs, machine temperature may gradually rise — monitor and adjust as needed 2. Incompatible Bag Material Not all sealing machines are compatible with all bag materials. Based on Daily Sealing
System's after-sales service experience across food processing, agricultural packaging, and industrial clients, bag material mismatch is one of the most frequently overlooked causes of seal quality problems. Different materials have different melting points
and bonding characteristics. Bag MaterialCommon ProblemRecommended EquipmentTypical Application Thin PE bags Burns easily if temperature is too high Impulse sealer Snacks, tea, dry food Aluminum foil / laminated pouches Insufficient bond if temperature is
too low Adjustable-temperature constant heat sealer Coffee, pharmaceuticals, industrial parts Vacuum channel bags Cannot achieve vacuum; seal leaks quickly Vacuum sealer Meat, seafood, fresh produce Medical sterilization pouches Seal does not meet medical
packaging standards Medical pouch sealer Medical devices, surgical instruments 3. Worn Heating Wire or Teflon Tape The heating wire and Teflon tape (PTFE heat-resistant tape) are the primary consumable components of a sealing machine. Daily Sealing System's
after-sales technical team consistently finds that a large proportion of seal quality complaints can be resolved simply by replacing worn consumables — without any need for machine repair. Both components degrade naturally with use and directly affect sealing
performance. Signs: Heating Wire Needs Replacing Uneven seal line width along the sealing bar Visible gaps or unheated sections within the seal line Non-uniform heating — partial sections seal, others do not Heating wire appears visibly discolored, brittle,
or broken Signs: Teflon Tape Needs Replacing Bag material sticks to the machine during sealing Irregular pressure marks on the seal line surface Visible holes, tears, or burnt areas on the tape surface Overall seal line appearance quality has declined When
to Replace When seal quality drops without a clear cause When heating wire shows visible discoloration or brittleness When Teflon tape shows visible wear, holes, or burn marks As part of scheduled routine maintenance checks 4. Contamination at the Bag Opening
The sealing area must be completely clean for heat bonding to work effectively. Oil, moisture, powder, or food residue at the bag opening creates a barrier between the two layers of bag material — preventing proper fusion and causing seal failure or leakage.
This is one of the most common operational causes of poor seal quality in food processing environments. Common contamination sources and recommended actions: Oil or sauce residue: Avoid contaminating the bag opening during filling. If residue is present, wipe
the opening clean with a dry cloth before sealing Moisture or high-water-content products: Ensure the bag opening is dry before sealing. For liquid products, a chamber vacuum sealer allows flat-position operation, minimizing liquid migration to the seal area
Powder residue (coffee, flour, spices): Confirm the bag opening is free of powder before sealing — even a small amount of contamination will prevent a reliable seal Overfilled bags: Leave adequate clearance above the fill level to ensure a clean area for sealing
5. Incorrect Operator Technique Even with the correct machine, bag material, and temperature setting, poor operator technique can still produce inconsistent seal results. This is particularly relevant for impulse sealers and foot sealers, where manual handling
directly affects the final seal quality. Common operator issues and recommended corrections: Bag opening not pulled flat before sealing: Wrinkles in the bag opening are the most common cause of an uneven seal line — always flatten the bag opening before applying
the seal Insufficient dwell time: On impulse sealers, releasing the pressure bar before the material has fully fused produces a weak seal — maintain pressure for the full recommended dwell time Misaligned bag opening: If the bag opening is not centered on
the sealing bar, part of the opening may not be sealed, leaving an unsealed gap High-frequency continuous operation: Impulse sealers require a brief cooling interval between seals — operating too rapidly can cause inconsistent results 6. Seal Problem Diagnostic
Table Based on Daily Sealing System's after-sales technical service experience, the following table covers the most common seal quality symptoms, their likely causes, recommended corrective actions, and whether the fix can be handled in-house: SymptomMost
Likely CauseRecommended ActionDIY Fix? Seal opens under light pressure Temperature too low or dwell time too short Increase temperature; extend dwell time ✅ Yes Seal line burnt or discolored Temperature too high Reduce temperature; confirm bag material compatibility
✅ Yes Wrinkled or uneven seal line Bag opening not flattened; Teflon tape worn Flatten bag before sealing; replace Teflon tape ✅ Yes Seal leaks (non-vacuum bag) Contamination or insufficient seal strength Clean bag opening; increase temperature or seal width
✅ Yes Vacuum bag loses vacuum quickly Incompatible bag material or seal width too narrow Confirm bag type; evaluate wider seal width machine ⚠️ Partial Uneven seal line width or gaps Heating wire worn or damaged Inspect and replace heating wire ✅ Yes Bag material
sticks to machine Teflon tape worn or temperature too high Replace Teflon tape; reduce temperature ✅ Yes Seal position offset or skewed Bag not centered on sealing bar Adjust handling; center bag on sealing bar ✅ Yes Problem persists after consumable replacement
Temperature control or internal component failure Contact manufacturer technical support ❌ Contact manufacturer 7. Sealing Machine Maintenance Checklist Consistent preventive maintenance significantly reduces the frequency of seal quality problems. Use this
checklist to establish a routine maintenance schedule for your sealing equipment: 🗓 Daily ☐ Clean sealing area — remove powder, oil, and debris ☐ Visually inspect Teflon tape for surface damage ☐ Confirm heating wire appearance (no visible discoloration)
☐ Run a test seal before starting production 📅 Weekly ☐ Inspect heating wire for uneven width or gaps ☐ Check Teflon tape for holes or burn marks ☐ Check all screws and fasteners for looseness ☐ Verify temperature settings against production requirements
🔧 Monthly ☐ Replace worn Teflon tape proactively ☐ Inspect power cable for visible wear ☐ Deep clean the full sealing area ☐ Review seal quality logs for any declining trend 📋 Quarterly ☐ Full equipment inspection ☐ Replace heating wire if showing any deterioration
☐ Test temperature calibration accuracy ☐ Contact manufacturer if performance has declined progressively 8. When to Contact a Technical Specialist The following situations warrant contacting your sealing machine manufacturer or a qualified technician. Avoid
disassembling the machine internally without professional guidance, as improper handling may cause additional damage or void the warranty. Contact a Technician When: Seal quality has not improved after replacing consumables Machine produces unusual sounds
or odors during operation Temperature control display is malfunctioning or unresponsive Heating wire replaced but heating remains uneven Machine is aging and overall performance has declined progressively Information to Prepare Before Contacting Machine model
number and purchase date Bag material type and thickness Current temperature setting Specific description of the seal quality symptom Frequency of the issue and when it first occurred Related Products If your current sealing machine is consistently underperforming
despite troubleshooting, it may be time to evaluate whether a different machine type better fits your bag material or production volume. Impulse Sealer PE bags, OPP bags, light packaging View Series Continuous Band Sealer High-volume production line sealing
View Series Vacuum Sealer Meat, seafood, food preservation View Series Medical Pouch Sealer Sterilization pouches, medical packaging View Series The following questions are compiled from Daily Sealing System's after-sales technical service experience across
food processing, agricultural packaging, electronics manufacturing, and industrial packaging clients since 2010. Frequently Asked Questions Q1: Why is my heat sealer not sealing properly? Poor seal quality is most commonly caused by one of five issues: incorrect
sealing temperature, incompatible bag material, worn heating wire or Teflon tape, contamination at the bag opening, or incorrect operator technique. Start by checking these five factors systematically — most seal quality problems can be resolved without professional
repair. Q2: Why does my seal line look wrinkled or uneven? A wrinkled or uneven seal line is most commonly caused by the bag opening not being pulled flat before sealing, or by Teflon tape that has worn and degraded. First, try flattening the bag opening completely
before applying the seal. If the issue persists, inspect the Teflon tape for visible wear or damage and replace it if necessary. Q3: Why is my seal line burnt or turning black? A burnt or blackened seal line indicates that the sealing temperature is set too
high, or that the bag material is not compatible with the machine. Reduce the temperature immediately and confirm the bag material is appropriate for the machine type. Aluminum foil bags and standard PE bags require very different sealing temperatures. Q4:
Why does my vacuum-sealed bag lose vacuum quickly after sealing? Vacuum bags that lose vacuum quickly typically indicate one of four issues: incompatible bag material (not using a vacuum channel or flat vacuum bag), insufficient seal width, contamination at
the bag opening, or a degraded heating wire producing an incomplete seal. Work through these four causes systematically before contacting a technician. Q5: How often does the heating wire need to be replaced? Heating wire has no fixed replacement interval
— it depends on usage frequency and bag material. Machines used for high-volume daily production or sealing thicker materials such as aluminum foil bags will wear through heating wire more quickly. When seal lines become uneven, develop gaps, or the wire shows
visible discoloration or brittleness, replace it promptly. Q6: Can poor seal quality damage product shelf life? Yes. A weak or incomplete seal allows moisture, oxygen, and environmental contamination to enter the package — directly reducing product shelf life
and increasing the risk of spoilage, flavor degradation, or contamination. For food products, even a small gap in the seal line can significantly shorten the period during which the product remains safe and market-ready. Maintaining consistent seal quality
is a direct food safety and product quality issue, not only a packaging efficiency concern. 📖 Further Reading Related articles on sealing machine selection, specifications, and performance: → How to Choose the Right Sealing Machine Based on Product Type →
How to Choose the Right Sealing Length and Sealing Width → Vacuum Sealer vs. Continuous Band Sealer: Which Should You Choose? → What Industries Use Vacuum Sealers? Applications and Buying Guide → When Should You Use a Continuous Band Sealer? About This Article
This article was prepared by the Daily Sealing System technical team. It is intended as a practical troubleshooting guide for packaging engineers, purchasing teams, food manufacturers, and industrial packaging users. Daily Sealing System Co., Ltd. is a Taiwan-based
sealing machine manufacturer with an in-house production facility. Our product range includes vacuum sealers, external vacuum sealers, chamber vacuum sealers, continuous band sealers, foot sealers, impulse sealers, medical pouch sealers, and customized sealing
equipment. The company holds ISO 9001:2015 certification. Certain products and related materials carry CE, FDA, EU No.10/2011, and BPA Free certifications. Patents are registered in Taiwan, the United States, Europe, Germany, Japan, and China. Content in this
article is based on Daily Sealing System's practical manufacturing experience and after-sales technical service since 2010, and is intended to support equipment troubleshooting and purchasing decisions by B2B buyers and packaging operations teams. Need Help
Identifying the Cause? Our technical team can help you determine whether your seal quality issue is related to: ✓ Machine settings and temperature calibration ✓ Bag material compatibility ✓ Consumable parts condition ✓ Equipment selection for your application
View All Sealing Machine Series Contact Our Technical Team // //
We use cookies to provide a better experience. By proceeding, you agree to our PRIVACY POLICY, including the use of cookies and other tracking technologies.ACCEPT
 2026/10/14Custom Printed Vacuum Bags for Bulk Orders: Materials, Sizes, Printing & OEM Buying GuideCustom Printed Vacuum Bags for Bulk Orders: Materials, Sizes, Printing & OEM Buying Guide Ordering custom printed vacuum bags in bulk is very different from buying a few sample pouches. For importers, distributors, private-label brands, food processors and contract packers, a single specification error can be repeated across thousands of bags — or an entire container. The bag has to fit your vacuum machine, protect the product, carry the right print for the destination market, and ship in a carton and pallet configuration that works commercially. This guide explains what bulk buyers should confirm before requesting a quotation, how to specify bag type, material, size, thickness and printing, why MOQ is only one of several numbers to compare, and how sample approval leads to bulk production and FCL or LCL shipment. Quick Answer: What Should a Bulk Buyer Confirm Before Ordering Custom Vacuum Bags? Before requesting a quotation, buyers should confirm the product being packed, vacuum machine type, bag structure, thickness, size, printing requirements, annual or order volume, destination market and required documentation. Product being packed: frozen, chilled or dry; bone-in or sharp edges; liquid or marinade content Vacuum machine type: nozzle-type, chamber or external (non-nozzle) Bag type and structure: smooth or embossed (channel); material layers Thickness: in micron or mil, and what the figure refers to Bag size: width, length, headspace and sealing allowance Printing requirements: artwork, colors, print area, barcode or date-coding area Order volume: quantity per size, per design and per year Destination market and documents: labeling and documentation requirements Do not evaluate the bag independently from the vacuum sealing system. A bag that looks right on paper can still fail on your machine. 1. Start with the Product and the Machine, Not the Artwork Printing is the most visible part of a custom vacuum bag, but it is rarely the part that decides whether the order succeeds. Experienced buyers settle the functional specification first and send artwork afterwards. Two questions come before everything else: What is being packed? Product form, weight, sharp edges or bones, moisture or liquid content, and whether it will be refrigerated, frozen or heat-treated all influence the bag structure and thickness you need. Which vacuum machine will seal it? The machine's air-evacuation method determines which bag type can be used. This is the first compatibility check in any bulk order. 2. Smooth vs. Embossed Vacuum Bags: Which One Fits Your Machine? For international buyers, this is the most important first check. Vacuum bags are commonly supplied as smooth (flat) pouches or embossed (channel) bags, and the two are not interchangeable on every machine. FeatureSmooth (flat) vacuum pouchesEmbossed (channel) vacuum bags How air is removed The machine design removes the air — for example through a nozzle, or by placing the pouch in a vacuum chamber Embossed channels on the film create air paths, so an external machine can draw air out through the bag opening Commonly used with Nozzle-type and chamber vacuum sealers External (non-nozzle) vacuum sealers Buyer should confirm Pouch width against sealing length or chamber size; sealing conditions for the bag structure Bag opening position and effective sealing length in the machine manual; channel pattern suits the machine These pairings are common patterns, not guarantees. Machine designs vary, so confirm the bag type against the specification of your exact machine — and test before bulk production. Explore the bag ranges: Channel Vacuum Bags and Vacuum Sealer Bags (smooth). Machine types: nozzle type, non-nozzle type and chamber vacuum sealers. 3. How to Select Material Structure for Commercial Vacuum Packaging Commercial vacuum bags are usually multilayer films. PA (nylon)/PE laminates are one common structure, but do not assume that every bag with the same material name performs the same way. Barrier properties, puncture resistance and suitability for refrigerated or frozen use depend on the exact layers, resin grades and thickness — and should be confirmed from the supplier's specification. What to specifyWhy it matters Material structure (for example PA/PE or other multilayer) Affects barrier performance, flexibility and heat-seal behavior Heat-seal layer Determines sealing conditions and whether the bag suits your sealer Barrier requirement Depends on product sensitivity to oxygen and moisture and your target storage conditions Puncture resistance Important for bone-in products, shellfish, hardware or other sharp items Temperature application Refrigerated, frozen or heat-treated use should be confirmed against the actual bag specification Food-contact documentation Request the documents that apply to the exact bag and the destination market 4. How Should Importers Specify Bag Size and Thickness? Bag size is not simply product size. Size must also account for air evacuation, the sealing area and the machine's limits. Supply the following so the supplier can quote the right bag the first time: Bag width and length Inner dimensions, stated clearly as internal or external. Product dimensions Length, width and height of the packed product, including the thickest point. Headspace Enough open space above the product for air evacuation and a clean seal area. Sealing allowance The opening must not exceed the sealer's effective sealing length. Thickness In micron or mil, and whether it is total film thickness. Tolerance Agree acceptable dimensional and thickness tolerance in advance. Reading thickness: suppliers may quote micron (µm) or mil. One mil equals 25.4 µm, so 3 mil is about 76 µm and 4 mil is about 102 µm. Always confirm whether the number refers to total thickness or to a single layer, so quotes from different suppliers can be compared fairly. Bag format also matters. Daily Sealing supplies smooth pre-made vacuum sealer bags for nozzle-type and chamber vacuum sealers, while vacuum roll bags are channel-type bags designed for non-nozzle vacuum sealers. Confirm both the bag format and the machine type before ordering — and decide early whether you need pre-made pouches or roll stock that your team cuts to length. For help matching bag opening width to machine capacity, see: How to Choose the Right Sealing Length and Sealing Width. 5. Custom Printing for Private Label and Retail Packaging: What to Send the Supplier This section is not about how printing works — it is about what information a supplier needs from you to quote and produce printed vacuum bags correctly. ProvideWhy the supplier needs it Artwork file and logo Basis for the print layout and any tooling Print area Defines usable space and keeps print clear of the seal area Colors Affects process choice, cost and setup Barcode or QR code Needs a readable position away from seals, folds and edges Batch or date-coding area A blank, printable zone reserved for lot codes added later Mandatory labeling Legal text that must appear for your product and market Destination-market requirements Language, symbols and documentation vary by country Two cautions. First, keep key text, logos and codes away from the heat-seal area so they are not obscured or distorted after sealing; whether print affects sealing performance depends on the laminate structure and where the print layer sits, so confirm this with the supplier. Second, mandatory labeling for food or export products depends on the product and the destination market — it must be confirmed by the buyer and is not something a print layout can decide. 6. MOQ Is Not the Only Number Bulk Buyers Should Compare Minimum order quantity depends on bag type, size, material, thickness and printing, so there is no universal figure. For a container-level purchase, buyers should confirm the following items, not MOQ alone: Confirm with the supplierWhy it affects your cost and risk Order quantity per size Several sizes may be treated as separate production runs Quantity per artwork or design version Each print version can carry its own minimum Sample or pre-production sample Lets you test on your machine before committing Tooling or printing-plate cost, if applicable A one-time cost that changes the real unit price on smaller runs Production lead time Drives your shipping schedule and stock planning Carton packing Quantity per carton and carton marking affect handling at your end Pallet requirement Affects loading efficiency and freight cost Shipment volume / CBM Helps buyers plan LCL vs. FCL shipment and compare carton, pallet and loading efficiency Repeat-order consistency Print, dimensions and material should match from batch to batch Every item above is something for the buyer to confirm during quotation. Actual minimums, lead times and costs are agreed per specification and are not fixed in advance. 7. From Sample Approval to Bulk or FCL Shipment For volume orders, a practical procurement workflow is to confirm the specification and sample before moving into bulk production and export shipment. The exact sequence and timing depend on the agreed specification and supplier arrangement, so treat the stages below as a checklist rather than a promised schedule. 01 Specification confirmation Bag type, structure, size, thickness and machine 02 Artwork confirmation Print area, colors, codes and mandatory labeling 03 Sample / pre-production check Review dimensions, print and structure 04 Machine compatibility test Run the sample on your actual vacuum sealer 05 Production approval Written sign-off on the confirmed specification 06 Bulk production Production against the approved specification and reference sample, where applicable 07 Packing Carton marking, pallet configuration and loading plan 08 Export shipment Shipping documents and delivery arrangement 8. What Should Be Included in an RFQ for Custom Vacuum Bags? A complete request for quotation shortens the back-and-forth and reduces the risk of a wrong specification. Use the template below and replace the bracketed examples with your own information. If a value is not yet known, write "to be confirmed" rather than guessing. Product: [for example, frozen meat portions] Bag type: [smooth pouch / embossed channel bag / roll bag] Bag size: [width × length; opening position] Material structure and thickness: [for example, PA/PE; thickness in µm or mil] Vacuum machine: [brand and model; chamber / nozzle-type / external non-nozzle] Printing: [logo, product information, number of colors, print area] Barcode / QR / date-coding area: [required or not; preferred position] Estimated quantity: [per size / per design / annual] Destination market: [for example, USA / EU / Middle East] Required documents: [for example, food-contact documentation, material specification] Packing requirements: [carton marking, pallet, container loading] Shipping information: [destination port, preferred Incoterm if known, estimated FCL / LCL requirement] Target timing: [required arrival window] 9. Why Machine Compatibility Matters Before Bulk Production Many packaging-material suppliers sell only the bag. Daily Sealing System designs and manufactures vacuum sealing machines and also supplies vacuum sealer bags, with technical support for both. For a bulk buyer this means the bag and the machine can be evaluated as one system — which is exactly how they perform in production. Do not evaluate the bag independently from the vacuum sealing system. A change in bag structure, thickness or supplier can change how the bag evacuates, seals and holds vacuum. Compatibility check before approving bulk production: Run the sample bags on your actual vacuum sealer with the real product Confirm air evacuation works properly with the chosen bag type Check seal appearance and continuity after the machine cycle Observe vacuum retention over an internal QC period you define Re-confirm the sealing settings applicable to your machine — such as sealing time, temperature where adjustable, and cooling time — when the bag structure or thickness changes Record the confirmed settings for repeat production Related technical guides: How to Set Sealing Time for Impulse, Constant Heat & Band Sealers, Heat Sealing Temperature Guide for Different Packaging Materials, How to Check Heat Seal Integrity: Quality & Leak Inspection Guide. If a new bag produces weak seals, see Why Is My Sealing Machine Not Sealing Properly? Related Products Channel Vacuum Bags Embossed channel bags and roll bags for non-nozzle vacuum sealers View Series Vacuum Sealer Bags Smooth pre-made pouches for nozzle-type and chamber sealers View Series Chamber Vacuum Sealers For smooth pouches and moist or liquid products View Series Non-nozzle Vacuum Sealers External machines used with channel bags View Series The following answers are based on Daily Sealing System's sealing-machine manufacturing, vacuum-bag compatibility and after-sales technical support experience since 2010. Frequently Asked Questions Q1: Can vacuum bags be custom printed for OEM or private-label orders? Custom printed vacuum bags are commonly ordered for OEM and private-label use. Whether a specific bag type, size and print layout can be produced depends on the material structure, printing process and order conditions, so confirm the details during quotation before committing to a bulk order. Q2: Can both smooth and embossed vacuum bags be printed? This depends on the actual bag structure and manufacturing process. Smooth and embossed bags should not be assumed to have the same printing conditions, so confirm print feasibility for the specific bag type with the supplier. Q3: What is the minimum order quantity for custom vacuum bags? There is no universal figure. MOQ is influenced by bag type, size, material, thickness, printing method, number of colors, any tooling or plate requirement and production conditions. It should be confirmed by quotation, together with quantity per size, quantity per design and lead time. Q4: What information should be included in an RFQ for custom vacuum bags? Include the product, bag type, bag size, material structure and thickness, vacuum machine type, printing requirements, barcode or date-coding needs, estimated quantity, destination market, required documents and packing requirements. Use "to be confirmed" for anything not yet known rather than guessing. Q5: Should I test the bags on my vacuum machine before ordering in bulk? Yes. Test sample bags on your actual machine with the real product to confirm air evacuation, seal quality and vacuum retention, and re-confirm the sealing settings applicable to your machine (such as sealing time, temperature where adjustable, and cooling time) if the bag structure, thickness or supplier differs from your previous bags. Record the confirmed settings for repeat production. Q6: Are all printed vacuum bags suitable for freezing, boiling or microwave use? No. Frozen storage, boiling, hot-fill and microwave use are separate application requirements. Each must be supported by the exact bag structure and supplier documentation. Suitability for one condition does not automatically mean the bag is suitable for another. Q7: What documents should importers request for food-contact vacuum bags? Request the material specification and the food-contact documentation that applies to the exact bag and the destination market. The documents required differ by country and product, so confirm what is available and what your market requires before placing a bulk order. 📖 Further Reading → Vacuum Sealer vs. Continuous Band Sealer: Key Differences, Applications, and Buying Guide → How to Set Sealing Time for Impulse, Constant Heat & Band Sealers → Heat Sealing Temperature Guide for Different Packaging Materials → How to Check Heat Seal Integrity: Quality & Leak Inspection Guide → Why Is My Sealing Machine Not Sealing Properly? Common Causes and How to Fix Them → How to Choose the Right Sealing Length and Sealing Width About This Article This article was prepared by the Daily Sealing System technical team for importers, distributors, private-label brands, food processors, contract packers and procurement teams sourcing vacuum packaging. Daily Sealing System Co., Ltd. is a Taiwan-based manufacturer of sealing equipment and vacuum sealer bags, with an in-house production facility and experience supporting international B2B buyers. Its product range includes vacuum sealers, smooth vacuum pouches, channel vacuum bags, impulse sealers, constant heat sealers, continuous band sealers, medical pouch sealers and customized sealing equipment, together with OEM / ODM support and after-sales technical service. The company holds ISO 9001:2015 certification and has patents related to sealing equipment in Taiwan, the United States, Europe, Germany, Japan and China. See the certificates page for details. This guide is based on Daily Sealing System's sealing-machine manufacturing, vacuum-bag compatibility and after-sales technical support experience since 2010. This article is general buying guidance. Available bag structures, sizes, printing options, minimum order quantities, lead times and documentation depend on the specific specification and a formal quotation. Food-contact, freezing, heat-treatment and destination-market requirements should be confirmed against the actual bag specification and supplier documents. Planning a Bulk Order of Custom Printed Vacuum Bags? Send us your product, vacuum machine model, bag type and size, material and thickness requirements, printing needs, estimated quantity and destination market. Our technical team can help you check bag and machine compatibility and plan the specification before you request a quotation. View Vacuum Sealer Bags Contact Our Technical Team // //MORE
 2026/9/4How to Set Sealing Time for Impulse, Constant Heat & Band SealersHow to Set Sealing Time for Impulse, Constant Heat and Continuous Band Sealers How long should a sealing machine seal a bag? There is no single sealing time that works for every packaging material or sealing machine. The correct heat-sealing process depends on several variables, including the sealing method, pouch structure, material thickness, seal width, pressure, temperature and production speed. This is especially important for B2B packaging operations because impulse sealers, constant heat sealers, continuous band sealers and vacuum sealers do not control heat in the same way. For production teams, the goal should not be to find a universal number of seconds — the better approach is to establish a tested and documented sealing condition for the specific machine, packaging material and production requirement. Quick Answer: How Long Should Sealing Time Be? There is no universal sealing time. Impulse sealers: commonly control heating time or output rather than actual sealing temperature Constant heat sealers: require the correct combination of temperature, contact time and pressure Continuous band sealers: temperature and conveyor speed must be evaluated together, since line speed changes heat exposure Vacuum sealers: sealing time or temperature depends on machine design, pouch structure and sealing requirements When material changes: re-test the sealing conditions whenever pouch structure, thickness, supplier or machine configuration changes For industrial production, sealing time should always be treated as one process parameter rather than a standalone setting. 1. Why Is There No Universal Sealing Time? Heat sealing works by applying sufficient thermal energy to the pouch sealant layer while maintaining the required contact pressure for an appropriate period. This means that two machines sealing what appears to be the same pouch may still require different settings. Sealing Method Impulse, constant heat and continuous sealing systems transfer heat differently. An impulse sealer heats only during the sealing cycle, while a constant heat sealer maintains a heated sealing surface. A continuous band sealer moves the pouch through heating and cooling sections. Packaging Material Structure PE, PA/PE, PET/PE and other laminated films use different sealant layers and material structures. The outer material name alone does not determine the correct sealing time. Material Thickness Thickness affects heat transfer, but a thicker pouch does not automatically mean operators should simply increase temperature or extend heating time. Material structure, sealant layer and machine capability must also be considered. Seal Width and Pressure Seal width, contact area and pressure can affect how thermal energy is transferred across the sealing zone. A change in sealing width or pressure may therefore require process settings to be re-tested. Related guide: How to Choose the Right Sealing Length and Sealing Width 2. Impulse Sealers: Start with Heating Time or Output Hand impulse sealers, many foot impulse sealers and other impulse-type machines heat the sealing element only during the sealing cycle. For this reason, many impulse sealers do not directly control the actual surface temperature. Instead, the operator commonly adjusts heating time, timer level or output. Recommended adjustment process: Confirm the pouch structure and thickness Start from the machine manual or an existing tested setting Test the actual packaging material used in production Begin with a relatively low setting and increase gradually Change only one major parameter at a time Allow the seal area to cool appropriately before evaluating the result Record the confirmed machine and material settings Some impulse sealing systems also require a short pressure or cooling period after heating stops. Moving the pouch too early can affect a newly formed seal. Avoid this common mistake: if a pouch does not seal properly, do not immediately turn the timer to the maximum setting. Excessive heat input may cause pouch shrinkage, melting or burn-through, excessive seal distortion, material sticking, or unnecessary wear on heating elements or PTFE covers. The objective is not to apply maximum heat — it is to apply enough controlled heat to create a reliable seal without damaging the packaging material. 3. Constant Heat Sealers: Sealing Time Is Only One Part of the Process Constant heat sealers maintain the sealing jaws or heating surface at a controlled temperature. For these machines, sealing performance depends on the combined effect of sealing temperature, contact or dwell time, sealing pressure, pouch structure and material thickness. If the temperature is too low, simply holding the pouch longer may not produce a reliable seal. If temperature and dwell time are both excessive, the pouch may distort, thin out or melt through. For constant heat sealing, a better process is: pouch structure → suitable temperature range → dwell time → pressure → seal-quality verification — rather than asking only "how many seconds should I seal this bag?" For material-specific temperature guidance, see: Heat Sealing Temperature Guide for Different Packaging Materials. 4. Continuous Band Sealers: Conveyor Speed Changes Heat Exposure A continuous band sealer moves the pouch continuously through a heating section. For this reason, conveyor speed affects how long the packaging material remains exposed to heat. Production ChangePossible Effect Higher conveyor speed Shorter exposure time in the heating zone; existing temperature settings may provide insufficient heat Lower conveyor speed Longer heat exposure; excessive temperature may distort or overheat the pouch Different pouch thickness or laminate Temperature and conveyor speed should be re-tested together Temperature and conveyor speed should therefore be treated as linked process variables. A production team that increases line speed without rechecking the sealing condition may see previously stable seals become weak or inconsistent. Similarly, slowing the line while maintaining an unnecessarily high temperature may create excessive heat exposure. For higher-volume packaging operations, both seal consistency and production throughput should be considered when validating the settings. Related guide: When Should You Use a Continuous Band Sealer? 5. How Should Sealing Time Be Set on a Vacuum Sealer? A vacuum sealer normally performs at least two different process stages: air evacuation and heat sealing. The vacuum cycle and the sealing cycle should therefore be evaluated separately. Depending on machine design, the operator may adjust sealing time, temperature or another heat-control setting. Whenever the vacuum pouch supplier, material structure or thickness changes, the sealing condition should be re-tested — even if the vacuum extraction performance remains unchanged. If Sealing Heat Is Insufficient Incomplete seal formation Weak seal strength Gradual loss of vacuum Leakage after handling or storage If Heat Input Is Excessive Seal-area distortion Pouch shrinkage Melt-through Weakening of the seal area Always confirm the specific vacuum sealer design and pouch structure before establishing production settings. 6. How Can You Tell If Sealing Time Is Too Short or Too Long? The seal result provides useful clues, but one symptom does not always point to only one cause. Seal ConditionPossible Direction to Check Seal opens easily or contains unfused areas Heat input may be insufficient; also check material compatibility, pressure and contamination Seal line shrinks or wrinkles Possible excessive heat or unsuitable settings Pouch melts through or burns Heat input may be excessive The same section repeatedly fails to seal Check heating element, PTFE cover, pressure pad or sealing-area alignment rather than only increasing time Seal quality changes after switching pouch supplier Re-test material structure, thickness and sealing parameters If increasing sealing time does not improve the result, do not continue increasing it indefinitely. The problem may instead involve an incompatible packaging material, insufficient or excessive temperature, uneven pressure, contamination in the sealing area, a worn heating element, damaged PTFE material, or other machine-related issues. Related guide: Heat Sealer Not Sealing Properly? 5 Common Causes and How to Fix Them 7. How to Validate Sealing Time After Changing Packaging Material For manufacturers, food processors, contract packers and other B2B users, a pouch change should be treated as a process change. This includes changes in packaging supplier, resin or laminate structure, material thickness, bag dimensions, sealing machine, and production speed. 01 Confirm the Packaging Specification Record the material structure, total thickness and sealant layer when available 02 Confirm the Sealing Machine Type Impulse, constant heat, continuous band or vacuum sealer 03 Establish a Starting Setting Use manufacturer instructions or a previously confirmed condition 04 Keep Other Variables Stable Change only one major parameter at a time 05 Adjust Gradually Make small changes and compare seal results 06 Allow the Seal to Stabilize Allow sufficient cooling before judging the seal 07 Record the Confirmed Production Setting Document the machine, material and operating parameters 8. For Production Lines, Do Not Record Only "2 Seconds" or "3 Seconds" For repeat B2B production, a single sealing-time number is usually not enough. If the packaging material or equipment changes later, a record such as "seal for 2 seconds" provides very little information about why the process originally worked. A more useful production record should include: Sealing machine model Packaging material structure Pouch thickness Sealing time or output setting Sealing temperature, when applicable Conveyor speed for continuous band sealers Seal width Product type Pouch opening condition Seal inspection result Packaging-material supplier or batch, when relevant This makes it easier to reproduce confirmed conditions and troubleshoot future process changes. 9. B2B Sealing-Process Checklist: What Information Should Buyers Prepare? When contacting a sealing-machine manufacturer or packaging equipment supplier, providing complete process information can help identify the correct machine configuration and starting settings more efficiently. Prepare: Current sealing machine model Pouch material structure Pouch thickness Bag opening width Required sealing length Required seal width Product being packaged Dry, oily, powder or liquid product condition Current sealing time or timer setting Current temperature, when applicable Conveyor speed, when applicable Daily production volume Required production speed Current seal-quality problem Target market or special packaging requirement For OEM / ODM or new packaging projects, this information is also useful when determining whether the existing sealing method is suitable for the required output and material. The following questions are compiled from Daily Sealing System's manufacturing, packaging-material testing and after-sales technical support experience since 2010. Frequently Asked Questions Q1: How many seconds should a heat sealer be set for? There is no universal sealing time. The correct setting depends on machine type, pouch structure, thickness, seal width, pressure and other process conditions. Always validate the setting using the actual production material. Q2: Does a thicker bag always require a longer sealing time? No. Thickness can affect heat transfer, but material structure, sealant layer, temperature, machine output and pressure also influence the result. Thickness alone should not determine sealing time. Q3: Should I adjust temperature or time on an impulse sealer? Many impulse sealers primarily control heating time or output rather than actual sealing temperature. Machine designs vary, so always confirm the controls specified for the model. Q4: Why does my continuous band sealer produce weak seals after increasing conveyor speed? Increasing conveyor speed reduces the time the pouch remains in the heating zone. If other parameters remain unchanged, the material may receive insufficient heat. Re-test temperature and conveyor speed together. Q5: Why does the bag still not seal even after increasing sealing time? The problem may not be insufficient time. Check packaging-material compatibility, sealing temperature or output, pressure, contamination, heating elements and PTFE components before continuing to increase the setting. Q6: Do sealing settings need to be re-tested when changing pouch suppliers? Yes. Even when the material name and nominal thickness appear similar, the sealant layer, laminate structure and production specifications may differ. Re-test and document the sealing condition before full production. 📖 Further Reading For sealing-machine buyers, packaging engineers and production teams: → Heat Sealing Temperature Guide for PE, OPP & Foil Bags → Heat Sealer Not Sealing Properly? Common Causes and How to Fix Them → How to Choose the Right Sealing Length and Sealing Width → When Should You Use a Continuous Band Sealer? → Sealing Machine Maintenance: 7 Ways to Extend Service Life About This Article This article was prepared by the Daily Sealing System technical team for purchasing teams, packaging engineers, production managers, contract packers and industrial packaging users. Daily Sealing System Co., Ltd. is a Taiwan-based sealing machine manufacturer with an in-house production facility. The company provides impulse sealers, foot sealers, constant heat sealers, continuous band sealers, vacuum sealers, medical pouch sealers and customized sealing equipment, together with OEM / ODM support and after-sales technical service. This guide is based on Daily Sealing System's manufacturing, packaging-material testing and after-sales technical support experience since 2010. Actual sealing time, temperature, pressure and conveyor-speed settings vary by machine model, packaging material and production conditions. Production parameters should always be tested and confirmed using the actual machine and pouch specification. Need Help Determining the Right Sealing Settings for Your Packaging Material? Send us your machine model, pouch structure, pouch thickness, bag dimensions, product type, current sealing settings, daily production requirement and current seal result. Our technical team can help you evaluate the appropriate sealing-machine configuration and starting process settings for your packaging application. View Sealing Machines Contact Our Technical Team // //MORE
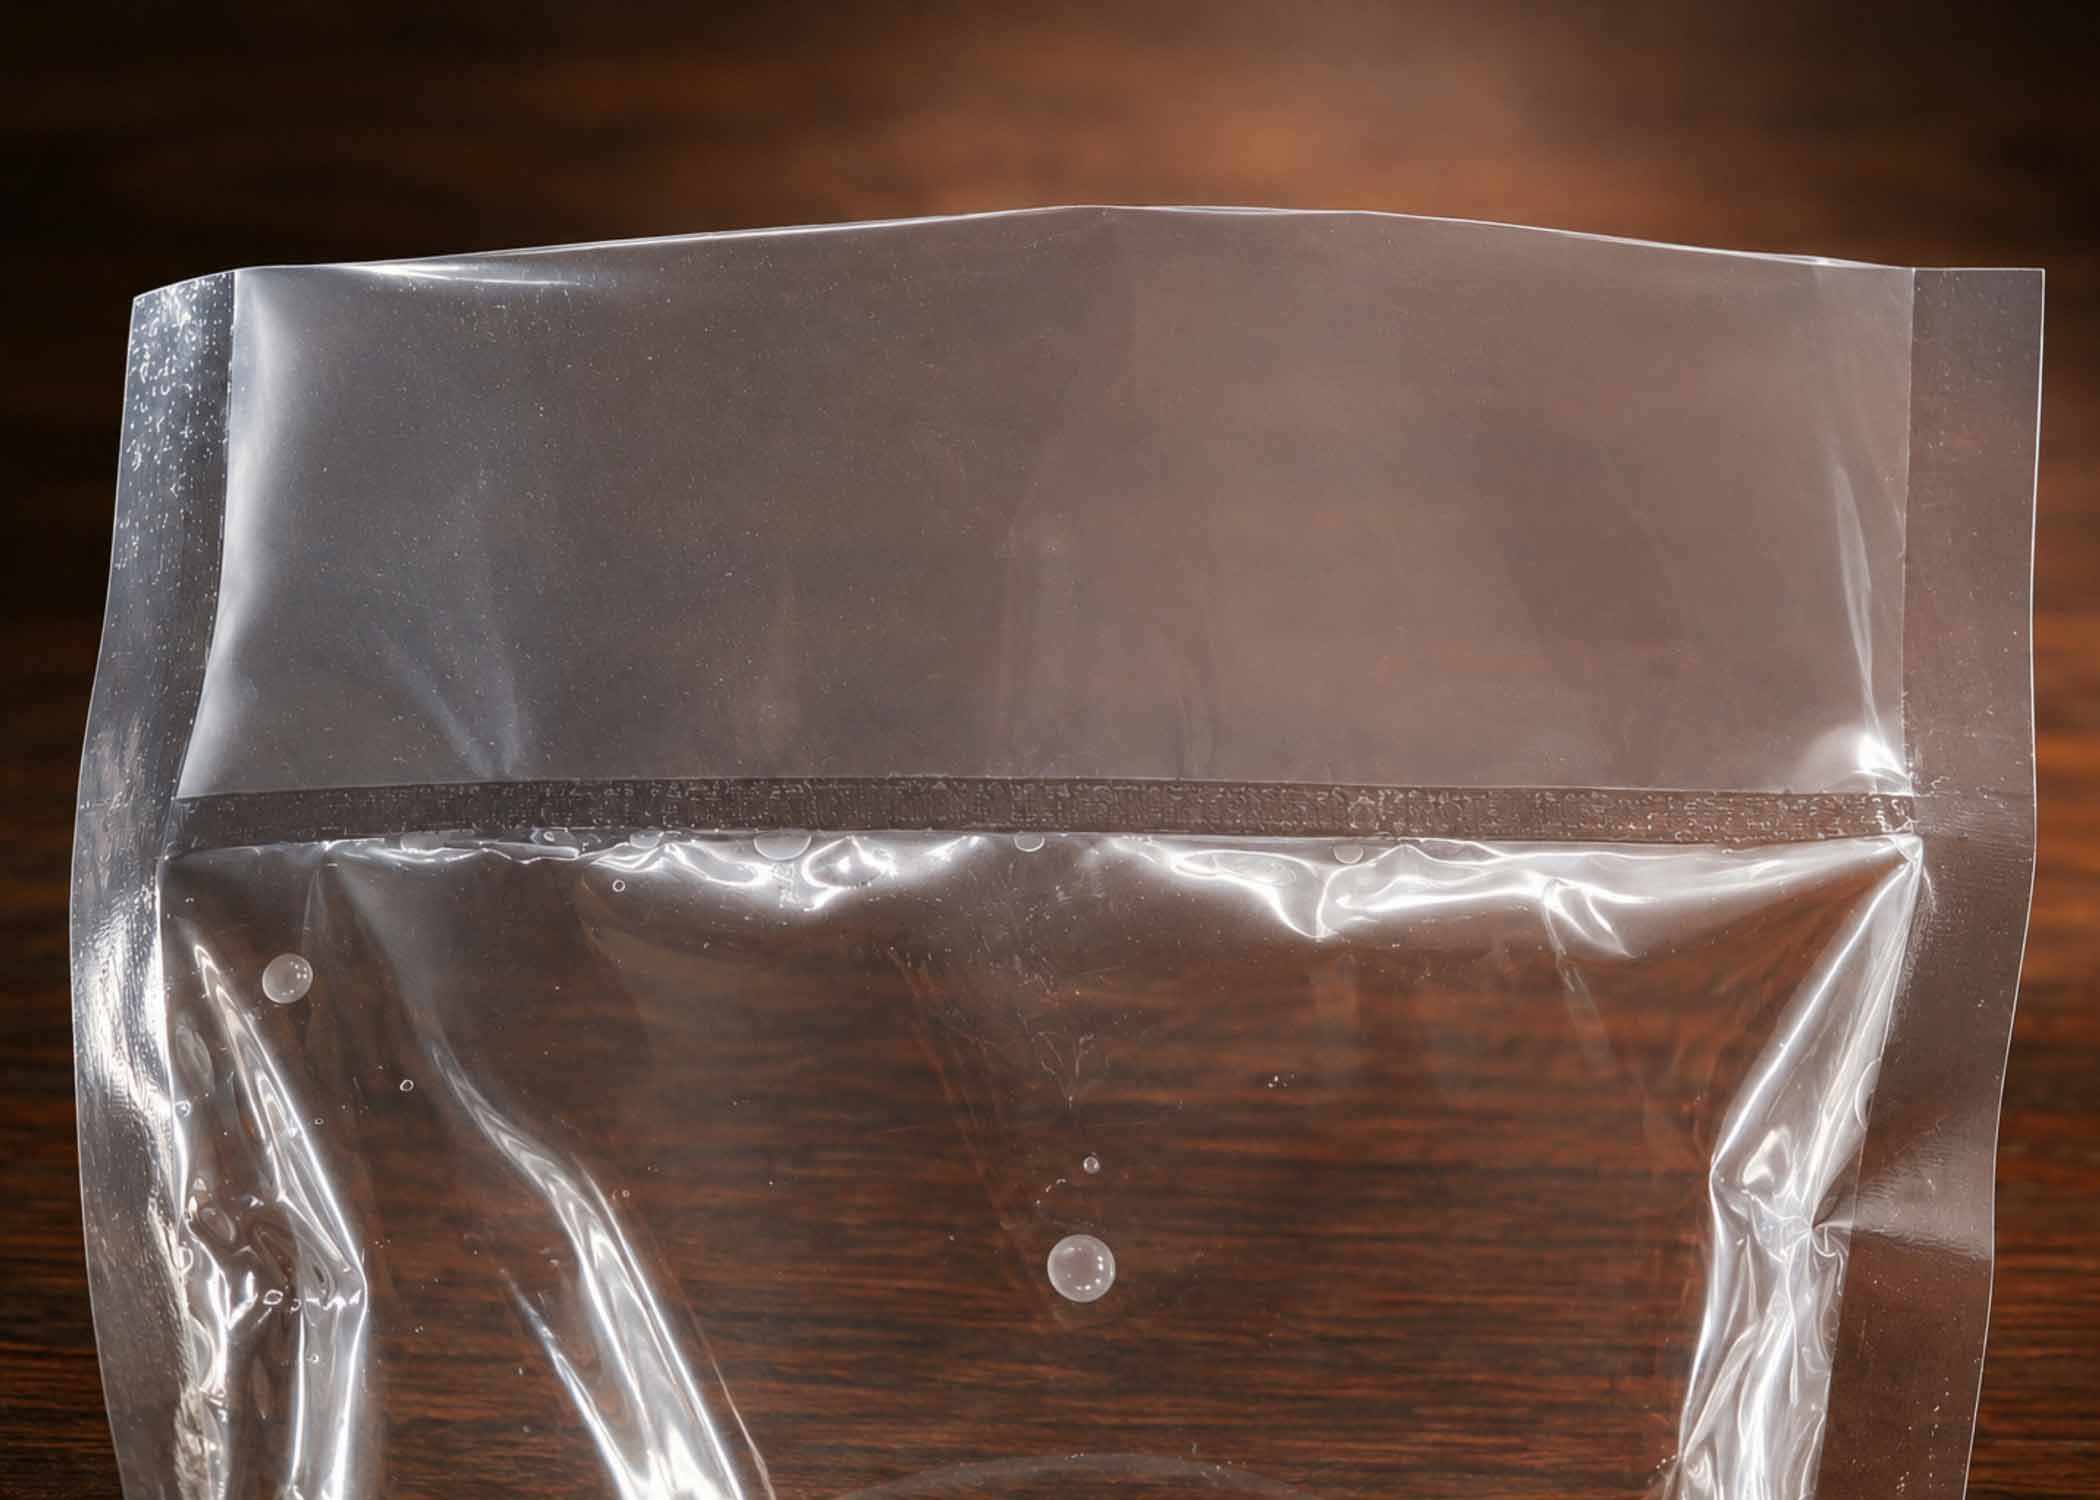 2026/9/4How to Check Heat Seal Integrity: Quality & Leak Inspection GuideHow to Check Heat Seal Integrity: Seal Quality & Leak Inspection Guide A pouch that looks closed is not necessarily properly sealed. A seal can appear complete while still containing wrinkles, unfused sections, contamination, pinholes, weak bonding or small leakage paths. In some cases, the problem does not become visible until the package is handled, transported or stored for a period of time. For B2B packaging operations, checking seal quality should therefore go beyond asking whether the two sides of the pouch are attached. Production and quality-control teams should evaluate seal-line continuity, seal appearance, post-cooling seal condition, leakage or vacuum loss, pouch and pre-made seal integrity, production consistency, and applicable customer or industry quality requirements. The inspection method should match the packaging material, product and required level of quality assurance. Quick Answer: How Do You Check Whether a Heat Seal Is Good? A practical first-level seal inspection can follow these steps: Inspect the seal line — it should be continuous and free from obvious wrinkles, burn-through, holes or unfused areas Check the pouch opening — oil, water, powder or product particles should not be trapped in the sealing area Allow the seal to cool — then perform an appropriate preliminary seal check for easy peeling or recurring weak areas Check for leakage or vacuum loss — inspect the seal, pouch body and original side or bottom seals For production use, establish a QC procedure — do not rely on the appearance of one sample as proof that the process is stable A visual or manual check is useful for preliminary inspection, but it does not replace formal seal-strength or package-integrity testing when such testing is required. 1. Start with a Visual Inspection of the Seal Line Visual inspection is usually the fastest first step. A properly formed heat seal should generally appear continuous and consistent, without obvious interruptions or damage. Is the Seal Line Continuous? Check the full sealing length for gaps, unfused sections, fixed-position defects or significant variation in appearance. If the same position repeatedly fails to seal, the issue may relate to the heating element, PTFE material, pressure pad or sealing-area alignment rather than only the process setting. Are There Wrinkles? Wrinkles across the seal area can create small leakage channels. This is especially important when sealing gusseted pouches, multi-layer sections, uneven bag openings, or pouches that were not flattened before sealing. Is There Evidence of Excessive Heat? Check for discoloration, severe shrinkage, material thinning, melt-through or burn marks. These conditions may indicate excessive heat input or a sealing condition that does not match the pouch structure. Is the Seal Area Contaminated? Oil, moisture, powder, food particles or other product residue can interfere with seal formation. For products with oily, wet or powdery contents, maintaining a clean sealing area is especially important. Related guide: Heat Sealer Not Sealing Properly? 5 Common Causes and How to Fix Them 2. Allow the Seal to Cool Before Performing a Preliminary Seal Check Heat-sealed material may still be soft immediately after the heating cycle. For this reason, seal quality should not always be judged the instant the pouch leaves the sealing area. Depending on machine design, the process may include heating time, pressure or dwell time, cooling time, and continued pressure during cooling. After the seal has cooled appropriately, a preliminary manual check can help identify obvious weak bonding. For example, if the seal opens under very light handling, repeatedly peels at the same position, or contains clearly unfused areas, the sealing condition should be reviewed. However, this type of manual check is only a shop-floor screening method. It should not be presented as a standardized seal-strength test. For products subject to customer specifications, regulated packaging requirements or formal quality systems, use the required measurement or verification method. 3. How Do You Check a Vacuum Package for Leakage? A vacuum package can appear normal immediately after sealing and later lose its vacuum. When this happens, inspect several possible leakage locations. Inspection AreaWhat to Check Heat seal line Wrinkles, contamination, unfused sections or interrupted sealing Pouch body Pinholes, punctures, sharp-product damage or handling damage Original side / bottom seals Leakage from pre-made pouch seams Packaging material Whether the pouch structure and barrier properties are suitable for the application Seal area Whether heat, pressure and time were sufficient for the material If the vacuum sealer cannot remove air from the beginning, the issue may involve pouch compatibility, air evacuation or the vacuum system rather than seal integrity. This is a different troubleshooting issue from a package that initially seals correctly and later loses vacuum. Important: Package Expansion Does Not Always Mean Seal Leakage. If a vacuum package gradually expands after sealing, leakage is one possible cause, but it should not automatically be assumed to be the only cause. Depending on the product and storage conditions, package appearance may also change because of factors such as product gas release or temperature changes. For this reason, investigate seal line → pouch body → original pouch seams → packaging material → product condition before concluding that the sealing machine is defective. 4. Can You Leave a Package for a Period of Time to Check for Leaks? Yes, a defined observation period can be used as an internal screening method. For example, a production team may keep vacuum-sealed samples and monitor whether they lose vacuum, rebound or expand, develop visible leakage, or show seal deterioration. However, the observation period should be defined by the company's product and QC requirements. There is no universal observation time that automatically proves package integrity for every application. For example, "no vacuum loss after 24 hours" may be useful as an internal screening criterion for a particular company or product, but 24 hours is not a universal industry standard for all vacuum packaging. 5. Formal Seal-Quality Verification Requires More Than Visual Inspection For production packaging, customer acceptance, food packaging, medical packaging or applications with defined quality requirements, visual inspection alone may not be sufficient. Depending on the product and quality specification, a company may need to evaluate seal strength or peel strength, package integrity or leakage, vacuum retention, package condition after transport or handling, and other test methods required by the customer, market or application. The appropriate method and acceptance criteria depend on pouch structure, packaging application, product risk, target market, customer specifications, and applicable internal or external quality requirements. Important scope note: The visual inspection, preliminary manual seal check and observation methods described in this guide are intended for general industrial packaging screening and troubleshooting. They do not replace any formal packaging validation, regulated test method or customer acceptance standard required for a specific product or industry. 6. Establish a Seal-Quality Sampling Record for Production Once a sealing process enters repeat production, "the machine is running normally" should not be the only quality criterion. Seal consistency can change because of packaging-material batch variation, material supplier changes, temperature changes, production speed changes, machine wear, heating-element condition, operator handling, contamination, or process-setting changes. A practical production QC record can include: Sealing machine model Pouch material structure Pouch thickness Pouch supplier or batch Sealing time Sealing temperature Conveyor speed, when applicable Seal width Visual inspection result Preliminary seal check result Vacuum-loss observation, when applicable Defect samples Adjustment history These records help production teams trace changes when seal quality starts to decline. They also make repeat production more consistent because the process is documented instead of relying only on operator memory. 7. What Should You Do When Seal Quality Fails Inspection? Once a seal-quality problem is identified, the next step should depend on the symptom. Problem FoundRecommended Direction Weak seal / easy peeling Check material, sealing temperature, time and pressure Wrinkled or burnt seal Review heat input and pouch compatibility Uncertain sealing time Re-test and document the sealing-time setting Same location repeatedly fails Inspect heating element, PTFE material, pressure area and alignment Vacuum package gradually loses vacuum Inspect seal line, pouch body and original pouch seams Problem continues after settings are corrected Inspect machine components or contact technical support For sealing-time adjustment, refer to: How to Set Sealing Time for Impulse, Constant Heat and Continuous Band Sealers For material-specific temperature guidance: Heat Sealing Temperature Guide for Different Packaging Materials For troubleshooting: Heat Sealer Not Sealing Properly? 5 Common Causes and How to Fix Them 8. B2B Seal-Quality Checklist: What Information Should You Prepare for Technical Support? When discussing a seal-quality problem with a sealing-machine manufacturer or packaging equipment supplier, providing complete application and process information can help the technical team identify whether the issue is related to the packaging material, process settings or equipment condition. Sealing machine model Sealing method: impulse, constant heat, band or vacuum Pouch structure Pouch thickness Pouch dimensions Required seal width Product being packaged Dry, oily, wet, powder or liquid condition Sealing temperature Sealing time or timer setting Conveyor speed, when applicable Current seal appearance Whether the seal opens easily Whether the package loses vacuum Whether the defect always occurs in the same position Daily production volume Applicable customer or quality requirements For OEM / ODM or new packaging projects, this information can also help determine whether the existing sealing method and machine configuration are suitable for the required material and production conditions. The following answers are based on Daily Sealing System's sealing-machine manufacturing, packaging-material application testing and after-sales technical support experience since 2010. Frequently Asked Questions Q1: How can I tell if a heat seal is properly sealed? Start with a visual inspection. The seal line should be continuous and free from obvious wrinkles, burn-through, contamination and unfused sections. After appropriate cooling, perform a preliminary seal check and use any additional strength or integrity verification required for the packaging application. Q2: Is a seal good if the pouch looks completely closed? Not necessarily. A pouch can appear closed while still containing weak bonding, wrinkles, contamination or small leakage paths. Seal appearance is only the first level of inspection. Q3: Is it normal if a heat seal opens easily after cooling? If the seal opens very easily after appropriate cooling, the material, sealing time, temperature, pressure or equipment condition should be reviewed. Formal acceptance criteria should still follow the applicable product or customer quality requirement. Q4: Does a vacuum package that expands later always mean the seal is leaking? No. Leakage from the heat seal, pouch body or original pouch seams is one possible cause, but product gas release or storage-temperature changes may also affect package appearance. Inspect both the package and the product condition before drawing a conclusion. Q5: If a vacuum bag does not leak after 24 hours, is it automatically acceptable? No. A 24-hour observation can be used as an internal screening condition, but it is not a universal acceptance standard for all products or vacuum packaging applications. Q6: Does every package need to be tested during production? Not necessarily. Whether a company uses 100% inspection or sampling depends on product risk, internal quality procedures, customer requirements and the production process. The inspection frequency and acceptance criteria should be defined by the applicable quality system. Q7: What is the difference between seal inspection and seal testing? Seal inspection usually includes preliminary checks such as visual condition, continuity, contamination and obvious bonding defects. Formal seal testing may involve defined strength, integrity or leakage methods with specified acceptance criteria. The required level depends on the packaging application. 📖 Further Reading → How to Set Sealing Time for Impulse, Constant Heat and Continuous Band Sealers → Heat Sealing Temperature Guide for Different Packaging Materials → Heat Sealer Not Sealing Properly? 5 Common Causes and How to Fix Them → How to Choose the Right Sealing Length and Sealing Width → Sealing Machine Maintenance: 7 Ways to Extend Service Life About This Article This article was prepared by the Daily Sealing System technical team for purchasing teams, packaging engineers, production managers, contract packers and industrial packaging users. Daily Sealing System Co., Ltd. is a Taiwan-based sealing machine manufacturer with an in-house production facility. The company provides impulse sealers, constant heat sealers, foot sealers, continuous band sealers, vacuum sealers, medical pouch sealers and customized sealing equipment, together with OEM / ODM support and after-sales technical service. This guide is based on Daily Sealing System's sealing-machine manufacturing, packaging-material application testing and after-sales technical support experience since 2010. The inspection methods described here are intended as general industrial packaging guidance. Where a product is subject to formal quality, regulatory or customer requirements, the applicable test method and acceptance criteria should take priority. Need Help Evaluating Seal Quality for Your Packaging Application? Send us your machine model, pouch material structure, pouch thickness, bag dimensions, product type, sealing temperature, sealing time, current seal appearance, photos of the defective seal, production volume and applicable quality requirements. Our technical team can help you identify whether the issue is more likely related to the packaging material, process settings, machine configuration or equipment condition. View Sealing Machines Contact Our Technical Team // //MORE
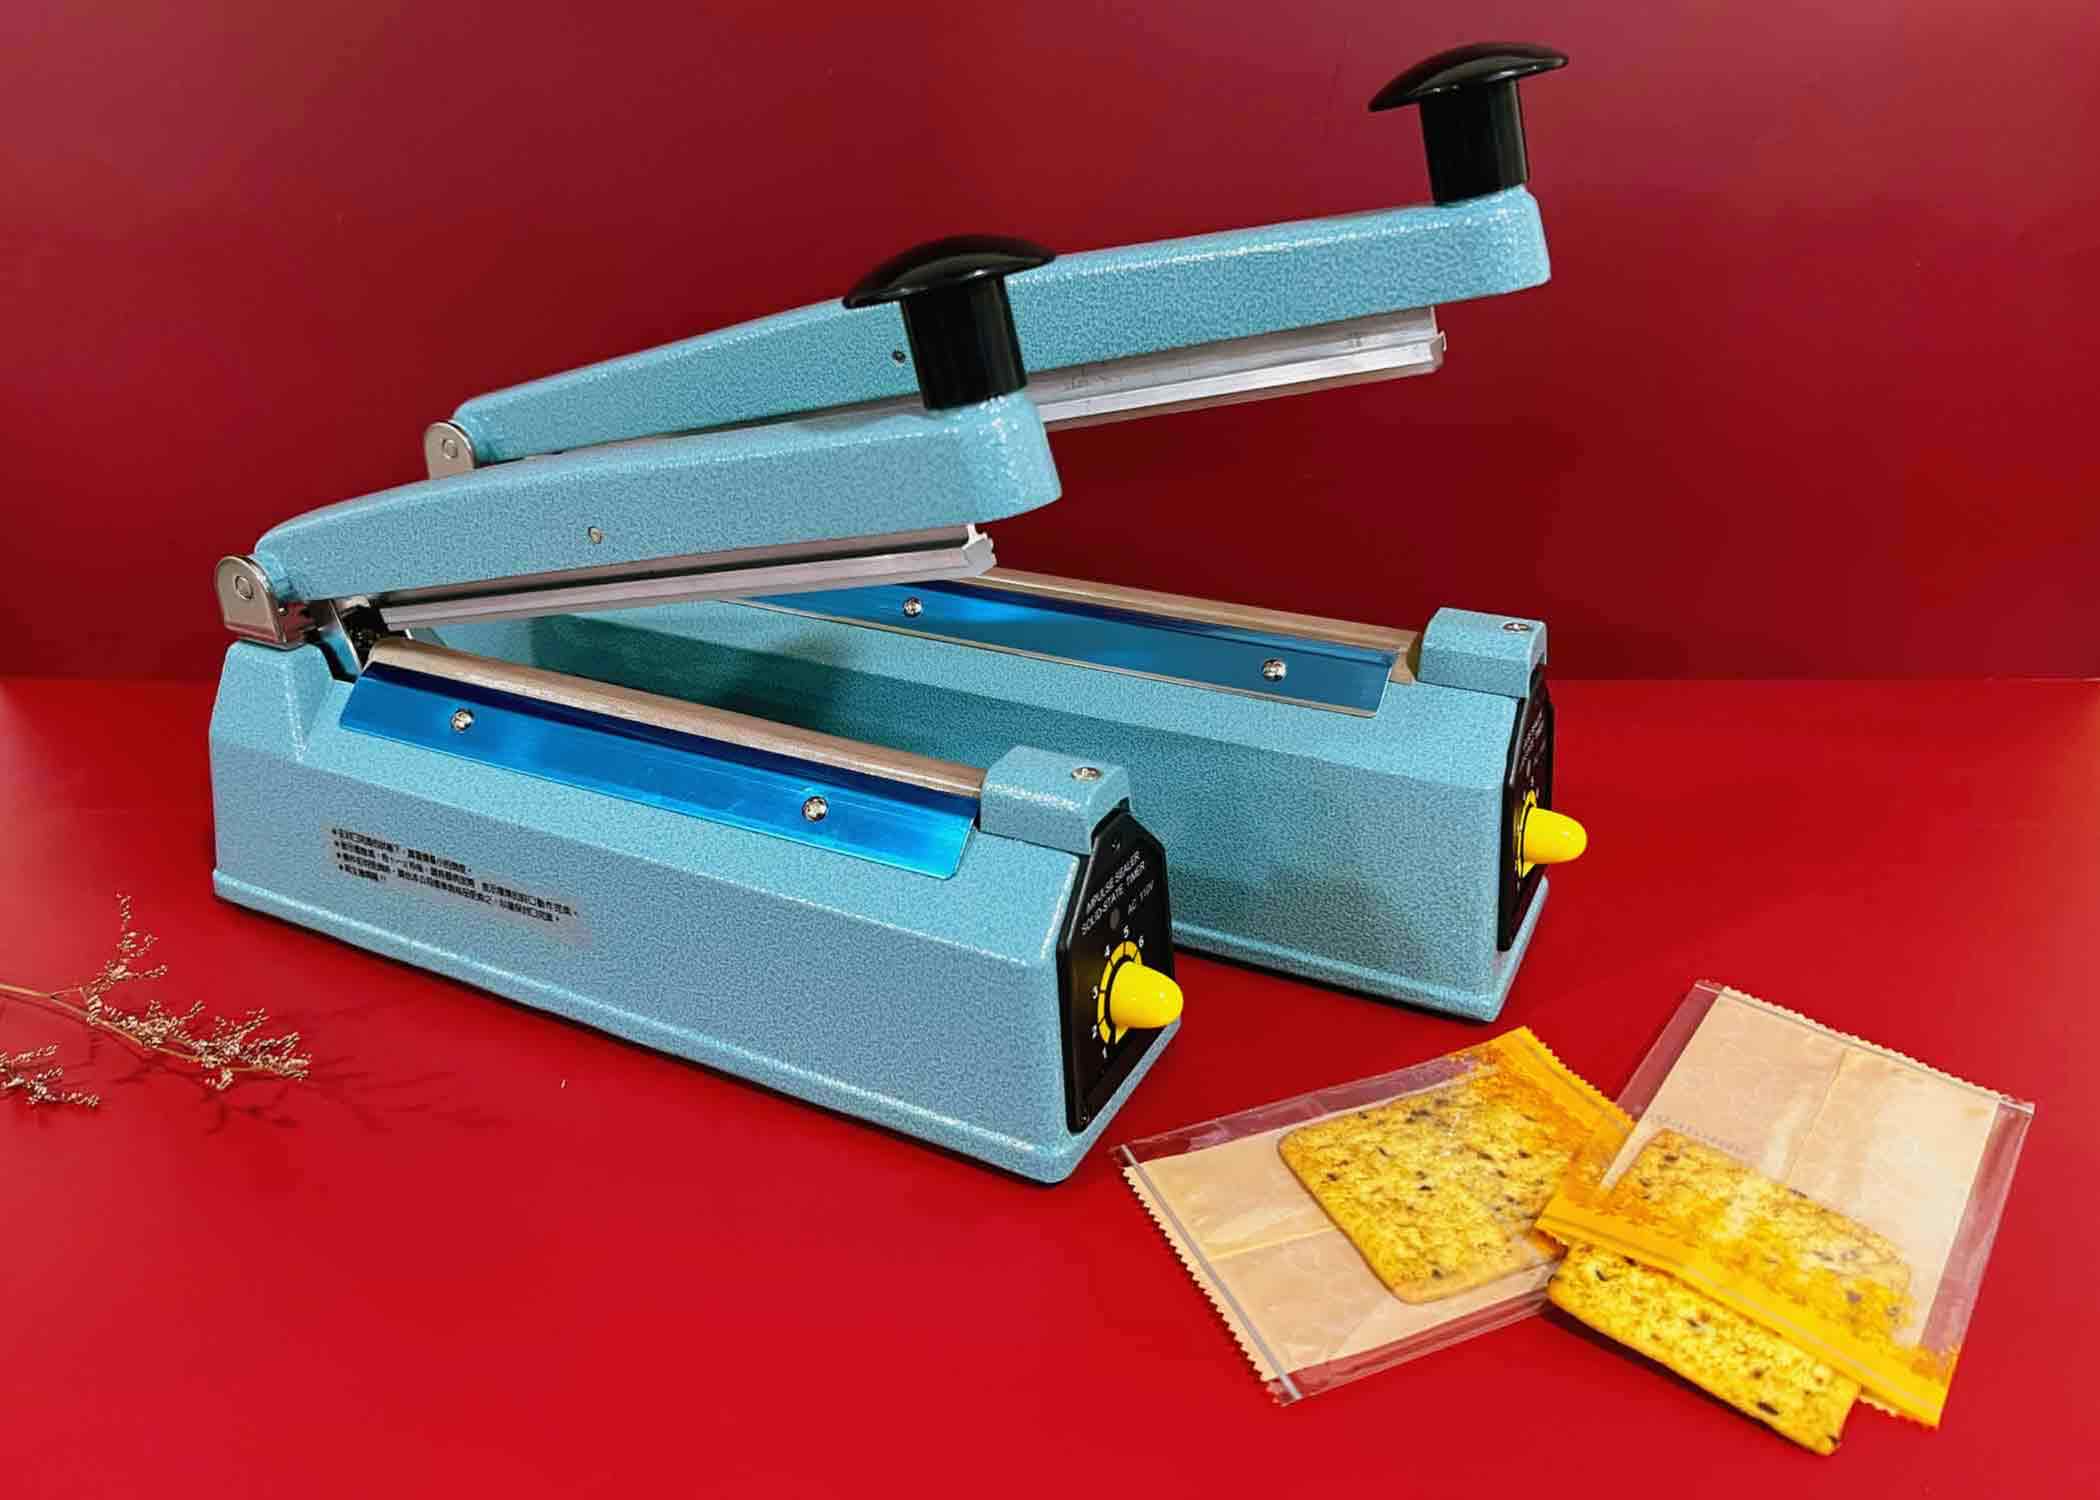 2026/8/11Sealing Machine Maintenance: 7 Ways to Extend Service LifeHow to Extend Sealing Machine Service Life: 7 Maintenance and Operating Practices For food processors, manufacturers, contract packers and other B2B packaging operations, a sealing machine is often a critical part of daily production. Equipment condition can directly affect seal consistency, production throughput, maintenance workload and the risk of unplanned downtime. Even two identical machines can have very different service lives when they are operated under different production conditions. Correct heat-sealing settings, routine cleaning and timely replacement of worn consumables are three of the most practical ways to reduce unnecessary equipment wear. This guide explains seven maintenance and operating practices for impulse sealers, foot sealers, continuous band sealers, vacuum sealers and other industrial sealing equipment. Quick Answer: 7 Ways to Extend Sealing Machine Service Life Use the correct heat-sealing settings — avoid excessive temperature or heating time. Use packaging materials compatible with the machine — confirm pouch structure, thickness and sealing method. Clean the sealing area after production — remove oil, powder and product residue. Operate within the machine's rated duty cycle — do not continuously overload intermittent-duty equipment. Inspect and replace worn consumables — heating elements, PTFE covers and silicone pads should be checked regularly. Store equipment correctly — protect the machine from moisture, dust and unnecessary environmental exposure. Maintain equipment records — document consumable replacement, settings and abnormal events. 1. Use the Correct Heat-Sealing Settings Excessive heat is one of the common causes of premature wear on sealing-machine consumables. Production operators sometimes assume that a higher temperature or longer heating time will always create a stronger seal. In practice, excessive thermal input can shorten the service life of heating elements, PTFE covers and silicone pressure pads while also damaging the packaging material. It is also important to understand that not every machine directly controls temperature. Impulse sealers typically control heating time or output, while constant heat sealers and continuous band sealers commonly use adjustable temperature controls. Potential Effects of Excessive Heat Heating elements may oxidize, become brittle or fail sooner PTFE covers or heat-resistant tape may discolor, carbonize or wear faster Silicone pressure pads may deform and reduce pressure uniformity Packaging film may burn, shrink or stick to the sealing surface Heat stress may increase wear on surrounding machine components Better Sealing-Setting Practice Confirm pouch material, structure and thickness Start from the recommended heat or timing range Run sample seals before full production Re-test when the packaging material or supplier changes Record validated machine settings for repeat production Related Guide: Heat-sealing conditions vary significantly by packaging material. Refer to our Heat Sealing Temperature Guide for Different Packaging Materials. 2. Use Packaging Materials Compatible with the Sealing Machine Packaging-material compatibility is an important factor in both seal quality and machine life. Different pouch structures require different heating methods, sealing times, pressures and machine configurations. Using a machine outside its intended material range may force operators to compensate with excessive heat or extended sealing time, which can increase consumable wear without solving the actual compatibility problem. Common Material-to-Machine Compatibility Issues: Thick foil laminates on a standard impulse sealer: Some multi-layer foil pouches require stable, adjustable heat that a basic impulse sealing system may not provide. Confirm pouch structure and machine capability before production. Vacuum embossed bags on an incompatible vacuum system: Embossed vacuum bags are commonly used with specific external vacuum systems. Incorrect bag and machine combinations may result in poor air extraction, weak seals or vacuum loss. Bag width exceeding the sealing length: The full bag opening must fit within the effective sealing length. Increasing heat cannot compensate for a bag opening that extends beyond the sealing bar. Using excessive temperature to compensate for thick material: Pouch thickness is only one factor. Heat method, dwell time, pressure and sealing width should be evaluated together. 3. Clean the Sealing Area After Daily Production Routine cleaning is one of the simplest preventive-maintenance practices for sealing equipment. Powder, oil, food particles, adhesive residue and moisture can accumulate around the sealing area. Repeated heating may carbonize this contamination, affecting heat transfer and gradually damaging PTFE covers, heating elements and pressure surfaces. Daily Cleaning Checklist Remove powder, oil and product residue from the sealing area Inspect the PTFE surface for contamination or damage Remove carbonized residue around the heating area Inspect the sealing bar and pressure surface Confirm that ventilation openings are not blocked Cleaning Precautions Disconnect the machine from power before maintenance when required by the equipment manual Allow heated components to cool before cleaning Avoid applying liquid cleaner directly to electrical or heating components Do not scrape PTFE surfaces with sharp or abrasive tools Follow the machine manufacturer's cleaning instructions 4. Operate Within the Machine's Rated Duty Cycle Different sealing machines are designed for different production volumes and operating patterns. A small impulse sealer used intermittently has a different duty requirement from a continuous band sealer designed for higher-volume production. For B2B buyers, machine selection should therefore be based not only on sealing length and material type, but also on hourly output, daily production volume and expected operating time. Machine TypeTypical Operating PatternMaintenance / Operating Consideration Hand Impulse Sealer Intermittent manual sealing for low- to medium-volume packaging Follow the rated duty cycle and observe seal consistency during repetitive operation. If production volume is consistently high, evaluate a higher-duty machine. Foot Impulse Sealer Repeated manual sealing where hands-free operation improves workflow Monitor seal consistency, heating element condition and production frequency. Avoid exceeding the manufacturer's recommended duty cycle. Continuous Band Sealer Continuous higher-volume packaging Monitor heater condition, temperature stability, conveyor speed and moving components. Follow the manufacturer's inspection and maintenance schedule. Vacuum Sealer Vacuum extraction and sealing performed as a production cycle Inspect vacuum-pump performance, sealing components and rated cycle frequency. For oil-lubricated pumps, maintain pump oil according to the equipment manual. 5. Inspect Consumables and Replace Them Before Failure Affects Production Heating elements, PTFE covers and silicone pressure pads are normal wear components on many sealing machines. Their service life depends on machine type, production frequency, material structure, heat settings and operating conditions. Instead of replacing consumables only after a complete failure, establish regular inspection points and replace parts when visible wear or seal-quality deterioration appears. This helps reduce the risk of secondary damage and unexpected production interruption. Heating Element / Heater Wire Inspect when: seal lines become uneven, heating becomes inconsistent, the element shows visible discoloration, deformation or signs of fatigue. Why it matters: a deteriorated heating element may create localized heating problems and can also damage the PTFE cover or pressure surface. PTFE Cover / Heat-Resistant Tape Inspect when: the surface shows abrasion, holes, burnt areas, contamination or sticking during sealing. Why it matters: damaged PTFE material may allow packaging film to contact the heating element directly, leading to sticking, contamination and additional component wear. Silicone Rubber Pad Inspect when: the pad becomes hardened, uneven, permanently compressed or visibly damaged. Why it matters: an uneven pressure surface can cause inconsistent sealing pressure across the seal line. 6. Store Sealing Equipment in a Clean, Dry Environment Equipment condition can deteriorate even during periods when the machine is not in production. Moisture, dust, direct sunlight and poor storage practices may affect metal components, electrical systems, rubber parts and ventilation paths. Recommended Storage Practices: Keep equipment dry: store machines away from water sources, condensation and excessive humidity. Control dust: use an appropriate protective cover during extended idle periods while keeping required ventilation areas clear. Avoid direct sunlight and heat: prolonged exposure may accelerate aging of plastics and rubber components. Store power cables correctly: avoid excessive bending, crushing or tension on the cable and plug. Before restarting after long-term storage: inspect the power cable, heating components, moving parts and machine exterior before trial operation. For vacuum sealing machines: check vacuum-pump condition before restarting. Oil-lubricated pumps should be inspected and serviced according to the manufacturer's instructions. 7. Keep a Preventive Maintenance and Consumables Record For sealing equipment used every day, a simple maintenance record helps production and purchasing teams understand component replacement patterns, identify recurring failures and prepare spare parts before a machine stops unexpectedly. Recommended Maintenance Record Items: Machine information: model, serial number, purchase date and production line Consumable replacement: heating element, PTFE cover, silicone pad and other wear parts Process settings: validated temperature, sealing time and conveyor speed for each packaging material Seal-quality observations: recurring seal defects and corrective actions Abnormal events: unusual noise, overheating, vacuum loss, electrical issues or emergency maintenance Spare-parts inventory: critical consumables and replacement components currently in stock A maintenance record does not need to be complicated. A spreadsheet, maintenance form or digital equipment-management system can be sufficient. The key is consistent documentation so that operators, maintenance staff and purchasing teams can identify trends and plan replacement parts in advance. B2B Maintenance Priority Summary Maintenance AreaWhy It MattersRecommended Action Sealing settings Excessive heat or time increases wear and can damage packaging material Validate settings for each pouch structure and document them Daily cleaning Residue affects heat transfer and consumable condition Clean and inspect the sealing area after production Consumables Worn parts can cause seal inconsistency and secondary damage Inspect regularly and keep critical spare parts available Duty cycle Equipment selected for insufficient production volume may be overloaded Match machine type to required output and operating hours Maintenance records Recurring failures and spare-part usage become easier to identify Record replacement dates, failures and process settings Key Principle: Proper sealing settings, routine cleaning and timely consumable inspection are relatively simple preventive-maintenance practices that can help reduce unnecessary wear and improve production consistency. Sealing Machine Spare Parts and Technical Support from Daily Sealing System Daily Sealing System Co., Ltd. is a Taiwan-based sealing machine manufacturer with an in-house production facility. Our product range includes impulse sealers, foot sealers, constant heat sealers, continuous band sealers, vacuum sealers, medical pouch sealers and customized sealing equipment. For maintenance and replacement-part inquiries, buyers can provide the machine model, serial number, packaging material, production frequency and current operating condition. Our technical team can help identify compatible consumables, replacement parts and maintenance requirements. The following questions reflect common sealing-machine maintenance and service-life concerns from food processors, agricultural packaging companies, electronics manufacturers and industrial packaging users. Frequently Asked Questions Q1: How long does a sealing machine usually last? There is no universal service-life figure for sealing equipment. Machine life depends on production volume, duty cycle, operating environment, packaging materials, maintenance quality and machine design. Replaceable parts such as heating elements, PTFE covers and silicone pads should be inspected separately from the main equipment structure. Q2: What commonly causes premature sealing machine wear? Common causes include excessive heat-sealing settings, contamination around the sealing area, operation beyond the machine's rated duty cycle, incompatible packaging materials and continued use of worn consumables. Regular inspection and correct process settings can reduce these risks. Q3: When should heating elements and PTFE covers be replaced? Replacement should be based on actual condition rather than a universal calendar interval. Inspect these consumables when seal quality becomes uneven, heating becomes inconsistent, PTFE material is worn or burnt, or packaging begins sticking to the sealing surface. Q4: Can a hand impulse sealer be used continuously for high-volume production? A hand impulse sealer is generally intended for intermittent manual operation. Actual duty capability varies by model. For sustained higher-volume production, buyers should compare required output, operating hours and cycle frequency with the machine specification and consider a foot sealer, semi-automatic sealer or continuous band sealer when appropriate. Q5: What maintenance information should purchasing teams keep for sealing equipment? Keep the machine model and serial number, consumable replacement history, validated sealing settings, maintenance dates, abnormal-event records and spare-parts inventory. These records make it easier to plan preventive maintenance and source replacement parts before an unexpected shutdown. Further Reading Related guides for sealing-machine buyers, maintenance teams and production managers: → Sealing Machine Maintenance Guide: How Often Should You Service Your Equipment? → Heat Sealer Not Sealing Properly? Common Causes & Fixes → How to Choose the Right Sealing Length and Sealing Width → Sealing Machine Buying Guide: How to Choose the Right Sealer → When Should You Use a Continuous Band Sealer? About This Article This article was prepared by the Daily Sealing System technical team for purchasing teams, maintenance personnel, production managers and industrial packaging users. Daily Sealing System Co., Ltd. is a Taiwan-based sealing machine manufacturer with an in-house production facility. The company manufactures vacuum sealers, impulse sealers, foot sealers, constant heat sealers, continuous band sealers, medical pouch sealers and customized sealing equipment, and provides OEM / ODM support. The company operates under ISO 9001:2015 quality management practices. Certain products and related packaging materials have CE, FDA, EU No.10/2011 and BPA Free compliance or certifications depending on the product and application. This guide is based on Daily Sealing System's manufacturing, maintenance and after-sales technical support experience since 2010. Actual maintenance intervals and replacement timing vary by machine model, usage frequency, packaging material and production environment, so always follow the applicable machine manual and maintenance recommendations. Need Help with Sealing Machine Maintenance or Replacement Parts? Send us your machine model, serial number, packaging material, production frequency and current operating condition. Our technical team can help you evaluate consumables, maintenance requirements and whether a different machine configuration would better match your production volume. View Sealing Machines Contact Our Technical Team // //MORE
.jpg) 2026/8/10Heat Sealing Temperature Guide for Different Packaging MaterialsDo Different Packaging Materials Require Different Sealing Temperatures? Heat Sealing Temperature Guide When switching from one packaging material to another, many production teams continue using the same heat sealer settings. This often results in weak seals, burnt seal lines, pouch deformation, leakage, or inconsistent seal quality. Based on Daily Sealing System's practical experience in sealing machine manufacturing and after-sales technical support since 2010, different packaging materials, sealant layers and material thicknesses require different heat sealing conditions. Selecting the correct sealing temperature is therefore one of the first steps toward achieving reliable and repeatable seal quality in a B2B packaging operation. A setting that is too low may result in insufficient bonding, while excessive heat can distort the pouch and accelerate wear on sealing-machine consumables. Quick Answer: Key Principles for Heat Sealing Temperature Settings Different packaging materials require different heat sealing conditions. Material structure and sealant-layer composition are as important as total pouch thickness. Always re-test sealing settings when changing pouch material, supplier, structure or thickness. A temperature that is too low may cause weak or incomplete seals. Excessive temperature may burn, distort or melt the packaging material and accelerate consumable wear. For production validation, start from the machine or material supplier's recommended range and adjust incrementally using sample pouches. Temperature is only one variable — dwell time, pressure, sealing width and conveyor speed can also affect final seal quality. 1. Why Do Different Packaging Materials Require Different Sealing Temperatures? A heat sealer applies thermal energy to the sealant layer of a pouch or bag. The two inner surfaces soften and bond under controlled heat and pressure, then form a seal as the material cools. Different pouch structures use different sealant materials, thicknesses and laminated layers. This means that the same machine setting may produce a strong seal on one material but an incomplete or burnt seal on another. When Sealing Temperature Is Too Low Sealant layers do not fully bond Seal line appears closed but opens under light pressure Vacuum bags may lose vacuum after sealing Thicker laminated pouches may seal inconsistently Parts of the seal line may remain unfused When Sealing Temperature Is Too High Seal line becomes burnt or discolored Pouch material melts through at the sealing area Seal edges become wrinkled or distorted Thin PE or heat-sealable OPP structures are particularly sensitive Heating elements and PTFE tape may wear faster 2. Reference Heat Sealing Temperature Ranges by Packaging Material The following ranges are intended as starting references for process testing, not universal production specifications. Actual settings can vary depending on pouch supplier, sealant-layer composition, total material thickness, machine design, sealing pressure, dwell time and production speed. For procurement and production teams, the safest approach is to confirm the material specification with the pouch supplier and then perform a sample sealing test on the actual machine before mass production. Packaging MaterialStarting Temperature Reference*Typical ApplicationsPurchasing / Production Notes Thin PE Bags Approx. 120–160°C Snacks, dry products, general lightweight packaging Relatively heat-sensitive. Start conservatively and verify actual material specifications before production. Heat-Sealable OPP / OPP Laminates Approx. 120–160°C Stationery, lightweight goods, food and retail packaging Confirm that the structure includes a heat-sealable layer. Pure OPP film structures may require different converting or sealing conditions. NY/PE Laminated Vacuum Bags Approx. 170–200°C Meat, seafood, agricultural products, vacuum packaging Settings depend strongly on laminate thickness, sealant layer and vacuum-sealer design. Confirm seal width and machine compatibility. PET/PE Laminated Pouches Approx. 170–200°C Food packaging, industrial components, general laminated packaging The PET outer layer provides heat resistance while the inner PE-based sealant layer forms the bond. Process settings must deliver sufficient heat to the sealant layer without damaging the laminate. Aluminum Foil / Foil-Laminated Pouches Approx. 180–220°C Coffee, tea, pharmaceutical packaging, moisture-sensitive industrial products Thicker foil laminates commonly require an adjustable-temperature constant heat sealer. Confirm pouch structure, sealant layer and equipment compatibility before purchase. Thick Multi-Layer Laminated Pouches May require 200°C or above depending on structure Heavy industrial products, agricultural bulk packaging, specialty packaging Do not increase temperature alone. Dwell time, sealing pressure, sealing width and heating method should be evaluated together. Important: The temperature ranges above are starting references only. Packaging films with the same generic material name can use different resin grades, sealant layers and laminate structures. Whenever the pouch material, supplier, thickness or structure changes, run a new sealing test before starting production. 3. How to Determine the Correct Heat Sealing Temperature There is no single sealing temperature that works for every material and every heat sealer. For B2B production, the correct approach is to establish a controlled test procedure and document the validated setting for each packaging material. 01 Identify the Material Confirm pouch structure, sealant layer and thickness — for example PE, NY/PE, PET/PE or foil laminate. 02 Set a Starting Point Use the machine manufacturer's or packaging-material supplier's recommended range as the starting point. 03 Run Sample Seals Use production-equivalent sample pouches and inspect seal appearance, continuity and initial seal strength. 04 Adjust Incrementally Increase heat gradually if the seal is weak. Reduce the setting if the pouch burns, distorts or melts. 05 Document the Setting Record pouch supplier, material structure, thickness, machine model, temperature and other relevant process settings. 4. How Can You Verify Whether the Seal Is Strong Enough? Temperature setting alone does not confirm seal quality. After establishing an initial setting, the production team should verify the actual seal according to the packaging requirements and internal quality-control criteria. Practical Seal Quality Checks: Visual Inspection: The seal line should be continuous and even, without burn marks, excessive wrinkles, holes or obvious unfused sections. Manual Pull Check: Apply even force to both sides of the sealed area. A properly bonded seal should not peel open easily under normal handling conditions. Vacuum Hold Observation: For vacuum packaging, monitor the package over a defined internal QC period to check for loss of vacuum, leakage or package rebound. A 24-hour observation may be used as an internal screening step, but it is not a universal industry standard. Production QC Testing: For applications with defined seal-integrity requirements, consider peel-strength, leak, burst or vacuum-decay testing according to your internal quality specification. Cross-Section Review: For troubleshooting, inspect the seal area for uniform fusion and signs of delamination. 5. Six Common Heat Sealing Temperature Mistakes 1. Changing Pouch Material Without Re-Testing Even materials with the same generic name can use different resin grades, thicknesses and sealant layers. Re-test whenever the pouch supplier or specification changes. 2. Assuming Higher Temperature Means a Stronger Seal Excessive heat can damage the pouch, distort the seal area and accelerate wear on heating elements and PTFE tape. 3. Ignoring Heat Build-Up During High-Volume Production During extended production runs, equipment temperature and process conditions may change. Periodically inspect seal quality instead of assuming the first validated setting remains optimal throughout the shift. 4. Looking Only at Material Thickness Thickness matters, but laminate structure, sealant layer, dwell time, sealing pressure and heating method can be equally important. 5. Sealing Through Oil, Moisture or Powder Contamination at the bag opening can prevent proper bonding even when the temperature setting is correct. Keep the sealing area clean and dry before sealing. 6. Using the Wrong Heating Method for Thick Foil Laminates Some thick multi-layer foil pouches require stable, adjustable heat that a standard impulse sealer may not provide. Confirm the pouch sealant structure and machine capability, and evaluate an adjustable-temperature constant heat sealer when required. 6. How Sealing Settings Differ by Machine Type Not every sealing machine controls heat in the same way. For purchasing teams, understanding the difference between time-controlled impulse sealing and temperature-controlled constant heat sealing is especially important. Sealing Machine TypePrimary Setting MethodB2B Purchasing / Production Notes Hand Impulse Sealer Sealing time / heating-time control rather than direct temperature setting Commonly used for PE and other compatible plastic bags. Material compatibility should be confirmed before purchasing. Foot Impulse Sealer Heating-time control Suitable for repetitive manual packaging where hands-free operation improves workflow. High-frequency use requires monitoring of seal consistency. Constant Heat Sealer Direct adjustable temperature control Often preferred for foil laminates, vacuum nylon bags and other thicker or multi-layer packaging materials requiring stable continuous heat. Continuous Band Sealer Temperature setting + conveyor speed Designed for higher-volume production. Temperature and line speed must be optimized together to maintain consistent heat input. Vacuum Sealer Sealing time or temperature depending on machine design Vacuum extraction and sealing are separate process stages. Confirm bag type, sealing method, seal width and production requirements before equipment selection. 7. Continuous Band Sealer: Why Temperature and Conveyor Speed Must Be Adjusted Together For a continuous band sealer, seal quality is determined by the combined effect of temperature, conveyor speed and material characteristics. Higher conveyor speed → shorter exposure time in the heating zone → process settings may need adjustment to maintain sufficient heat input. Lower conveyor speed → longer heat exposure → excessive temperature may distort or burn the pouch. Whenever pouch structure, thickness or conveyor speed changes, re-test the sealing conditions. Use sample material before a full production run and confirm that the seal line is continuous, undamaged and sufficiently strong for the intended application. B2B Buyer Checklist: Information to Prepare Before Selecting a Heat Sealer Packaging material structure: PE, OPP laminate, NY/PE, PET/PE, foil laminate, etc. Total pouch thickness and sealant-layer specification Bag opening width and required sealing length Required sealing width or number of seal lines Product type: dry, oily, powder, liquid, food, industrial component or medical product Daily production volume and required cycle speed Current sealing temperature, time or conveyor-speed settings Required seal-integrity or internal QC criteria Available power supply and production-line configuration Daily Sealing System Can Help Evaluate the Right Sealing Conditions for Your Packaging Material Daily Sealing System Co., Ltd. is a Taiwan-based sealing machine manufacturer with an in-house production facility. Our product range includes impulse sealers, constant heat sealers, foot sealers, continuous band sealers, vacuum sealers, medical pouch sealers and customized sealing equipment. For a new packaging project, buyers can provide the machine model, pouch structure, material thickness, bag dimensions, product type and daily output requirement so our technical team can help evaluate the appropriate sealing-machine configuration and starting process settings. The following questions are based on common sealing-temperature and packaging-material inquiries handled by Daily Sealing System's technical and after-sales service team across food processing, agricultural packaging, electronics manufacturing and industrial packaging applications. Frequently Asked Questions Q1: Do different packaging materials require different sealing temperatures? Yes. Different packaging films use different sealant layers, resin structures and thicknesses, so the same temperature setting may produce a weak seal on one material and burn another. Whenever the material, supplier, laminate structure or thickness changes, the sealing conditions should be re-tested before production. Q2: Does a higher sealing temperature always produce a stronger seal? No. The goal is to apply enough thermal energy to create a reliable bond without damaging the pouch. Excessive heat can distort the seal area, melt through the bag, weaken the laminate structure and accelerate wear on sealing-machine consumables. Q3: What type of sealer is recommended for aluminum foil or laminated foil pouches? Thick multi-layer foil laminates often require stable, adjustable heat so that sufficient thermal energy reaches the inner sealant layer. An adjustable-temperature constant heat sealer is commonly evaluated for these applications. However, machine selection should be based on the actual pouch structure, thickness, sealing width and production requirements rather than material name alone. Q4: How should I adjust the temperature of a continuous band sealer? Continuous band sealing depends on both temperature and conveyor speed. Increasing line speed reduces the time the pouch remains in the heating zone, while slower speed increases heat exposure. Whenever the material or production speed changes, test both parameters together and confirm seal quality before full production. Q5: How do I know whether my heat sealing temperature is correct? Start with a visual inspection: the seal line should be continuous and free from burns, holes and obvious unfused sections. Then perform an appropriate strength or leak check for the packaging application. For vacuum packaging, monitor whether the package maintains vacuum over your defined QC observation period. Once the process is validated, record the material specification, machine model and sealing settings for repeat production. Further Reading Related technical guides for sealing-machine buyers, production managers and packaging engineers: → Heat Sealer Not Sealing Properly? 5 Common Causes & Fixes → Sealing Machine Maintenance Guide: How Often Should You Service Your Equipment? → How to Choose the Right Sealing Length and Sealing Width → Sealing Machine Buying Guide: How to Choose the Right Sealer → When Should You Use a Continuous Band Sealer? About This Article This article was prepared by the Daily Sealing System technical team for purchasing teams, packaging engineers, production managers and industrial packaging users. Daily Sealing System Co., Ltd. is a Taiwan-based sealing machine manufacturer with an in-house production facility. Our product portfolio includes vacuum sealers, external vacuum sealers, chamber vacuum sealers, impulse sealers, constant heat sealers, foot sealers, continuous band sealers, medical pouch sealers and customized sealing equipment. The company holds ISO 9001:2015 certification. Certain products and related packaging materials carry CE, FDA, EU No.10/2011 and BPA Free certifications. Patents are registered in Taiwan, the United States, Europe, Germany, Japan and China. The content in this guide is based on Daily Sealing System's practical manufacturing experience, packaging-material testing and after-sales technical support since 2010. The temperature ranges provided are starting references only; actual production settings should always be validated using the specific pouch material and machine configuration. Need Help Matching Your Packaging Material to the Right Heat Sealer? Send us your pouch material, thickness, bag size, product type, required daily output and current sealing-machine model. Our technical team can help you evaluate the appropriate sealing-machine configuration and starting process settings for your packaging application. View All Sealing Machines Contact Our Technical Team // //MORE
.jpg) 2026/7/14Sealing Machine Maintenance Guide: How Often Should You Service Your Equipment?How Often Should You Maintain Your Sealing Machine? Preventive Maintenance Guide for Better Seal Quality Sealing machines are critical equipment in food processing, agricultural packaging, electronics, and industrial manufacturing — but many operators only consider maintenance after a seal quality problem has already appeared. Waiting until failure typically means higher repair costs, unexpected production downtime, and avoidable product loss. Based on Daily Sealing System's practical experience in sealing machine manufacturing and after-sales technical support since 2010, the majority of seal quality problems can be prevented through consistent preventive maintenance. This guide explains how often to maintain your sealing machine, what to inspect at each interval, and how to identify when consumable parts need to be replaced. Quick Answer: How Often Should You Maintain a Sealing Machine? Most sealing machines should be inspected weekly or monthly depending on production volume. Here is the recommended schedule by usage level: Occasional use: Full inspection every 3–6 months Daily use: Monthly inspection of heating wire (nichrome wire), PTFE tape, and seal quality High-volume continuous production: Weekly inspection of heating system, consumables, and full machine cleaning Any usage level: If seal quality declines at any point, inspect consumables immediately — do not wait for the next scheduled date Regular maintenance helps extend the service life of sealing machines and prevents most seal quality problems before they affect production output. 1. Why Do Sealing Machines Need Preventive Maintenance? A sealing machine relies on its heating wire (nichrome wire), PTFE tape (Teflon tape), heating system, and pressure mechanism to create a consistent seal. All of these components are subject to natural wear over time. A preventive maintenance schedule reduces unexpected downtime and repair costs — and allows problems to be identified and corrected before they escalate into seal failures or production stoppages. Consequences of Neglected Maintenance Weak or incomplete seals — increased leakage risk Burnt or discolored seal lines Uneven seal appearance affecting product presentation Reduced sealing throughput Significantly shortened equipment service life Higher repair and replacement costs Benefits of Regular Preventive Maintenance Consistent seal quality across every production run Reduced risk of unexpected equipment failure Extended overall equipment service life Lower repair and consumable costs over time Reduced packaging defect rate Improved production line reliability and uptime 2. Sealing Machine Maintenance Schedule There is no single fixed maintenance interval that applies to all sealing machines. The right schedule depends on usage frequency, daily output volume, and bag material type. From Daily Sealing System's after-sales service experience, machines sealing aluminum foil or thick laminated bags wear through consumables noticeably faster than those sealing standard PE bags — and should be inspected more frequently. Usage FrequencyRecommended Maintenance IntervalMain Inspection Items Occasional use (less than daily) Every 3–6 months Consumable appearance, power cable, seal quality test Daily regular use Monthly Heating wire, PTFE tape, silicone strip, full cleaning High-volume continuous production Weekly Heating wire, PTFE tape, heating system, full machine cleaning Any usage level — seal quality declines Immediately Inspect consumables first — do not wait for the next scheduled date 📌 Key principle: Most sealing quality problems can be prevented through routine maintenance. If seal quality starts declining between scheduled maintenance dates, check consumables immediately — this is almost always the fastest, lowest-cost solution. 3. Preventive Maintenance Checklist Use this checklist to establish a consistent maintenance routine across your production operation. Heating wires (nichrome wire) and PTFE tape (Teflon tape) are consumable parts that require periodic replacement — but proper daily care extends their service life considerably. ⚙️ Before Every Shift ☐ Visually inspect PTFE tape surface ☐ Check heating wire appearance ☐ Run a test seal with a scrap bag ☐ Confirm temperature setting is correct 🗓 Daily (End of Shift) ☐ Clean sealing area — remove powder, oil, debris ☐ Inspect PTFE tape for damage or burn marks ☐ Confirm heating wire shows no discoloration ☐ Allow machine to cool before shutdown 📅 Weekly ☐ Inspect heating wire for uneven width or gaps ☐ Check PTFE tape for holes or worn areas ☐ Check all screws and fasteners for looseness ☐ Verify temperature settings vs. production requirements 🔧 Monthly ☐ Replace PTFE tape proactively if showing wear ☐ Inspect power cable for visible damage ☐ Deep clean the full sealing area ☐ Review seal quality trend from past month 📋 Quarterly ☐ Full equipment inspection ☐ Replace heating wire if showing any deterioration ☐ Test temperature calibration accuracy ☐ Contact manufacturer if performance has declined 4. Heating Wire (Nichrome Wire) Replacement: When and How to Tell The heating wire — also referred to as nichrome wire or sealing wire — is a primary consumable component in impulse sealers and continuous band sealers. It has no fixed replacement interval. Replacement timing depends on usage frequency, bag material type, and observed seal quality. From Daily Sealing System's technical service experience, machines sealing thicker materials or running high daily volumes will wear through heating wire (nichrome wire) significantly faster. Signs the heating wire (nichrome wire) needs replacing: Seal line width is uneven — some sections visibly narrower than others Gaps or unheated sections appear within the seal line Heating is non-uniform — part of the seal holds, other sections do not Heating wire appears visibly discolored, brittle, or has broken through Increasing temperature does not improve seal quality Heating wire (nichrome wire) is a user-replaceable consumable on most sealing machine models. Daily Sealing System can supply original-specification replacement parts and confirm the correct part number for your machine model. 5. PTFE Tape (Teflon Tape) Replacement: When and How to Tell PTFE tape (Teflon tape) acts as a non-stick barrier between the bag material and the heating wire, preventing the bag from sticking to the sealing bar during heat bonding. PTFE tape wear is one of the most commonly overlooked causes of declining seal quality. Signs PTFE Tape Needs Replacing Bag material sticks to the sealing bar during operation Irregular pressure marks or uneven texture on the seal line surface Visible holes, tears, or burnt areas on the tape surface Overall seal line appearance has declined without another obvious cause Replacement Notes Ensure the machine has fully cooled before replacing PTFE tape Confirm the new tape matches the original manufacturer specification Apply the tape flat — no wrinkles or bubbles Run a test seal with a scrap bag after installation Contact the manufacturer if unsure of the correct specification 6. What Can You Handle In-House — and When to Call a Technician? Most routine sealing machine maintenance can be performed by the equipment operator without specialist tools. Issues involving internal components or control systems should be handled by a qualified technician to avoid additional damage or warranty issues. Maintenance TaskIn-HouseContact Manufacturer Clean sealing area ✅ Replace heating wire (nichrome wire) ✅ Most models Replace PTFE tape (Teflon tape) ✅ Per operating manual Check and tighten fasteners ✅ Visual check of power cable ✅ Temperature control malfunction or display error ✅ Control board failure ✅ Motor noise or abnormal vibration ✅ Vacuum system not achieving vacuum ✅ Progressive overall performance decline ✅ 7. Operational Habits That Extend Sealing Machine Service Life Beyond scheduled maintenance, daily operating habits have a direct impact on how long a sealing machine performs reliably. Based on Daily Sealing System's after-sales technical service experience, premature equipment wear is often caused by operating practices rather than product quality issues. Use Compatible Bag Materials Mismatched bag materials accelerate consumable wear. Before sealing a new material type — PE bags, aluminum foil, or vacuum bags — confirm it is compatible with your machine's heating method and temperature range. Set the Correct Sealing Temperature Running at excessively high temperatures is one of the primary causes of accelerated consumable degradation. Set temperature based on the bag material specification — not higher than necessary to achieve a reliable seal. Do Not Exceed Operating Limits Impulse sealers and foot sealers have recommended continuous operation limits. During high-frequency use, allow brief cooling intervals to prevent overheating and premature component wear. Replace Consumables Proactively Do not wait for a machine failure before replacing consumables. Proactively replacing heating wire (nichrome wire) and PTFE tape on a maintenance schedule significantly reduces the risk of unexpected production stoppages. Related Products If your sealing machine is consistently underperforming despite regular maintenance, it may be time to evaluate whether a different machine type better fits your current bag material or production volume requirements. Impulse Sealers PE bags, OPP bags, light packaging View Series Continuous Band Sealers High-volume production line sealing View Series Vacuum Sealers Meat, seafood, food preservation View Series Medical Pouch Sealers Sterilization pouches, medical packaging View Series The following questions are compiled from Daily Sealing System's after-sales technical service experience across food processing, agricultural packaging, electronics manufacturing, and industrial packaging clients since 2010. Frequently Asked Questions Q1: How often should I maintain my sealing machine? Most sealing machines should be inspected weekly or monthly depending on production volume. Machines used occasionally should be checked every 3–6 months. Daily-use machines should receive monthly maintenance. High-volume production equipment should be inspected weekly. Regardless of schedule, if seal quality declines at any point, inspect consumables immediately. Q2: Does declining seal quality always require professional repair? Not necessarily. When seal quality declines, the first step is always to inspect the heating wire (nichrome wire) and PTFE tape — these consumables are the most common cause of seal quality problems. In many cases, replacing one or both resolves the issue without any professional repair. If quality does not improve after replacing consumables, contact the manufacturer for technical diagnosis. Q3: How often does the heating wire (nichrome wire) need to be replaced? Heating wire (nichrome wire) has no fixed replacement interval — timing depends on usage frequency and bag material. When the seal line becomes uneven, develops gaps, or the wire shows visible discoloration or brittleness, replace it promptly. Machines used for high-volume daily production or sealing thicker materials such as aluminum foil bags will wear through heating wire more quickly. Q4: Can I replace the PTFE tape (Teflon tape) myself? Yes, on most sealing machine models PTFE tape can be replaced in-house without specialized tools. Allow the machine to cool completely before replacing. Confirm the replacement tape matches the original specification. Run a test seal with a scrap bag after installation to confirm correct fit and restored seal quality. Contact the manufacturer if you are unsure of the correct specification for your model. Q5: Does a sealing machine need to be cleaned regularly? Yes. After each production shift, clean the sealing area to remove powder, oil residue, food debris, and moisture. Residue buildup directly accelerates PTFE tape and heating wire (nichrome wire) degradation, and is a common contributing factor to seal quality problems. Use a dry cloth and confirm the machine has fully cooled before cleaning — avoid applying liquid cleaners directly to heating elements. Q6: How can preventive maintenance reduce downtime? Preventive maintenance reduces downtime by identifying consumable wear and developing performance issues before they cause a production stoppage. Replacing a heating wire or PTFE tape during a scheduled maintenance window takes minutes. Waiting until the machine fails mid-production means unplanned downtime, delayed shipments, and potentially wasted product. A consistent maintenance schedule converts reactive repair time into planned, controlled maintenance windows — significantly improving overall equipment availability and production reliability. 📖 Further Reading Related articles on sealing machine troubleshooting, selection, and performance: → Heat Sealer Not Sealing Properly? 5 Common Causes and How to Fix Them → How to Choose the Right Sealing Machine Based on Product Type → How to Choose the Right Sealing Length and Sealing Width → Vacuum Sealer vs. Continuous Band Sealer: Which Should You Choose? → When Should You Use a Continuous Band Sealer? About This Article This article was prepared by the Daily Sealing System technical team. It is intended as a practical maintenance reference for packaging engineers, production managers, purchasing teams, and industrial packaging operators. Daily Sealing System Co., Ltd. is a Taiwan-based sealing machine manufacturer with an in-house production facility. Our product range includes vacuum sealers, external vacuum sealers, chamber vacuum sealers, continuous band sealers, foot sealers, impulse sealers, medical pouch sealers, and customized sealing equipment. The company holds ISO 9001:2015 certification. Certain products and related materials carry CE, FDA, EU No.10/2011, and BPA Free certifications. Patents are registered in Taiwan, the United States, Europe, Germany, Japan, and China. Content in this article is based on Daily Sealing System's practical manufacturing experience and after-sales technical service since 2010. The recommendations provided in this article are intended for general industrial sealing applications. Maintenance intervals may vary depending on machine model, production volume, and packaging material. Need Help Identifying the Correct Maintenance Schedule for Your Sealing Machine? Our technical team can recommend the appropriate consumables and maintenance intervals based on your machine model and production requirements. Share your machine model and current situation — we'll recommend the most appropriate solution. ✓ Heating wire (nichrome wire) — original specification ✓ PTFE tape (Teflon tape) — multiple widths available ✓ Technical consultation and maintenance guidance ✓ Equipment repair support View All Sealing Machine Series Contact Our Technical Team // //MORE
.jpg) 2026/7/13Why Is My Sealing Machine Not Sealing Properly? Common Causes and How to Fix ThemHeat Sealer Not Sealing Properly? 5 Common Causes and How to Fix Them Sealing machines are straightforward to operate — but seal quality problems are more common than most users expect. Wrinkled seal lines, seals that open under light pressure, burnt or discolored seal lines, and vacuum-sealed bags that lose vacuum quickly are all issues that packaging operators regularly encounter. In most cases, the problem is not a machine failure — it is caused by incorrect temperature settings, incompatible bag material, worn consumables, contamination at the bag opening, or operator technique. This guide covers the five most common causes of poor seal quality, a practical diagnostic table, and a maintenance checklist to help you identify and resolve the issue quickly. Quick Answer: Why Is My Heat Sealer Not Sealing? Most heat sealer problems are caused by one of these five issues: Incorrect sealing temperature — too high or too low, both cause seal failure Wrong bag material — incompatible material leads to weak seals or burnt bags Worn heating wire — degraded wire causes uneven or incomplete sealing Damaged Teflon tape — worn tape produces wrinkled, uneven seal lines Contamination at the bag opening — oil, moisture, or powder prevents proper heat bonding Most issues can be resolved without replacing the machine. Start by checking consumables and temperature settings before contacting a technician. 1. Incorrect Sealing Temperature Sealing temperature is the most direct factor affecting seal quality. Based on Daily Sealing System's practical experience in sealing machine manufacturing and after-sales technical support since 2010, incorrect temperature settings are the single most common cause of poor seal quality. Different bag materials and thicknesses require significantly different sealing temperatures — and what works for one material can burn or fail to bond another. Symptoms: Temperature Too Low Seal line appears closed but opens under light pressure Seal area looks hazy or incompletely fused Vacuum-sealed bags lose vacuum quickly after sealing Thicker bag materials seal inconsistently or fail entirely Symptoms: Temperature Too High Seal line is burnt, discolored, or blackened Bag material melts through or distorts at the seal area Seal line edges are uneven or charred Thin PE or OPP bags are particularly susceptible Recommended fixes: Start from the mid-point of the manufacturer's recommended temperature range and adjust incrementally When switching to a new bag material, always re-test and recalibrate the temperature setting Thicker bag materials generally require higher sealing temperatures During extended high-volume runs, machine temperature may gradually rise — monitor and adjust as needed 2. Incompatible Bag Material Not all sealing machines are compatible with all bag materials. Based on Daily Sealing System's after-sales service experience across food processing, agricultural packaging, and industrial clients, bag material mismatch is one of the most frequently overlooked causes of seal quality problems. Different materials have different melting points and bonding characteristics. Bag MaterialCommon ProblemRecommended EquipmentTypical Application Thin PE bags Burns easily if temperature is too high Impulse sealer Snacks, tea, dry food Aluminum foil / laminated pouches Insufficient bond if temperature is too low Adjustable-temperature constant heat sealer Coffee, pharmaceuticals, industrial parts Vacuum channel bags Cannot achieve vacuum; seal leaks quickly Vacuum sealer Meat, seafood, fresh produce Medical sterilization pouches Seal does not meet medical packaging standards Medical pouch sealer Medical devices, surgical instruments 3. Worn Heating Wire or Teflon Tape The heating wire and Teflon tape (PTFE heat-resistant tape) are the primary consumable components of a sealing machine. Daily Sealing System's after-sales technical team consistently finds that a large proportion of seal quality complaints can be resolved simply by replacing worn consumables — without any need for machine repair. Both components degrade naturally with use and directly affect sealing performance. Signs: Heating Wire Needs Replacing Uneven seal line width along the sealing bar Visible gaps or unheated sections within the seal line Non-uniform heating — partial sections seal, others do not Heating wire appears visibly discolored, brittle, or broken Signs: Teflon Tape Needs Replacing Bag material sticks to the machine during sealing Irregular pressure marks on the seal line surface Visible holes, tears, or burnt areas on the tape surface Overall seal line appearance quality has declined When to Replace When seal quality drops without a clear cause When heating wire shows visible discoloration or brittleness When Teflon tape shows visible wear, holes, or burn marks As part of scheduled routine maintenance checks 4. Contamination at the Bag Opening The sealing area must be completely clean for heat bonding to work effectively. Oil, moisture, powder, or food residue at the bag opening creates a barrier between the two layers of bag material — preventing proper fusion and causing seal failure or leakage. This is one of the most common operational causes of poor seal quality in food processing environments. Common contamination sources and recommended actions: Oil or sauce residue: Avoid contaminating the bag opening during filling. If residue is present, wipe the opening clean with a dry cloth before sealing Moisture or high-water-content products: Ensure the bag opening is dry before sealing. For liquid products, a chamber vacuum sealer allows flat-position operation, minimizing liquid migration to the seal area Powder residue (coffee, flour, spices): Confirm the bag opening is free of powder before sealing — even a small amount of contamination will prevent a reliable seal Overfilled bags: Leave adequate clearance above the fill level to ensure a clean area for sealing 5. Incorrect Operator Technique Even with the correct machine, bag material, and temperature setting, poor operator technique can still produce inconsistent seal results. This is particularly relevant for impulse sealers and foot sealers, where manual handling directly affects the final seal quality. Common operator issues and recommended corrections: Bag opening not pulled flat before sealing: Wrinkles in the bag opening are the most common cause of an uneven seal line — always flatten the bag opening before applying the seal Insufficient dwell time: On impulse sealers, releasing the pressure bar before the material has fully fused produces a weak seal — maintain pressure for the full recommended dwell time Misaligned bag opening: If the bag opening is not centered on the sealing bar, part of the opening may not be sealed, leaving an unsealed gap High-frequency continuous operation: Impulse sealers require a brief cooling interval between seals — operating too rapidly can cause inconsistent results 6. Seal Problem Diagnostic Table Based on Daily Sealing System's after-sales technical service experience, the following table covers the most common seal quality symptoms, their likely causes, recommended corrective actions, and whether the fix can be handled in-house: SymptomMost Likely CauseRecommended ActionDIY Fix? Seal opens under light pressure Temperature too low or dwell time too short Increase temperature; extend dwell time ✅ Yes Seal line burnt or discolored Temperature too high Reduce temperature; confirm bag material compatibility ✅ Yes Wrinkled or uneven seal line Bag opening not flattened; Teflon tape worn Flatten bag before sealing; replace Teflon tape ✅ Yes Seal leaks (non-vacuum bag) Contamination or insufficient seal strength Clean bag opening; increase temperature or seal width ✅ Yes Vacuum bag loses vacuum quickly Incompatible bag material or seal width too narrow Confirm bag type; evaluate wider seal width machine ⚠️ Partial Uneven seal line width or gaps Heating wire worn or damaged Inspect and replace heating wire ✅ Yes Bag material sticks to machine Teflon tape worn or temperature too high Replace Teflon tape; reduce temperature ✅ Yes Seal position offset or skewed Bag not centered on sealing bar Adjust handling; center bag on sealing bar ✅ Yes Problem persists after consumable replacement Temperature control or internal component failure Contact manufacturer technical support ❌ Contact manufacturer 7. Sealing Machine Maintenance Checklist Consistent preventive maintenance significantly reduces the frequency of seal quality problems. Use this checklist to establish a routine maintenance schedule for your sealing equipment: 🗓 Daily ☐ Clean sealing area — remove powder, oil, and debris ☐ Visually inspect Teflon tape for surface damage ☐ Confirm heating wire appearance (no visible discoloration) ☐ Run a test seal before starting production 📅 Weekly ☐ Inspect heating wire for uneven width or gaps ☐ Check Teflon tape for holes or burn marks ☐ Check all screws and fasteners for looseness ☐ Verify temperature settings against production requirements 🔧 Monthly ☐ Replace worn Teflon tape proactively ☐ Inspect power cable for visible wear ☐ Deep clean the full sealing area ☐ Review seal quality logs for any declining trend 📋 Quarterly ☐ Full equipment inspection ☐ Replace heating wire if showing any deterioration ☐ Test temperature calibration accuracy ☐ Contact manufacturer if performance has declined progressively 8. When to Contact a Technical Specialist The following situations warrant contacting your sealing machine manufacturer or a qualified technician. Avoid disassembling the machine internally without professional guidance, as improper handling may cause additional damage or void the warranty. Contact a Technician When: Seal quality has not improved after replacing consumables Machine produces unusual sounds or odors during operation Temperature control display is malfunctioning or unresponsive Heating wire replaced but heating remains uneven Machine is aging and overall performance has declined progressively Information to Prepare Before Contacting Machine model number and purchase date Bag material type and thickness Current temperature setting Specific description of the seal quality symptom Frequency of the issue and when it first occurred Related Products If your current sealing machine is consistently underperforming despite troubleshooting, it may be time to evaluate whether a different machine type better fits your bag material or production volume. Impulse Sealer PE bags, OPP bags, light packaging View Series Continuous Band Sealer High-volume production line sealing View Series Vacuum Sealer Meat, seafood, food preservation View Series Medical Pouch Sealer Sterilization pouches, medical packaging View Series The following questions are compiled from Daily Sealing System's after-sales technical service experience across food processing, agricultural packaging, electronics manufacturing, and industrial packaging clients since 2010. Frequently Asked Questions Q1: Why is my heat sealer not sealing properly? Poor seal quality is most commonly caused by one of five issues: incorrect sealing temperature, incompatible bag material, worn heating wire or Teflon tape, contamination at the bag opening, or incorrect operator technique. Start by checking these five factors systematically — most seal quality problems can be resolved without professional repair. Q2: Why does my seal line look wrinkled or uneven? A wrinkled or uneven seal line is most commonly caused by the bag opening not being pulled flat before sealing, or by Teflon tape that has worn and degraded. First, try flattening the bag opening completely before applying the seal. If the issue persists, inspect the Teflon tape for visible wear or damage and replace it if necessary. Q3: Why is my seal line burnt or turning black? A burnt or blackened seal line indicates that the sealing temperature is set too high, or that the bag material is not compatible with the machine. Reduce the temperature immediately and confirm the bag material is appropriate for the machine type. Aluminum foil bags and standard PE bags require very different sealing temperatures. Q4: Why does my vacuum-sealed bag lose vacuum quickly after sealing? Vacuum bags that lose vacuum quickly typically indicate one of four issues: incompatible bag material (not using a vacuum channel or flat vacuum bag), insufficient seal width, contamination at the bag opening, or a degraded heating wire producing an incomplete seal. Work through these four causes systematically before contacting a technician. Q5: How often does the heating wire need to be replaced? Heating wire has no fixed replacement interval — it depends on usage frequency and bag material. Machines used for high-volume daily production or sealing thicker materials such as aluminum foil bags will wear through heating wire more quickly. When seal lines become uneven, develop gaps, or the wire shows visible discoloration or brittleness, replace it promptly. Q6: Can poor seal quality damage product shelf life? Yes. A weak or incomplete seal allows moisture, oxygen, and environmental contamination to enter the package — directly reducing product shelf life and increasing the risk of spoilage, flavor degradation, or contamination. For food products, even a small gap in the seal line can significantly shorten the period during which the product remains safe and market-ready. Maintaining consistent seal quality is a direct food safety and product quality issue, not only a packaging efficiency concern. 📖 Further Reading Related articles on sealing machine selection, specifications, and performance: → How to Choose the Right Sealing Machine Based on Product Type → How to Choose the Right Sealing Length and Sealing Width → Vacuum Sealer vs. Continuous Band Sealer: Which Should You Choose? → What Industries Use Vacuum Sealers? Applications and Buying Guide → When Should You Use a Continuous Band Sealer? About This Article This article was prepared by the Daily Sealing System technical team. It is intended as a practical troubleshooting guide for packaging engineers, purchasing teams, food manufacturers, and industrial packaging users. Daily Sealing System Co., Ltd. is a Taiwan-based sealing machine manufacturer with an in-house production facility. Our product range includes vacuum sealers, external vacuum sealers, chamber vacuum sealers, continuous band sealers, foot sealers, impulse sealers, medical pouch sealers, and customized sealing equipment. The company holds ISO 9001:2015 certification. Certain products and related materials carry CE, FDA, EU No.10/2011, and BPA Free certifications. Patents are registered in Taiwan, the United States, Europe, Germany, Japan, and China. Content in this article is based on Daily Sealing System's practical manufacturing experience and after-sales technical service since 2010, and is intended to support equipment troubleshooting and purchasing decisions by B2B buyers and packaging operations teams. Need Help Identifying the Cause? Our technical team can help you determine whether your seal quality issue is related to: ✓ Machine settings and temperature calibration ✓ Bag material compatibility ✓ Consumable parts condition ✓ Equipment selection for your application View All Sealing Machine Series Contact Our Technical Team // //MORE