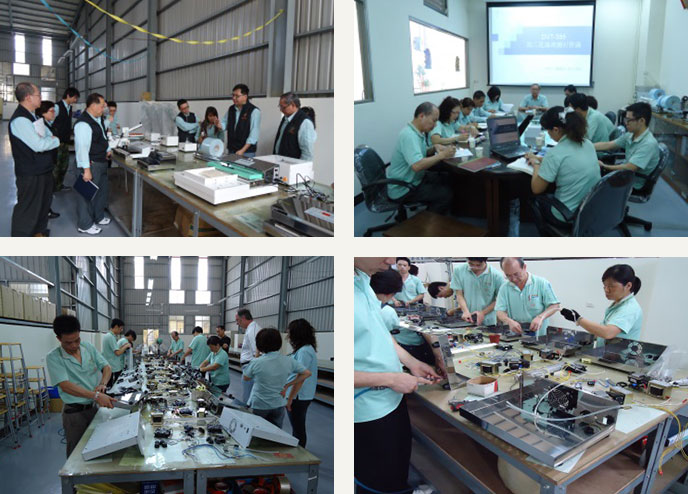
Motor, Transformers, PCB and vacuum bags are made in Taiwan.
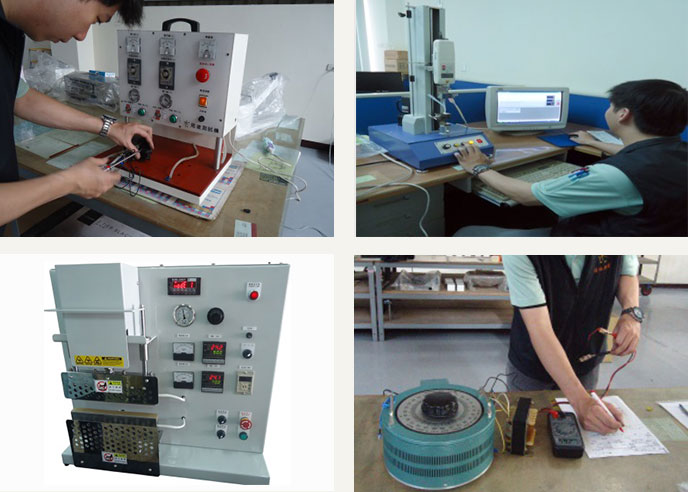
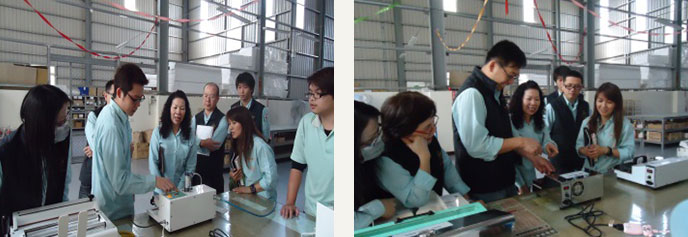
Strict quality control
100% product inspection: The inspection is included functions and
appearance of sealing machines.
Tensile strength test to ensure the sealing line tensile strength
value reaches the customer standard.
Electric leakage test: Puncture and insulation test.
Our production and inspection are all based on ISO 9001.
Professional packaging and sealing machine factory
Produce many kinds sealing machines and ODM/OEM products and provide
custom-made services.
More than 30 year experiences in packaging machines industry.
Sell sealing machines to America, Europe, Latin America and Asia.
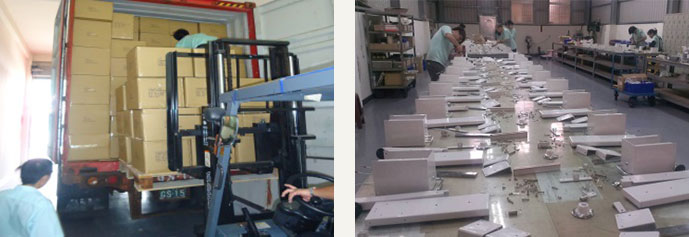
85% products in stocks, so we can deliver the products quickly.
The production process is based on SOP to ensure the quality of
sealing machines consistently.
Complete range of specifications of sealing machines
Complete range of specifications of sealing machines.
Many kinds of sealing machines and consumptive materials in stocks,
so customers can do one-stop shopping here.
The customers include Biotechnology companies, Medical equipment
companies, Food industry, Electronics industry, Handmade soap
industry and other industry..
Custom-made sealing machine service
Custom-made sealing machine service
Designs of the special sealing machine for irregular shape sealing
line, such as U-shape sealing line and L-shape sealing line.
Different width of sealing line could be custom-made to meet
customer requirements.
After-sales service of professional sealing machine
Provide the professional service for repair the broken sealing
machine immediately.
The sufficient supply of parts stock, so don’t worry about the parts
replace.
Some parts of sealing machine are used in common specifications, so
it is easy to get the parts for replace.
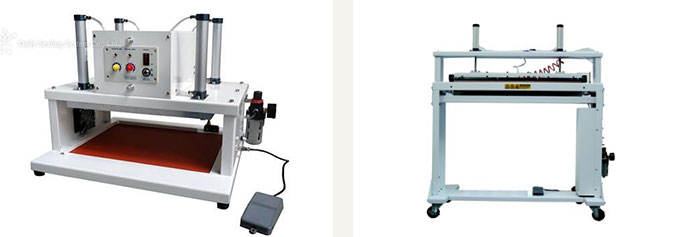
Hand type sealer is the easiest sealer for users. Hand type sealer is small size that can save space. Portable sealer is suitable for large and heavy package. ※ Hand type sealer : ➤For different operating type : - Hand type sealer: table type. Save space.
Press the hand lever and hand type sealer start to seal. Easy operating. - Hand press sealer: table type. Pull the lever down to start sealing. It can save effort. 25cm sealing line is suitable for tea bags or coffee bag packing. - Portable sealer is suitable
for wide working space. Portable sealer is also suitable for large and heavy articles, such us pallet package. ➤For different material of package bags : - Impulse hand type sealer/ portable sealer: It is suitable for PE, PP, PET material, and aluminum bags
and medical bags. - Constant heat hand type sealer / portable sealer: It is suitable for aluminum bags, vacuum bags and medical bags. More details: Click here
How to Set Sealing Time for Impulse, Constant Heat and Continuous Band Sealers How long should a sealing machine seal a bag? There is no single sealing time that works for every packaging material or sealing machine. The correct heat-sealing process depends
on several variables, including the sealing method, pouch structure, material thickness, seal width, pressure, temperature and production speed. This is especially important for B2B packaging operations because impulse sealers, constant heat sealers, continuous
band sealers and vacuum sealers do not control heat in the same way. For production teams, the goal should not be to find a universal number of seconds — the better approach is to establish a tested and documented sealing condition for the specific machine,
packaging material and production requirement. Quick Answer: How Long Should Sealing Time Be? There is no universal sealing time. Impulse sealers: commonly control heating time or output rather than actual sealing temperature Constant heat sealers: require
the correct combination of temperature, contact time and pressure Continuous band sealers: temperature and conveyor speed must be evaluated together, since line speed changes heat exposure Vacuum sealers: sealing time or temperature depends on machine design,
pouch structure and sealing requirements When material changes: re-test the sealing conditions whenever pouch structure, thickness, supplier or machine configuration changes For industrial production, sealing time should always be treated as one process parameter
rather than a standalone setting. 1. Why Is There No Universal Sealing Time? Heat sealing works by applying sufficient thermal energy to the pouch sealant layer while maintaining the required contact pressure for an appropriate period. This means that two
machines sealing what appears to be the same pouch may still require different settings. Sealing Method Impulse, constant heat and continuous sealing systems transfer heat differently. An impulse sealer heats only during the sealing cycle, while a constant
heat sealer maintains a heated sealing surface. A continuous band sealer moves the pouch through heating and cooling sections. Packaging Material Structure PE, PA/PE, PET/PE and other laminated films use different sealant layers and material structures. The
outer material name alone does not determine the correct sealing time. Material Thickness Thickness affects heat transfer, but a thicker pouch does not automatically mean operators should simply increase temperature or extend heating time. Material structure,
sealant layer and machine capability must also be considered. Seal Width and Pressure Seal width, contact area and pressure can affect how thermal energy is transferred across the sealing zone. A change in sealing width or pressure may therefore require process
settings to be re-tested. Related guide: How to Choose the Right Sealing Length and Sealing Width 2. Impulse Sealers: Start with Heating Time or Output Hand impulse sealers, many foot impulse sealers and other impulse-type machines heat the sealing element
only during the sealing cycle. For this reason, many impulse sealers do not directly control the actual surface temperature. Instead, the operator commonly adjusts heating time, timer level or output. Recommended adjustment process: Confirm the pouch structure
and thickness Start from the machine manual or an existing tested setting Test the actual packaging material used in production Begin with a relatively low setting and increase gradually Change only one major parameter at a time Allow the seal area to cool
appropriately before evaluating the result Record the confirmed machine and material settings Some impulse sealing systems also require a short pressure or cooling period after heating stops. Moving the pouch too early can affect a newly formed seal. Avoid
this common mistake: if a pouch does not seal properly, do not immediately turn the timer to the maximum setting. Excessive heat input may cause pouch shrinkage, melting or burn-through, excessive seal distortion, material sticking, or unnecessary wear on
heating elements or PTFE covers. The objective is not to apply maximum heat — it is to apply enough controlled heat to create a reliable seal without damaging the packaging material. 3. Constant Heat Sealers: Sealing Time Is Only One Part of the Process Constant
heat sealers maintain the sealing jaws or heating surface at a controlled temperature. For these machines, sealing performance depends on the combined effect of sealing temperature, contact or dwell time, sealing pressure, pouch structure and material thickness.
If the temperature is too low, simply holding the pouch longer may not produce a reliable seal. If temperature and dwell time are both excessive, the pouch may distort, thin out or melt through. For constant heat sealing, a better process is: pouch structure
→ suitable temperature range → dwell time → pressure → seal-quality verification — rather than asking only "how many seconds should I seal this bag?" For material-specific temperature guidance, see: Heat Sealing Temperature Guide for Different Packaging Materials.
4. Continuous Band Sealers: Conveyor Speed Changes Heat Exposure A continuous band sealer moves the pouch continuously through a heating section. For this reason, conveyor speed affects how long the packaging material remains exposed to heat. Production ChangePossible
Effect Higher conveyor speed Shorter exposure time in the heating zone; existing temperature settings may provide insufficient heat Lower conveyor speed Longer heat exposure; excessive temperature may distort or overheat the pouch Different pouch thickness
or laminate Temperature and conveyor speed should be re-tested together Temperature and conveyor speed should therefore be treated as linked process variables. A production team that increases line speed without rechecking the sealing condition may see previously
stable seals become weak or inconsistent. Similarly, slowing the line while maintaining an unnecessarily high temperature may create excessive heat exposure. For higher-volume packaging operations, both seal consistency and production throughput should be
considered when validating the settings. Related guide: When Should You Use a Continuous Band Sealer? 5. How Should Sealing Time Be Set on a Vacuum Sealer? A vacuum sealer normally performs at least two different process stages: air evacuation and heat sealing.
The vacuum cycle and the sealing cycle should therefore be evaluated separately. Depending on machine design, the operator may adjust sealing time, temperature or another heat-control setting. Whenever the vacuum pouch supplier, material structure or thickness
changes, the sealing condition should be re-tested — even if the vacuum extraction performance remains unchanged. If Sealing Heat Is Insufficient Incomplete seal formation Weak seal strength Gradual loss of vacuum Leakage after handling or storage If Heat
Input Is Excessive Seal-area distortion Pouch shrinkage Melt-through Weakening of the seal area Always confirm the specific vacuum sealer design and pouch structure before establishing production settings. 6. How Can You Tell If Sealing Time Is Too Short or
Too Long? The seal result provides useful clues, but one symptom does not always point to only one cause. Seal ConditionPossible Direction to Check Seal opens easily or contains unfused areas Heat input may be insufficient; also check material compatibility,
pressure and contamination Seal line shrinks or wrinkles Possible excessive heat or unsuitable settings Pouch melts through or burns Heat input may be excessive The same section repeatedly fails to seal Check heating element, PTFE cover, pressure pad or sealing-area
alignment rather than only increasing time Seal quality changes after switching pouch supplier Re-test material structure, thickness and sealing parameters If increasing sealing time does not improve the result, do not continue increasing it indefinitely.
The problem may instead involve an incompatible packaging material, insufficient or excessive temperature, uneven pressure, contamination in the sealing area, a worn heating element, damaged PTFE material, or other machine-related issues. Related guide: Heat
Sealer Not Sealing Properly? 5 Common Causes and How to Fix Them 7. How to Validate Sealing Time After Changing Packaging Material For manufacturers, food processors, contract packers and other B2B users, a pouch change should be treated as a process change.
This includes changes in packaging supplier, resin or laminate structure, material thickness, bag dimensions, sealing machine, and production speed. 01 Confirm the Packaging Specification Record the material structure, total thickness and sealant layer when
available 02 Confirm the Sealing Machine Type Impulse, constant heat, continuous band or vacuum sealer 03 Establish a Starting Setting Use manufacturer instructions or a previously confirmed condition 04 Keep Other Variables Stable Change only one major parameter
at a time 05 Adjust Gradually Make small changes and compare seal results 06 Allow the Seal to Stabilize Allow sufficient cooling before judging the seal 07 Record the Confirmed Production Setting Document the machine, material and operating parameters 8.
For Production Lines, Do Not Record Only "2 Seconds" or "3 Seconds" For repeat B2B production, a single sealing-time number is usually not enough. If the packaging material or equipment changes later, a record such as "seal for 2 seconds" provides very little
information about why the process originally worked. A more useful production record should include: Sealing machine model Packaging material structure Pouch thickness Sealing time or output setting Sealing temperature, when applicable Conveyor speed for continuous
band sealers Seal width Product type Pouch opening condition Seal inspection result Packaging-material supplier or batch, when relevant This makes it easier to reproduce confirmed conditions and troubleshoot future process changes. 9. B2B Sealing-Process Checklist:
What Information Should Buyers Prepare? When contacting a sealing-machine manufacturer or packaging equipment supplier, providing complete process information can help identify the correct machine configuration and starting settings more efficiently. Prepare:
Current sealing machine model Pouch material structure Pouch thickness Bag opening width Required sealing length Required seal width Product being packaged Dry, oily, powder or liquid product condition Current sealing time or timer setting Current temperature,
when applicable Conveyor speed, when applicable Daily production volume Required production speed Current seal-quality problem Target market or special packaging requirement For OEM / ODM or new packaging projects, this information is also useful when determining
whether the existing sealing method is suitable for the required output and material. The following questions are compiled from Daily Sealing System's manufacturing, packaging-material testing and after-sales technical support experience since 2010. Frequently
Asked Questions Q1: How many seconds should a heat sealer be set for? There is no universal sealing time. The correct setting depends on machine type, pouch structure, thickness, seal width, pressure and other process conditions. Always validate the setting
using the actual production material. Q2: Does a thicker bag always require a longer sealing time? No. Thickness can affect heat transfer, but material structure, sealant layer, temperature, machine output and pressure also influence the result. Thickness
alone should not determine sealing time. Q3: Should I adjust temperature or time on an impulse sealer? Many impulse sealers primarily control heating time or output rather than actual sealing temperature. Machine designs vary, so always confirm the controls
specified for the model. Q4: Why does my continuous band sealer produce weak seals after increasing conveyor speed? Increasing conveyor speed reduces the time the pouch remains in the heating zone. If other parameters remain unchanged, the material may receive
insufficient heat. Re-test temperature and conveyor speed together. Q5: Why does the bag still not seal even after increasing sealing time? The problem may not be insufficient time. Check packaging-material compatibility, sealing temperature or output, pressure,
contamination, heating elements and PTFE components before continuing to increase the setting. Q6: Do sealing settings need to be re-tested when changing pouch suppliers? Yes. Even when the material name and nominal thickness appear similar, the sealant layer,
laminate structure and production specifications may differ. Re-test and document the sealing condition before full production. 📖 Further Reading For sealing-machine buyers, packaging engineers and production teams: → Heat Sealing Temperature Guide for PE,
OPP & Foil Bags → Heat Sealer Not Sealing Properly? Common Causes and How to Fix Them → How to Choose the Right Sealing Length and Sealing Width → When Should You Use a Continuous Band Sealer? → Sealing Machine Maintenance: 7 Ways to Extend Service Life About
This Article This article was prepared by the Daily Sealing System technical team for purchasing teams, packaging engineers, production managers, contract packers and industrial packaging users. Daily Sealing System Co., Ltd. is a Taiwan-based sealing machine
manufacturer with an in-house production facility. The company provides impulse sealers, foot sealers, constant heat sealers, continuous band sealers, vacuum sealers, medical pouch sealers and customized sealing equipment, together with OEM / ODM support and
after-sales technical service. This guide is based on Daily Sealing System's manufacturing, packaging-material testing and after-sales technical support experience since 2010. Actual sealing time, temperature, pressure and conveyor-speed settings vary by machine
model, packaging material and production conditions. Production parameters should always be tested and confirmed using the actual machine and pouch specification. Need Help Determining the Right Sealing Settings for Your Packaging Material? Send us your machine
model, pouch structure, pouch thickness, bag dimensions, product type, current sealing settings, daily production requirement and current seal result. Our technical team can help you evaluate the appropriate sealing-machine configuration and starting process
settings for your packaging application. View Sealing Machines Contact Our Technical Team // //
Do Different Packaging Materials Require Different Sealing Temperatures? Heat Sealing Temperature Guide When switching from one packaging material to another, many production teams continue using the same heat sealer settings. This often results in weak
seals, burnt seal lines, pouch deformation, leakage, or inconsistent seal quality. Based on Daily Sealing System's practical experience in sealing machine manufacturing and after-sales technical support since 2010, different packaging materials, sealant layers
and material thicknesses require different heat sealing conditions. Selecting the correct sealing temperature is therefore one of the first steps toward achieving reliable and repeatable seal quality in a B2B packaging operation. A setting that is too low
may result in insufficient bonding, while excessive heat can distort the pouch and accelerate wear on sealing-machine consumables. Quick Answer: Key Principles for Heat Sealing Temperature Settings Different packaging materials require different heat sealing
conditions. Material structure and sealant-layer composition are as important as total pouch thickness. Always re-test sealing settings when changing pouch material, supplier, structure or thickness. A temperature that is too low may cause weak or incomplete
seals. Excessive temperature may burn, distort or melt the packaging material and accelerate consumable wear. For production validation, start from the machine or material supplier's recommended range and adjust incrementally using sample pouches. Temperature
is only one variable — dwell time, pressure, sealing width and conveyor speed can also affect final seal quality. 1. Why Do Different Packaging Materials Require Different Sealing Temperatures? A heat sealer applies thermal energy to the sealant layer of a
pouch or bag. The two inner surfaces soften and bond under controlled heat and pressure, then form a seal as the material cools. Different pouch structures use different sealant materials, thicknesses and laminated layers. This means that the same machine
setting may produce a strong seal on one material but an incomplete or burnt seal on another. When Sealing Temperature Is Too Low Sealant layers do not fully bond Seal line appears closed but opens under light pressure Vacuum bags may lose vacuum after sealing
Thicker laminated pouches may seal inconsistently Parts of the seal line may remain unfused When Sealing Temperature Is Too High Seal line becomes burnt or discolored Pouch material melts through at the sealing area Seal edges become wrinkled or distorted
Thin PE or heat-sealable OPP structures are particularly sensitive Heating elements and PTFE tape may wear faster 2. Reference Heat Sealing Temperature Ranges by Packaging Material The following ranges are intended as starting references for process testing,
not universal production specifications. Actual settings can vary depending on pouch supplier, sealant-layer composition, total material thickness, machine design, sealing pressure, dwell time and production speed. For procurement and production teams, the
safest approach is to confirm the material specification with the pouch supplier and then perform a sample sealing test on the actual machine before mass production. Packaging MaterialStarting Temperature Reference*Typical ApplicationsPurchasing / Production
Notes Thin PE Bags Approx. 120–160°C Snacks, dry products, general lightweight packaging Relatively heat-sensitive. Start conservatively and verify actual material specifications before production. Heat-Sealable OPP / OPP Laminates Approx. 120–160°C Stationery,
lightweight goods, food and retail packaging Confirm that the structure includes a heat-sealable layer. Pure OPP film structures may require different converting or sealing conditions. NY/PE Laminated Vacuum Bags Approx. 170–200°C Meat, seafood, agricultural
products, vacuum packaging Settings depend strongly on laminate thickness, sealant layer and vacuum-sealer design. Confirm seal width and machine compatibility. PET/PE Laminated Pouches Approx. 170–200°C Food packaging, industrial components, general laminated
packaging The PET outer layer provides heat resistance while the inner PE-based sealant layer forms the bond. Process settings must deliver sufficient heat to the sealant layer without damaging the laminate. Aluminum Foil / Foil-Laminated Pouches Approx. 180–220°C
Coffee, tea, pharmaceutical packaging, moisture-sensitive industrial products Thicker foil laminates commonly require an adjustable-temperature constant heat sealer. Confirm pouch structure, sealant layer and equipment compatibility before purchase. Thick
Multi-Layer Laminated Pouches May require 200°C or above depending on structure Heavy industrial products, agricultural bulk packaging, specialty packaging Do not increase temperature alone. Dwell time, sealing pressure, sealing width and heating method should
be evaluated together. Important: The temperature ranges above are starting references only. Packaging films with the same generic material name can use different resin grades, sealant layers and laminate structures. Whenever the pouch material, supplier,
thickness or structure changes, run a new sealing test before starting production. 3. How to Determine the Correct Heat Sealing Temperature There is no single sealing temperature that works for every material and every heat sealer. For B2B production, the
correct approach is to establish a controlled test procedure and document the validated setting for each packaging material. 01 Identify the Material Confirm pouch structure, sealant layer and thickness — for example PE, NY/PE, PET/PE or foil laminate. 02
Set a Starting Point Use the machine manufacturer's or packaging-material supplier's recommended range as the starting point. 03 Run Sample Seals Use production-equivalent sample pouches and inspect seal appearance, continuity and initial seal strength. 04
Adjust Incrementally Increase heat gradually if the seal is weak. Reduce the setting if the pouch burns, distorts or melts. 05 Document the Setting Record pouch supplier, material structure, thickness, machine model, temperature and other relevant process
settings. 4. How Can You Verify Whether the Seal Is Strong Enough? Temperature setting alone does not confirm seal quality. After establishing an initial setting, the production team should verify the actual seal according to the packaging requirements and
internal quality-control criteria. Practical Seal Quality Checks: Visual Inspection: The seal line should be continuous and even, without burn marks, excessive wrinkles, holes or obvious unfused sections. Manual Pull Check: Apply even force to both sides of
the sealed area. A properly bonded seal should not peel open easily under normal handling conditions. Vacuum Hold Observation: For vacuum packaging, monitor the package over a defined internal QC period to check for loss of vacuum, leakage or package rebound.
A 24-hour observation may be used as an internal screening step, but it is not a universal industry standard. Production QC Testing: For applications with defined seal-integrity requirements, consider peel-strength, leak, burst or vacuum-decay testing according
to your internal quality specification. Cross-Section Review: For troubleshooting, inspect the seal area for uniform fusion and signs of delamination. 5. Six Common Heat Sealing Temperature Mistakes 1. Changing Pouch Material Without Re-Testing Even materials
with the same generic name can use different resin grades, thicknesses and sealant layers. Re-test whenever the pouch supplier or specification changes. 2. Assuming Higher Temperature Means a Stronger Seal Excessive heat can damage the pouch, distort the seal
area and accelerate wear on heating elements and PTFE tape. 3. Ignoring Heat Build-Up During High-Volume Production During extended production runs, equipment temperature and process conditions may change. Periodically inspect seal quality instead of assuming
the first validated setting remains optimal throughout the shift. 4. Looking Only at Material Thickness Thickness matters, but laminate structure, sealant layer, dwell time, sealing pressure and heating method can be equally important. 5. Sealing Through Oil,
Moisture or Powder Contamination at the bag opening can prevent proper bonding even when the temperature setting is correct. Keep the sealing area clean and dry before sealing. 6. Using the Wrong Heating Method for Thick Foil Laminates Some thick multi-layer
foil pouches require stable, adjustable heat that a standard impulse sealer may not provide. Confirm the pouch sealant structure and machine capability, and evaluate an adjustable-temperature constant heat sealer when required. 6. How Sealing Settings Differ
by Machine Type Not every sealing machine controls heat in the same way. For purchasing teams, understanding the difference between time-controlled impulse sealing and temperature-controlled constant heat sealing is especially important. Sealing Machine TypePrimary
Setting MethodB2B Purchasing / Production Notes Hand Impulse Sealer Sealing time / heating-time control rather than direct temperature setting Commonly used for PE and other compatible plastic bags. Material compatibility should be confirmed before purchasing.
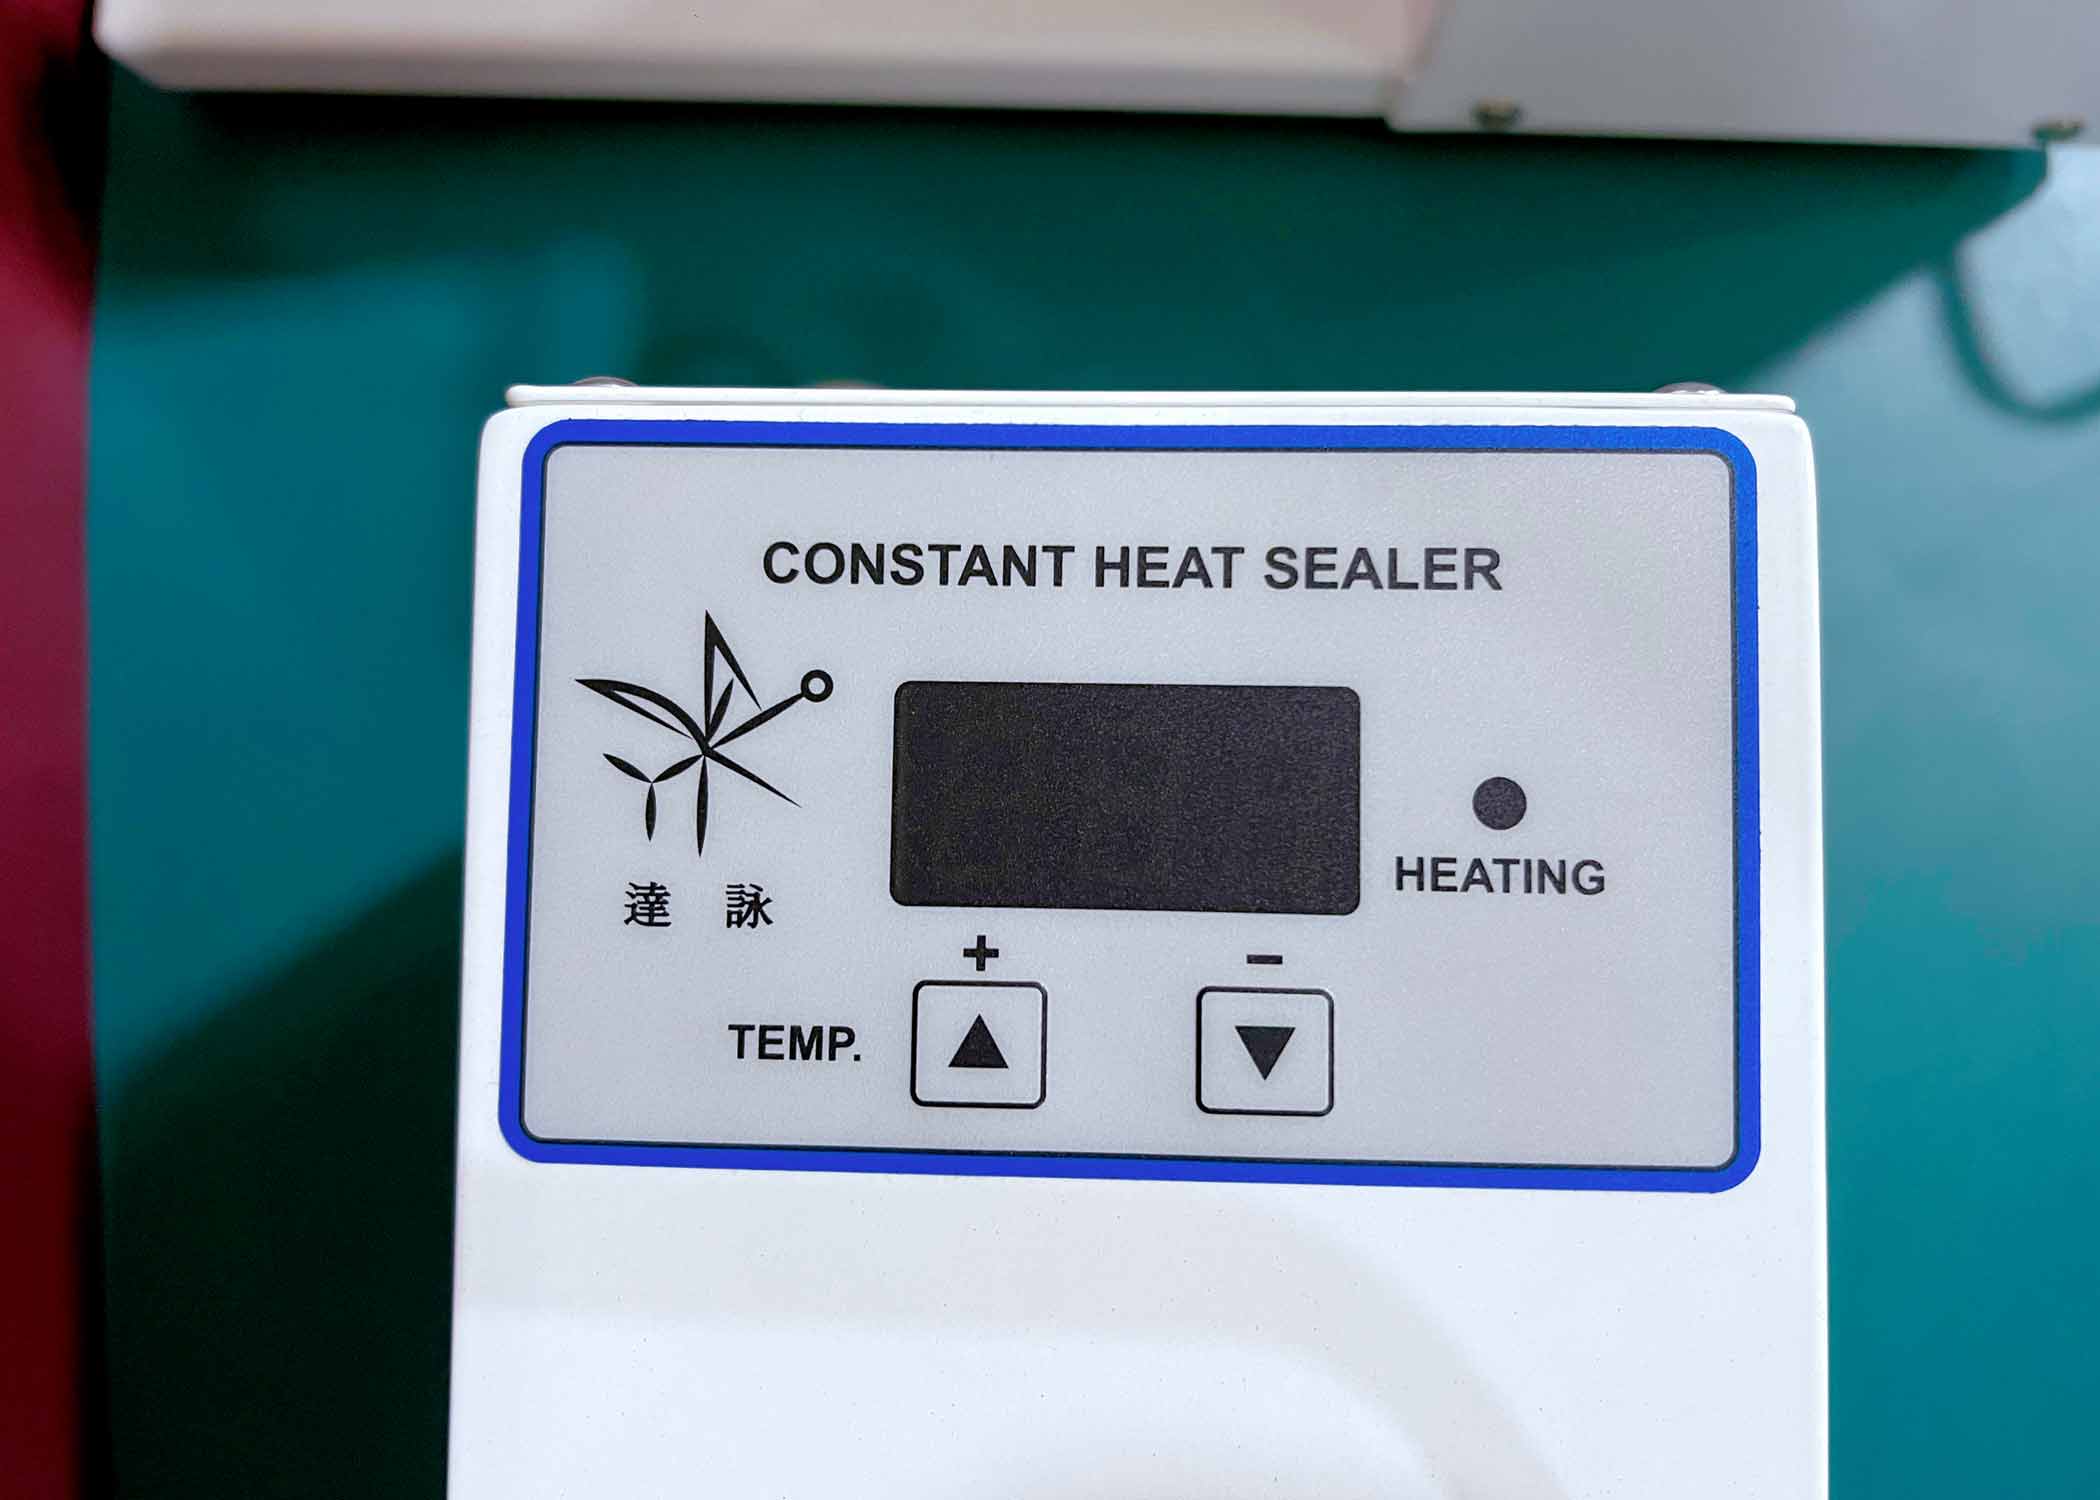
Foot Impulse Sealer Heating-time control Suitable for repetitive manual packaging where hands-free operation improves workflow. High-frequency use requires monitoring of seal consistency. Constant Heat Sealer Direct adjustable temperature control Often preferred
for foil laminates, vacuum nylon bags and other thicker or multi-layer packaging materials requiring stable continuous heat. Continuous Band Sealer Temperature setting + conveyor speed Designed for higher-volume production. Temperature and line speed must
be optimized together to maintain consistent heat input. Vacuum Sealer Sealing time or temperature depending on machine design Vacuum extraction and sealing are separate process stages. Confirm bag type, sealing method, seal width and production requirements
before equipment selection. 7. Continuous Band Sealer: Why Temperature and Conveyor Speed Must Be Adjusted Together For a continuous band sealer, seal quality is determined by the combined effect of temperature, conveyor speed and material characteristics.
Higher conveyor speed → shorter exposure time in the heating zone → process settings may need adjustment to maintain sufficient heat input. Lower conveyor speed → longer heat exposure → excessive temperature may distort or burn the pouch. Whenever pouch structure,
thickness or conveyor speed changes, re-test the sealing conditions. Use sample material before a full production run and confirm that the seal line is continuous, undamaged and sufficiently strong for the intended application. B2B Buyer Checklist: Information
to Prepare Before Selecting a Heat Sealer Packaging material structure: PE, OPP laminate, NY/PE, PET/PE, foil laminate, etc. Total pouch thickness and sealant-layer specification Bag opening width and required sealing length Required sealing width or number
of seal lines Product type: dry, oily, powder, liquid, food, industrial component or medical product Daily production volume and required cycle speed Current sealing temperature, time or conveyor-speed settings Required seal-integrity or internal QC criteria
Available power supply and production-line configuration Daily Sealing System Can Help Evaluate the Right Sealing Conditions for Your Packaging Material Daily Sealing System Co., Ltd. is a Taiwan-based sealing machine manufacturer with an in-house production
facility. Our product range includes impulse sealers, constant heat sealers, foot sealers, continuous band sealers, vacuum sealers, medical pouch sealers and customized sealing equipment. For a new packaging project, buyers can provide the machine model, pouch
structure, material thickness, bag dimensions, product type and daily output requirement so our technical team can help evaluate the appropriate sealing-machine configuration and starting process settings. The following questions are based on common sealing-temperature
and packaging-material inquiries handled by Daily Sealing System's technical and after-sales service team across food processing, agricultural packaging, electronics manufacturing and industrial packaging applications. Frequently Asked Questions Q1: Do different
packaging materials require different sealing temperatures? Yes. Different packaging films use different sealant layers, resin structures and thicknesses, so the same temperature setting may produce a weak seal on one material and burn another. Whenever the
material, supplier, laminate structure or thickness changes, the sealing conditions should be re-tested before production. Q2: Does a higher sealing temperature always produce a stronger seal? No. The goal is to apply enough thermal energy to create a reliable
bond without damaging the pouch. Excessive heat can distort the seal area, melt through the bag, weaken the laminate structure and accelerate wear on sealing-machine consumables. Q3: What type of sealer is recommended for aluminum foil or laminated foil pouches?
Thick multi-layer foil laminates often require stable, adjustable heat so that sufficient thermal energy reaches the inner sealant layer. An adjustable-temperature constant heat sealer is commonly evaluated for these applications. However, machine selection
should be based on the actual pouch structure, thickness, sealing width and production requirements rather than material name alone. Q4: How should I adjust the temperature of a continuous band sealer? Continuous band sealing depends on both temperature and
conveyor speed. Increasing line speed reduces the time the pouch remains in the heating zone, while slower speed increases heat exposure. Whenever the material or production speed changes, test both parameters together and confirm seal quality before full
production. Q5: How do I know whether my heat sealing temperature is correct? Start with a visual inspection: the seal line should be continuous and free from burns, holes and obvious unfused sections. Then perform an appropriate strength or leak check for
the packaging application. For vacuum packaging, monitor whether the package maintains vacuum over your defined QC observation period. Once the process is validated, record the material specification, machine model and sealing settings for repeat production.
Further Reading Related technical guides for sealing-machine buyers, production managers and packaging engineers: → Heat Sealer Not Sealing Properly? 5 Common Causes & Fixes → Sealing Machine Maintenance Guide: How Often Should You Service Your Equipment?
→ How to Choose the Right Sealing Length and Sealing Width → Sealing Machine Buying Guide: How to Choose the Right Sealer → When Should You Use a Continuous Band Sealer? About This Article This article was prepared by the Daily Sealing System technical team
for purchasing teams, packaging engineers, production managers and industrial packaging users. Daily Sealing System Co., Ltd. is a Taiwan-based sealing machine manufacturer with an in-house production facility. Our product portfolio includes vacuum sealers,
external vacuum sealers, chamber vacuum sealers, impulse sealers, constant heat sealers, foot sealers, continuous band sealers, medical pouch sealers and customized sealing equipment. The company holds ISO 9001:2015 certification. Certain products and related
packaging materials carry CE, FDA, EU No.10/2011 and BPA Free certifications. Patents are registered in Taiwan, the United States, Europe, Germany, Japan and China. The content in this guide is based on Daily Sealing System's practical manufacturing experience,
packaging-material testing and after-sales technical support since 2010. The temperature ranges provided are starting references only; actual production settings should always be validated using the specific pouch material and machine configuration. Need Help
Matching Your Packaging Material to the Right Heat Sealer? Send us your pouch material, thickness, bag size, product type, required daily output and current sealing-machine model. Our technical team can help you evaluate the appropriate sealing-machine configuration
and starting process settings for your packaging application. View All Sealing Machines Contact Our Technical Team // //
We use cookies to provide a better experience. By proceeding, you agree to our PRIVACY POLICY, including the use of cookies and other tracking technologies.ACCEPT


(16).jpg)
(17).jpg)

.jpg)